

What is a Bentonite Powder Conveyor? Understanding Its Design Principles
For industries dealing with bentonite powder, the efficient and reliable transport of this fine material is crucial. A bentonite powder conveyor, also known as a bentonite powder handling system, is a specialized piece of equipment designed to move bentonite powder from one location to another with precision and minimal loss. This article explores the fundamental aspects of bentonite powder conveyors, focusing on their design principles and the key factors that contribute to their effectiveness in industrial applications.
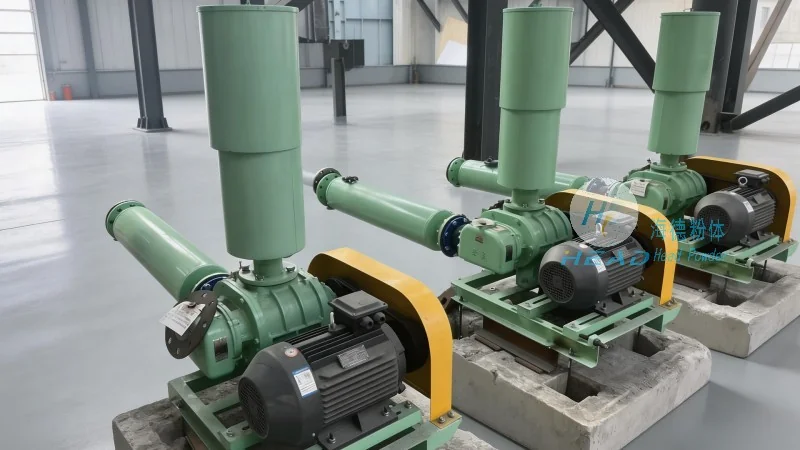
Understanding the Basics of Bentonite Powder Conveyors
Bentonite powder, a type of clay mineral, is widely used in various industries including oil drilling, paper manufacturing, and foundry casting due to its unique properties such as high swelling capacity and excellent thixotropy. The transportation of bentonite powder requires equipment that can handle its fine particle size and prevent caking or segregation. Bentonite powder conveyors are engineered to address these challenges by providing a controlled environment for material movement.
The Core Design Principles of Bentonite Powder Conveyors
The design of a bentonite powder conveyor is centered around several critical principles to ensure optimal performance. First, the equipment must be capable of handling the fine, cohesive nature of bentonite powder without causing blockages or material degradation. This is achieved through the use of specialized components such as flexible hoses, rotary valves, and low-friction conveying tubes. Second, the system is designed to maintain a consistent flow rate, which is essential for maintaining the uniformity of the bentonite powder. This is typically achieved through the integration of variable speed drives and pressure sensors that regulate the conveying process.
Third, the design incorporates features to prevent dust generation and ensure environmental compliance. Bentonite powder is a fine particulate that can easily become airborne, posing health and safety risks. Therefore, most bentonite powder conveyors are equipped with dust collection systems and sealed housing to contain the material and minimize exposure. Fourth, the system is built for durability and low maintenance, as bentonite powder can be abrasive and corrosive to certain materials. High-quality materials like stainless steel and wear-resistant coatings are used in the construction of the conveyor components to extend the equipment's lifespan.
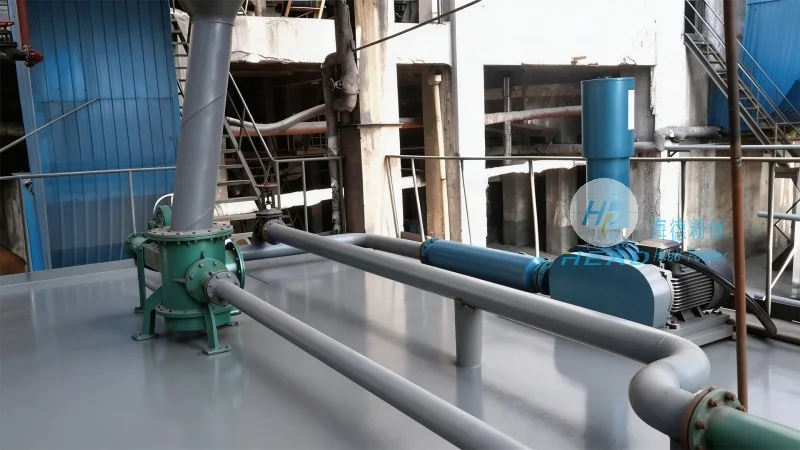
Key Components and Their Functions in Bentonite Powder Conveyors
Several key components work together to ensure the smooth operation of a bentonite powder conveyor. The feeding mechanism, often a hopper or a rotary feeder, is responsible for introducing the bentonite powder into the system at a controlled rate. This component prevents overloading and ensures a steady flow into the conveying line. The conveying line itself, which can be a flexible hose or a rigid tube, transports the powder from the feeding point to the discharge point. The choice between a flexible and rigid line depends on the application, with flexible hoses offering more flexibility for complex layouts and rigid tubes providing higher pressure resistance.
The discharge mechanism, typically a rotary valve or a slide gate, controls the release of the bentonite powder from the conveyor. This component is crucial for controlling the flow rate and preventing backflow or material spillage. The control system, which includes sensors and a control panel, monitors the conveyor's operation and adjusts parameters as needed. For example, pressure sensors can detect blockages and trigger alarms or automatic shutdowns to prevent equipment damage. The dust collection system, which may include filters and a vacuum pump, captures any airborne particles and returns them to the conveyor line, ensuring minimal material loss and compliance with environmental regulations.
Applications and Benefits of Bentonite Powder Conveyors
Bentonite powder conveyors are widely used in industries where the consistent and efficient transport of bentonite powder is essential. In the oil and gas industry, bentonite is used as a drilling fluid additive to improve the fluid's properties. The conveyor system ensures that the bentonite powder is delivered to the drilling site in a controlled manner, maintaining the quality of the drilling fluid. In the paper industry, bentonite is used as a filler and a coating agent. The conveyor system allows for the precise addition of bentonite to the paper manufacturing process, improving the paper's strength and quality. In the foundry industry, bentonite is used as a mold and core material. The conveyor system ensures that the bentonite powder is delivered to the casting site in a uniform manner, reducing defects in the final products.
The benefits of using a bentonite powder conveyor extend beyond just efficient material transport. By maintaining the purity and consistency of the bentonite powder, the conveyor system helps to improve the quality of the end products. It also reduces labor costs by automating the material handling process, allowing workers to focus on other tasks. Additionally, the conveyor system improves safety by containing the material and reducing dust exposure, which is particularly important in industries where bentonite powder can be hazardous to human health.
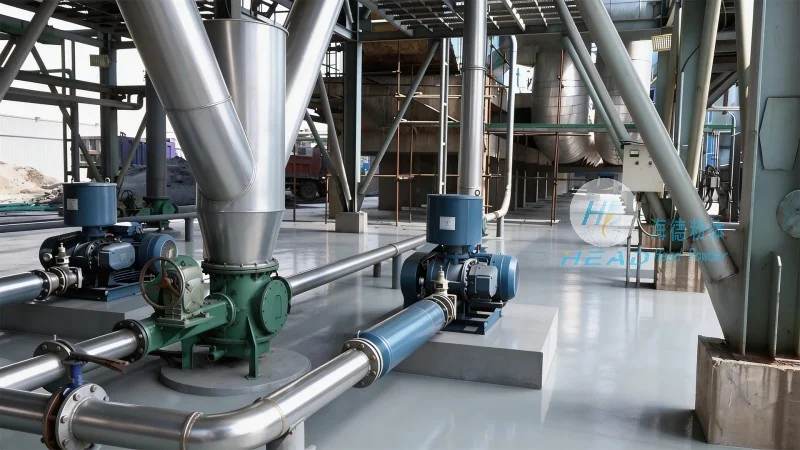
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of bentonite powder handling equipment. With its headquarters located in Shandong, China, the company specializes in designing and manufacturing high-quality bentonite powder conveyors and related systems. HeadPowder's team of engineers and technicians has extensive experience in the field of powder handling, ensuring that their products meet the highest standards of performance and reliability. The company's commitment to innovation and customer satisfaction has made it a trusted partner for industries worldwide.
HeadPowder's bentonite powder conveyors are designed to meet the specific needs of each customer. The company offers a range of models with different capacities, materials, and features to suit various applications. Whether it's a small-scale operation or a large industrial plant, HeadPowder can provide a customized solution that ensures efficient and safe transport of bentonite powder. The company's products are backed by a comprehensive warranty and technical support, giving customers peace of mind knowing that their equipment will perform reliably for years to come.
Conclusion
In conclusion, a bentonite powder conveyor is a critical piece of equipment for industries that rely on bentonite powder. Its design principles, which focus on handling the fine and cohesive nature of the material, ensure that the conveyor system operates efficiently and safely. The key components and features of the conveyor, such as the feeding mechanism, conveying line, and discharge mechanism, work together to maintain the quality and consistency of the bentonite powder. The use of a bentonite powder conveyor not only improves the efficiency of the material handling process but also enhances the quality of the end products and ensures workplace safety.