

What is a Vacuum-Pressure Mixed Powder Conveying System Equipment? What is its Design Principle?
A vacuum-pressure mixed powder conveying system is a specialized industrial equipment designed to transport bulk powders and granular materials over long distances with high efficiency and minimal product degradation. This system integrates both vacuum and pressure modes of operation, offering a versatile solution for various material handling challenges in industries such as pharmaceuticals, food processing, chemical manufacturing, and more. The equipment is engineered to handle a wide range of materials, from fine powders to coarse granules, while maintaining product integrity and ensuring consistent flow rates.
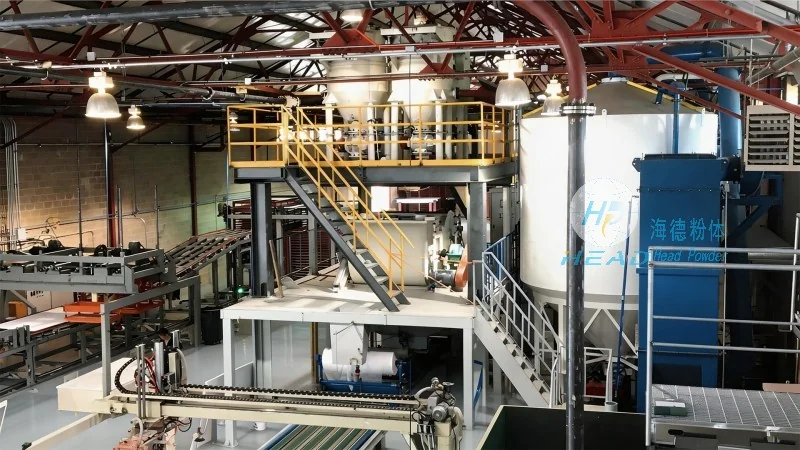
Understanding the Core Components and Functionality
The vacuum-pressure mixed powder conveying system consists of several key components that work in tandem to achieve effective material transport. These components typically include a vacuum pump, a pressure blower, a hopper or feed hopper for material storage, a conveying line (often equipped with flexible hoses or rigid pipes), and a control system for regulating the flow. The vacuum mode is used to draw material from the source, while the pressure mode is employed to push the material through the conveying line to the destination. This mixed operation allows for precise control over the material flow, enabling the system to handle both low and high material loads with ease.
The Design Principle Behind the System
The design principle of the vacuum-pressure mixed powder conveying system is centered on the balance between vacuum and pressure forces to create a stable and continuous material flow. The system operates by creating a negative pressure (vacuum) at the intake end to attract the material from the source, and then applying positive pressure (from the blower) at the discharge end to propel the material forward. The mixing of these two forces ensures that the material is conveyed smoothly without clogging or segregation. The control system plays a crucial role in maintaining the optimal pressure differential, which is essential for preventing material buildup and ensuring consistent performance. The design also incorporates features such as air filtration and separation to prevent dust contamination and maintain product purity.
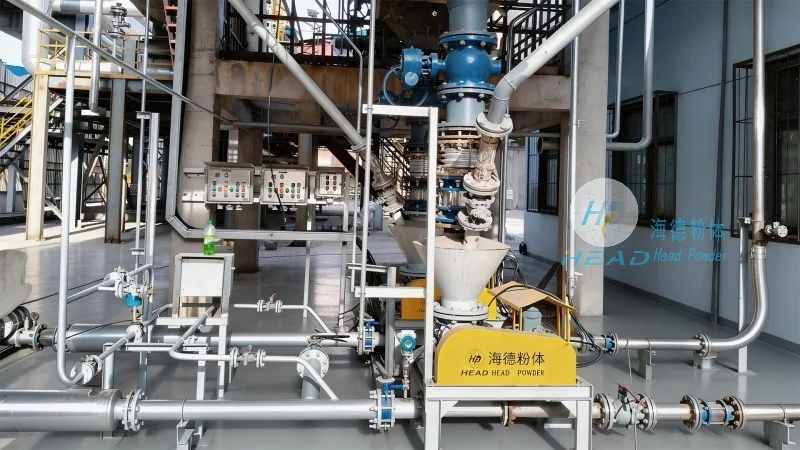
Key Features and Advantages of the Equipment
One of the primary advantages of the vacuum-pressure mixed powder conveying system is its ability to handle a wide variety of materials, including those that are sensitive to moisture or air exposure. The system's flexible design allows for easy integration into existing production lines, and it can be customized to meet specific operational requirements. Another key feature is the system's energy efficiency, as it uses both vacuum and pressure modes in a coordinated manner to minimize energy consumption. The equipment also offers high reliability and low maintenance requirements, making it a cost-effective solution for long-term material handling needs. Additionally, the system provides precise control over material flow rates, which is critical for maintaining product quality and meeting production targets.
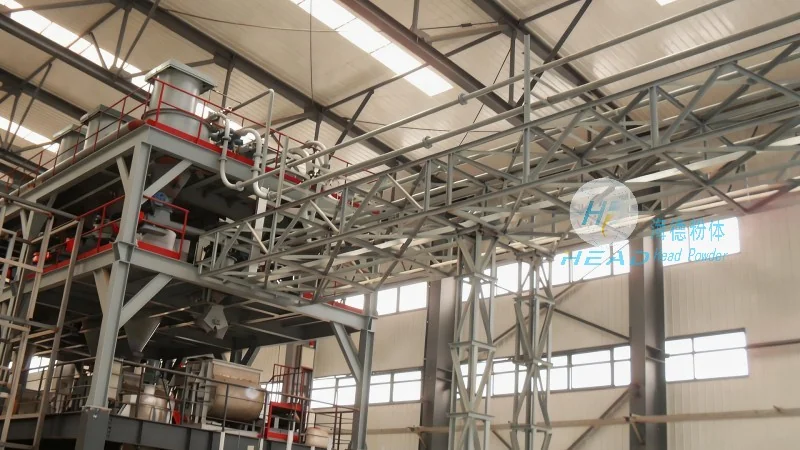
Application Scenarios and Industry Use Cases
The vacuum-pressure mixed powder conveying system is widely used in various industries due to its versatility and efficiency. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the materials are handled under sterile conditions. In the food processing industry, the system is employed to convey ingredients such as flour, sugar, and spices, maintaining product freshness and preventing contamination. In chemical manufacturing, the system is used to transport raw materials and intermediates, ensuring that the materials are conveyed safely and without degradation. The equipment is also used in the agricultural sector to transport fertilizers and other bulk materials, improving the efficiency of material handling operations.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial powder handling equipment based in China. The company specializes in the design, development, and production of vacuum-pressure mixed powder conveying systems and other related equipment. With years of experience in the industry, HeadPowder has established itself as a trusted provider of high-quality, reliable equipment that meets the needs of various industries. The company's products are known for their durability, efficiency, and ease of maintenance, making them a preferred choice for many businesses. HeadPowder's commitment to quality and customer satisfaction has helped it build a strong reputation in the market, and it continues to innovate and improve its products to meet the evolving needs of its clients.