

What is an Automatic Quantitative Powder Conveyor? What are its Design Principles?
An automatic quantitative powder conveyor is a specialized industrial equipment designed to handle, transport, and dispense bulk powders with high precision and efficiency. This machinery is crucial in various industries, including pharmaceuticals, food processing, chemical manufacturing, and more, where accurate measurement and controlled delivery of powders are essential for product quality and process consistency. The primary function of such a conveyor is to ensure that the right amount of powder is delivered to the next stage of production, minimizing waste and optimizing operational performance.
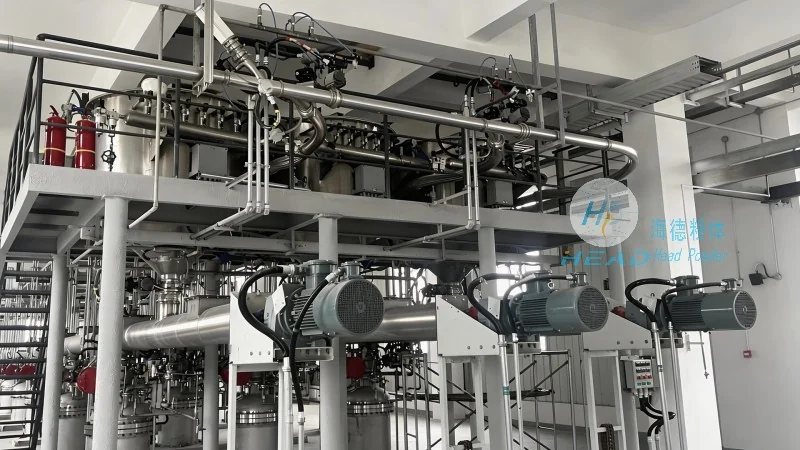
Key Design Principles Behind the Automatic Quantitative Powder Conveyor
The design of an automatic quantitative powder conveyor is built on several fundamental principles that ensure its reliability, accuracy, and adaptability to different powder types and applications. One of the core principles is the integration of precise measurement mechanisms, such as volumetric or gravimetric sensors, which allow for exact control over the quantity of powder being conveyed. These mechanisms are often calibrated to handle a wide range of powder densities and flow characteristics, ensuring consistent performance regardless of the material being processed.
Another critical design principle is the use of robust and durable construction materials. Since powder conveyors are exposed to abrasive and potentially corrosive environments, the equipment is typically made from high-quality stainless steel or other corrosion-resistant materials. This not only enhances the longevity of the machine but also maintains hygiene standards, which are particularly important in industries like pharmaceuticals and food processing. The design also incorporates features like easy cleaning and maintenance, with components that can be disassembled and sanitized without compromising the conveyor's structural integrity.
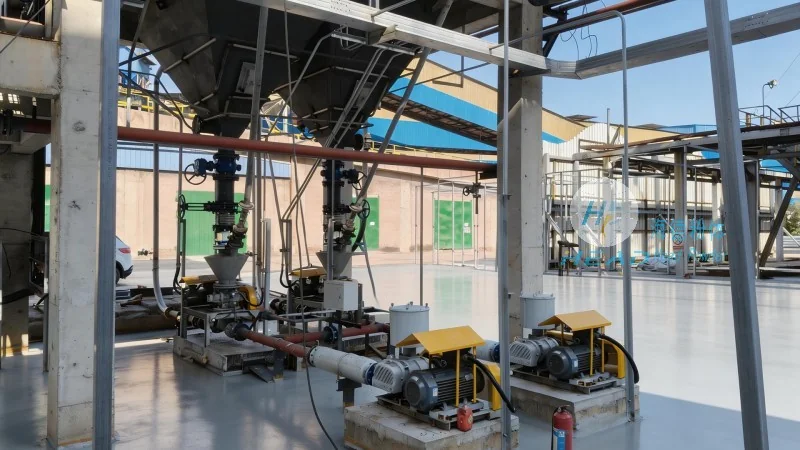
Control systems play a vital role in the design of automatic quantitative powder conveyors. Modern models often feature advanced digital control panels and programmable logic controllers (PLCs), which allow operators to set and adjust parameters such as flow rate, discharge quantity, and cycle timing with ease. These systems can also integrate with other production equipment, enabling seamless automation and data tracking. Additionally, many conveyors are equipped with safety features, including emergency stop buttons, overload protection, and sensors that detect blockages or malfunctions, ensuring safe and reliable operation.
HeadPowder: A Leader in Automatic Quantitative Powder Conveyors
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable manufacturer specializing in the design, development, and production of high-quality automatic quantitative powder conveyors. With a strong commitment to innovation and precision engineering, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient powder handling solutions. The company's products are engineered to meet the stringent demands of various applications, offering customization options to suit specific operational needs.
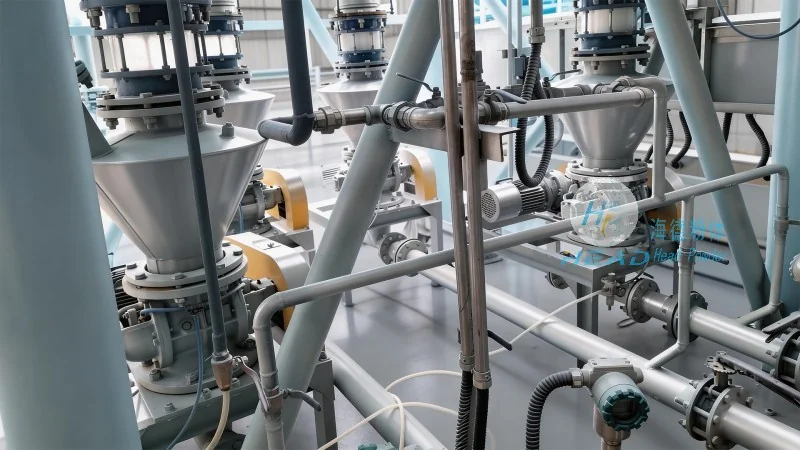
HeadPowder's automatic quantitative powder conveyors are designed with the latest technological advancements, ensuring optimal performance and durability. The company adheres to international quality standards and employs rigorous testing procedures to guarantee the reliability of its equipment. By leveraging years of industry experience and customer feedback, HeadPowder continuously improves its products to deliver superior results for its clients. The company's focus on customer satisfaction and technical support ensures that users receive comprehensive assistance throughout the product lifecycle, from installation to maintenance and troubleshooting.
HeadPowder's facilities are located in Shandong, China, where the company operates a state-of-the-art manufacturing plant equipped with advanced machinery and skilled workforce. This enables the company to produce high-quality powder conveyors that meet global market demands while maintaining competitive pricing. The company's dedication to research and development ensures that its products remain at the forefront of the industry, incorporating the latest innovations in powder handling technology.