

What is a Capsule Powder Conveyor? What are its Design Principles?
For industrial applications that require efficient and reliable powder handling, the capsule powder conveyor stands out as a specialized solution. This equipment is designed to transport bulk powders in a compact and flexible manner, addressing the unique challenges of material flow in various production environments. The following article explores the fundamental aspects of this machinery, including its design principles and operational characteristics.
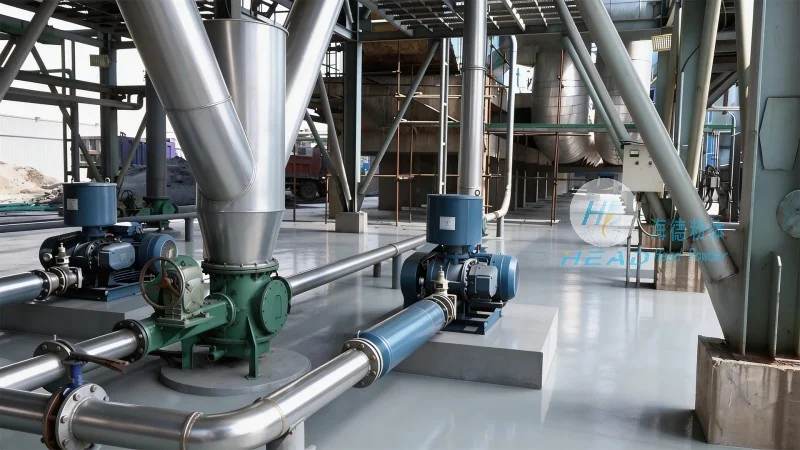
Capsule Powder Conveyor: An Overview
A capsule powder conveyor, also known as a rotary valve or a star feeder, is a type of bulk material handling equipment used to transport dry powders or granules from one location to another within a processing system. The term "capsule" refers to the compact, often cylindrical, housing that encloses the rotating mechanism, which is responsible for moving the material through the system. This design allows for a self-contained and low-profile unit that can be integrated into existing production lines without requiring extensive modifications.
Design Principles of the Capsule Powder Conveyor
The core design of a capsule powder conveyor is centered on the principle of positive displacement. The machine consists of a rotating star or paddle wheel that is enclosed within a sealed housing. As the star rotates, it creates a series of compartments that trap the powder and move it forward in a controlled manner. This mechanism ensures that the material is conveyed without any backflow or spillage, which is critical for maintaining product purity and preventing contamination.
Key design elements include the material of construction, which is typically made from stainless steel or other corrosion-resistant materials to accommodate a wide range of powders, including those that are hygroscopic or abrasive. The housing is designed to be airtight, preventing dust emissions and ensuring compliance with environmental regulations. Additionally, the conveyor features a discharge port at the end of the housing, which allows the material to be released into the next stage of the process. The speed of the rotating star can be adjusted to control the flow rate, providing flexibility in meeting varying production demands.
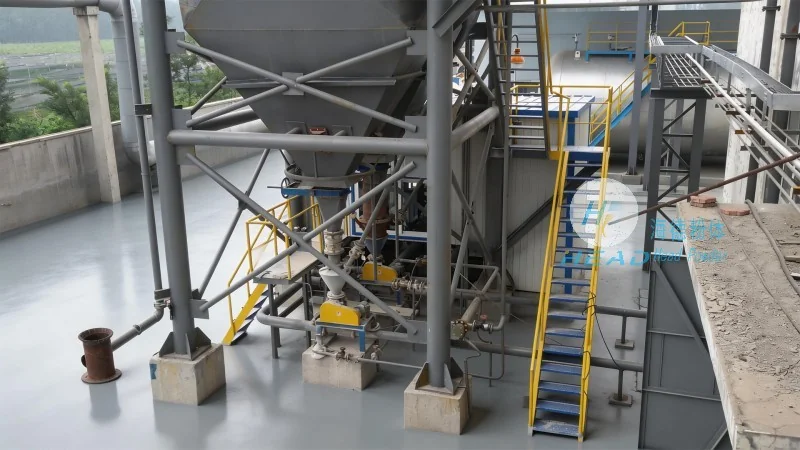
Operational Mechanism and Key Features
The operation of a capsule powder conveyor is straightforward yet highly effective. When the machine is activated, the star wheel begins to rotate, and the powder is drawn into the housing through an inlet port. The rotating paddles then push the powder forward, one compartment at a time, until it reaches the discharge end. This positive displacement method ensures a consistent and predictable flow rate, making it suitable for applications where precise material control is essential, such as in pharmaceutical manufacturing, food processing, or chemical production.
One of the most significant advantages of this design is its ability to handle a wide variety of materials, from fine powders to larger granules. The compact size of the capsule conveyor allows it to fit into tight spaces, making it ideal for retrofitting into existing plants or for use in new installations where space is limited. The airtight construction also minimizes dust generation, which is a major concern in many industrial settings. Furthermore, the equipment is relatively low-maintenance, as the main moving parts are enclosed and protected from direct contact with the material, reducing the risk of wear and tear.
Applications and Industry Use Cases
Due to its versatility and reliability, capsule powder conveyors are widely used in various industries. In the pharmaceutical sector, for example, they are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets strict quality standards. In the food industry, they handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry also relies on these conveyors for transporting powders such as pigments, catalysts, and other raw materials, where consistent flow and purity are paramount.
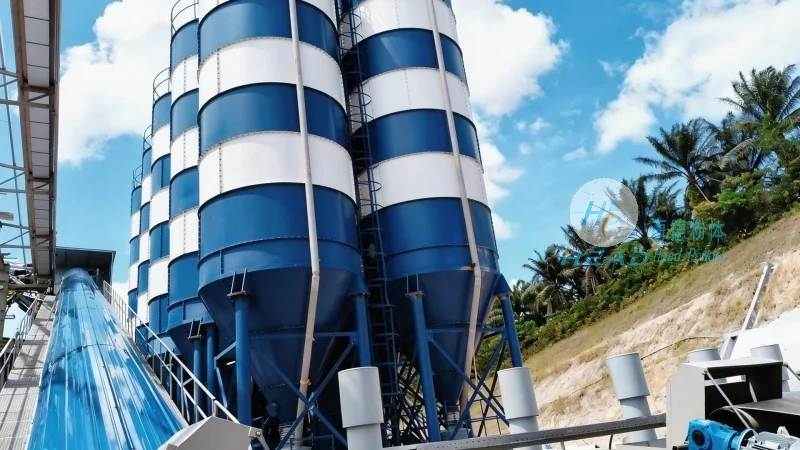
Another common application is in the packaging and blending processes, where the conveyor is used to feed material into mixers or blenders at a controlled rate. The ability to adjust the flow rate makes it suitable for dynamic production environments where demand fluctuates. Additionally, the compact design allows for easy integration with other equipment, such as hoppers, silos, and processing machines, creating a seamless material handling system.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of bulk material handling equipment in China. With a focus on innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient powder processing solutions. HeadPowder's products, including capsule powder conveyors, are designed to meet the specific needs of various applications, ensuring optimal performance and durability.
HeadPowder is headquartered in Shandong, China, where the company operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. The company adheres to strict quality control standards, ensuring that each product meets international specifications and customer requirements. With a commitment to customer satisfaction and continuous improvement, HeadPowder provides comprehensive support, including technical assistance, installation guidance, and after-sales service, to ensure that clients can maximize the benefits of their equipment.