

What is a Sulfur Material Handling Conveyor? And What Are Its Design Principles?
Sulfur, a vital industrial chemical, is widely utilized in the production of fertilizers, chemicals, and other industrial products. Efficient and safe transportation of sulfur is critical for industrial operations. This article explores the concept of sulfur material handling conveyors and examines the design principles that ensure their effective and safe operation.
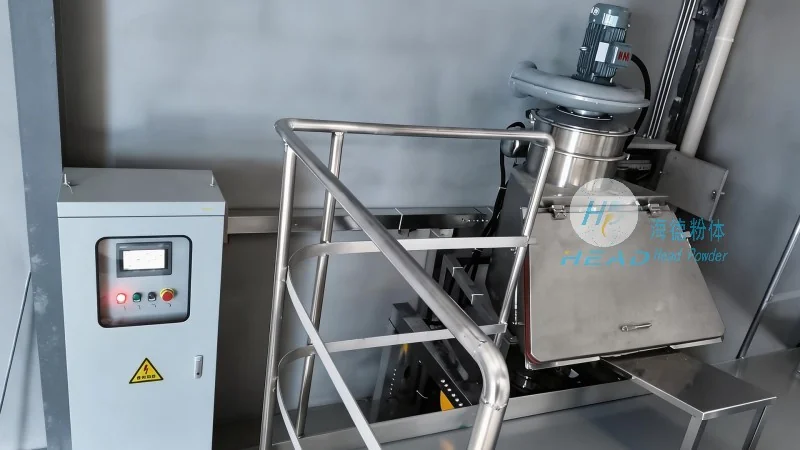
Understanding Sulfur Material Handling Conveyors: Design Principles and Applications
A sulfur material handling conveyor is a specialized system engineered to transport sulfur, typically in the form of solid granules or lumps, from one location to another within industrial facilities. These systems are designed to address the unique properties of sulfur, such as its tendency to adhere to surfaces, its sensitivity to temperature, and its potential for dust generation. The design of these conveyors must tackle these challenges to ensure reliable and safe operation.
Key Characteristics of Sulfur and Their Impact on Conveyor Design
Sulfur is a yellow, crystalline solid existing in various forms, including rhombic and monoclinic. It has a melting point around 115°C (239°F) and is known for its adhesive properties, which can cause material buildup on conveyor surfaces. Additionally, sulfur is a flammable substance, making fire safety a critical consideration in its handling. The chemical reactivity of sulfur also necessitates materials resistant to corrosion and chemical attack. These characteristics directly influence the selection of materials for conveyor components like belts, idlers, and housing.
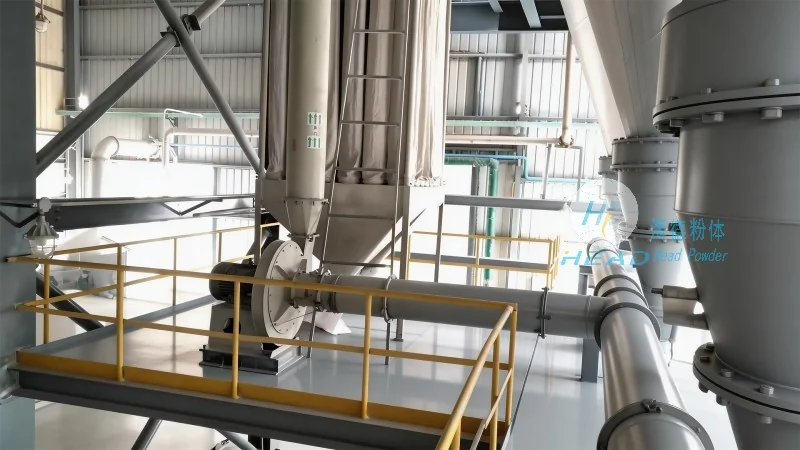
Design Principles for Sulfur Material Handling Conveyors
The design of sulfur material handling conveyors involves several key principles aimed at addressing the unique challenges posed by sulfur. Temperature control is a primary concern, as sulfur can melt and flow at elevated temperatures, leading to blockages or equipment damage. Therefore, conveyor systems often incorporate cooling mechanisms or are designed to operate within specific temperature ranges to prevent sulfur from becoming too fluid. To mitigate the adhesion problem, conveyor surfaces are often treated with anti-stick coatings or designed with self-cleaning features, such as oscillating or vibrating idlers, to prevent material buildup.
Another critical design principle is the use of sealed and explosion-proof components. Sulfur dust is a significant fire and explosion hazard, especially in enclosed spaces. Conveyor systems must be equipped with proper ventilation, dust collection systems, and explosion-proof motors and controls to minimize ignition risk. The selection of materials for conveyor components, such as stainless steel or specialized alloys, is also crucial to resist corrosion and chemical degradation from sulfur and its byproducts.
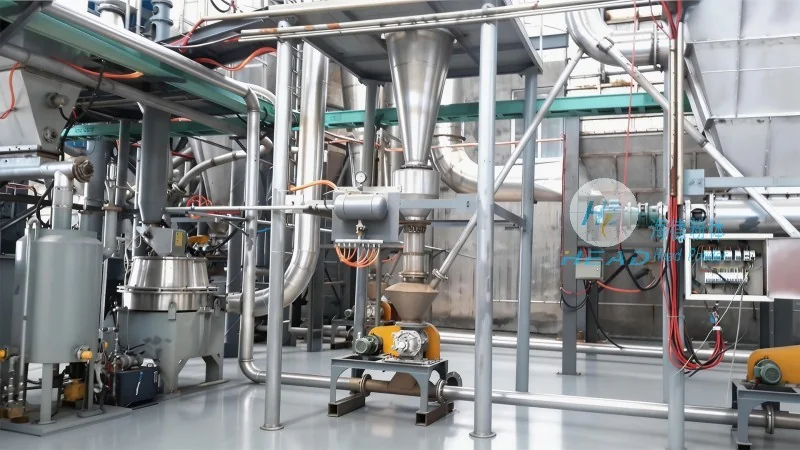
The Role of Shandong HeadPowder Engineering Co., Ltd. in Sulfur Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial material handling solutions, specializes in designing and manufacturing sulfur material handling conveyors tailored to client-specific needs. With years of industry experience, HeadPowder understands the complexities of sulfur handling and applies advanced engineering principles to develop reliable and efficient systems. The company's approach involves thorough analysis of client requirements, including the type of sulfur, production capacity, and operational environment, to design customized conveyor solutions that meet safety standards and operational efficiency.
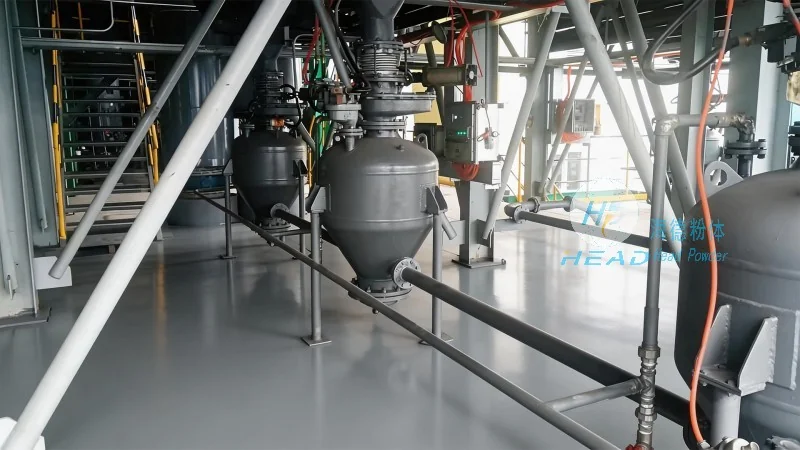
HeadPowder's sulfur material handling systems are built with high-quality materials and components, ensuring durability and long-term performance. The company adheres to international safety and quality standards, such as ISO certifications, to guarantee product safety and reliability. By leveraging its expertise in material handling technology, HeadPowder provides comprehensive solutions that include not only the conveyor systems but also related equipment like feeders, elevators, and storage silos, ensuring a seamless material flow process from raw material to final product.
Conclusion: Ensuring Safe and Efficient Sulfur Transportation
In conclusion, sulfur material handling conveyors are essential for the efficient and safe transportation of sulfur in industrial applications. The design principles governing these systems focus on addressing the unique properties of sulfur, including temperature control, anti-adhesion measures, and fire safety. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing customized and reliable solutions that meet specific client needs, ensuring safe and efficient sulfur handling. By investing in well-designed sulfur material handling systems, industrial facilities can enhance operational safety, improve productivity, and comply with regulatory requirements.