

What is a Stone Aggregate Material Handling System? What are its Design Principles?
Understanding the stone aggregate material handling system equipment and its design principles is crucial for industries that rely on efficient material transport. This equipment is specifically engineered to handle and transport stone aggregates, which are essential raw materials in construction, road building, and other related sectors. The system's design integrates advanced engineering concepts to ensure optimal performance, durability, and safety in material handling operations.
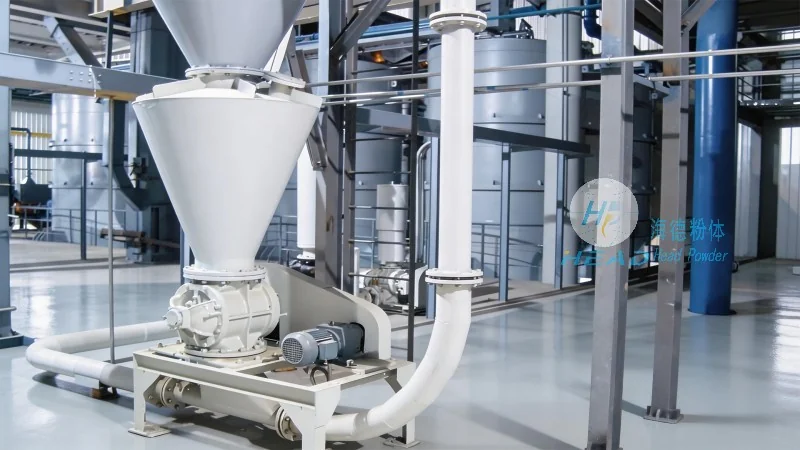
Introduction to Stone Aggregate Material Handling Systems
Stone aggregate material handling systems are specialized equipment designed to transport and manage stone aggregates, which include various sizes of crushed stones, gravel, and sand. These materials are fundamental components in construction projects, serving as bases for roads, foundations, and concrete mixes. The efficiency of material handling directly impacts project timelines, costs, and overall quality. Therefore, the design of such systems must prioritize reliability, adaptability, and energy efficiency to meet the demands of modern industrial applications.
About HeadPowder: A Leading Provider of Material Handling Solutions
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in China, specializing in the design, manufacturing, and supply of advanced material handling equipment. With a strong presence in the industry, HeadPowder has established itself as a trusted partner for businesses seeking reliable solutions for stone aggregate transport. The company's commitment to innovation and quality ensures that its products meet international standards and cater to diverse operational needs.
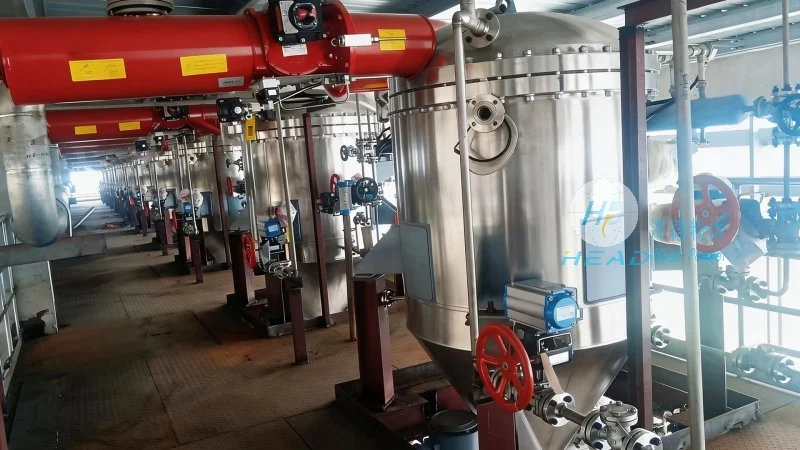
Key Components and Functions of the Material Handling System
The stone aggregate material handling system typically consists of several key components, each playing a vital role in the overall operation. These components may include feeders, conveyors, elevators, and storage silos, all working in tandem to ensure smooth material flow. The feeders are responsible for evenly distributing the stone aggregates into the conveyor system, preventing blockages and ensuring consistent feed rates. The conveyors, often belt or chain-driven, transport the materials over long distances with minimal energy consumption. Elevators are used to lift materials vertically, while storage silos provide temporary storage to regulate the flow and prevent overloading of downstream equipment.
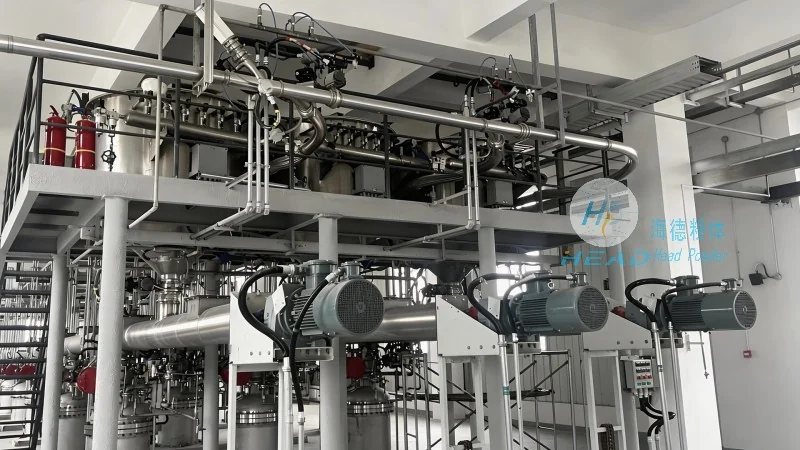
Design Principles Behind the System
The design principles of the stone aggregate material handling system are centered on several critical factors, including material properties, operational efficiency, and safety. The system is designed to accommodate the varying sizes and shapes of stone aggregates, ensuring that no material is left behind or damaged during transport. This is achieved through the use of appropriate feeder designs, such as vibrating feeders or rotary valves, which can handle different particle sizes effectively. Additionally, the system's layout is optimized to minimize the number of components and reduce the risk of material spillage or contamination. The use of durable materials, such as stainless steel or high-strength alloys, ensures that the equipment can withstand the abrasive nature of stone aggregates and operate for extended periods without maintenance.
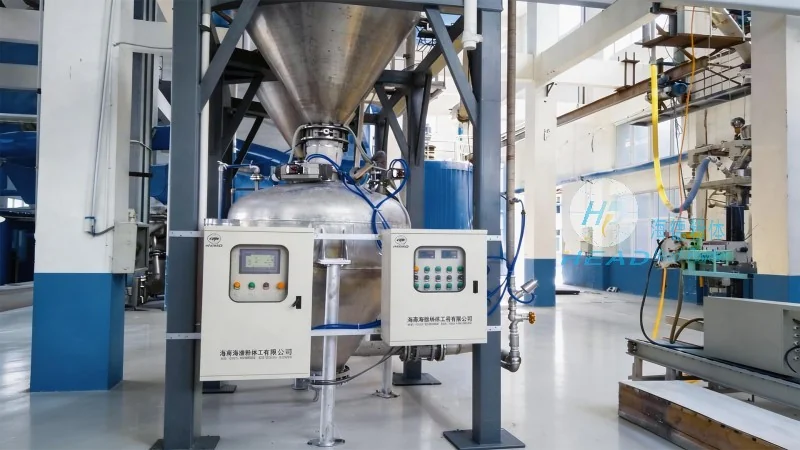
Application and Benefits in Industrial Settings
Stone aggregate material handling systems are widely used in various industrial settings, including construction sites, mining operations, and aggregate processing plants. The primary benefits of these systems include increased productivity, reduced labor costs, and improved safety. By automating the material transport process, businesses can achieve higher throughput rates and minimize the risk of accidents associated with manual handling. The system's design also allows for easy integration with other production equipment, creating a seamless workflow from raw material intake to finished product output. Furthermore, the energy-efficient design of modern systems helps reduce operational costs and environmental impact, making them a sustainable choice for industrial applications.
Conclusion and Future Developments
In conclusion, the stone aggregate material handling system is a sophisticated piece of equipment that plays a vital role in the efficient operation of industries relying on stone aggregates. The design principles behind these systems focus on optimizing material flow, ensuring durability, and enhancing safety. Companies like HeadPowder continue to innovate and improve these systems, incorporating advanced technologies such as automation and smart controls to further enhance performance. As industrial demands evolve, the stone aggregate material handling system will continue to adapt, providing reliable and efficient solutions for the future of material handling.