

What is Quartz Stone Material Pneumatic Conveying? And What Are Its Design Principles?
Quartz stone material pneumatic conveying is a specialized method used in industrial settings to transport quartz stone particles through a pipeline using air or gas as the conveying medium. This technology is essential for efficiently moving quartz stone from one location to another, often in manufacturing, processing, or construction applications. The design principles behind such systems are critical to ensuring reliable, efficient, and cost-effective operation.
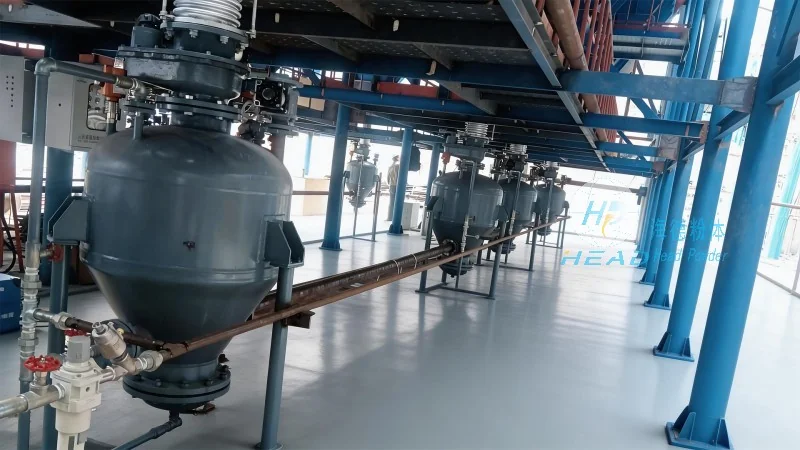
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. With a focus on precision engineering and customer-centric solutions, HeadPowder has established itself as a trusted partner in the industry. The company is headquartered in Shandong, China, and specializes in customizing pneumatic conveying solutions for various materials, including quartz stone. HeadPowder's expertise lies in designing systems that meet the unique requirements of each client, ensuring optimal performance and longevity.
Understanding Quartz Stone Material Pneumatic Conveying
Quartz stone, a hard, crystalline mineral composed primarily of silicon dioxide, is widely used in construction, manufacturing, and decorative applications. Transporting quartz stone via traditional methods like trucks or conveyor belts can be inefficient, costly, and environmentally unfriendly. Pneumatic conveying offers a more efficient alternative, as it eliminates the need for physical contact between the material and the conveying equipment, reducing wear and tear while minimizing dust generation. The process involves creating a pressure differential within a pipeline, where air or gas is used to move the quartz stone particles through the system. This method is particularly advantageous for handling fine or abrasive materials like quartz stone, which can be challenging to transport using conventional means.
Key Design Principles for Quartz Stone Pneumatic Conveying Systems
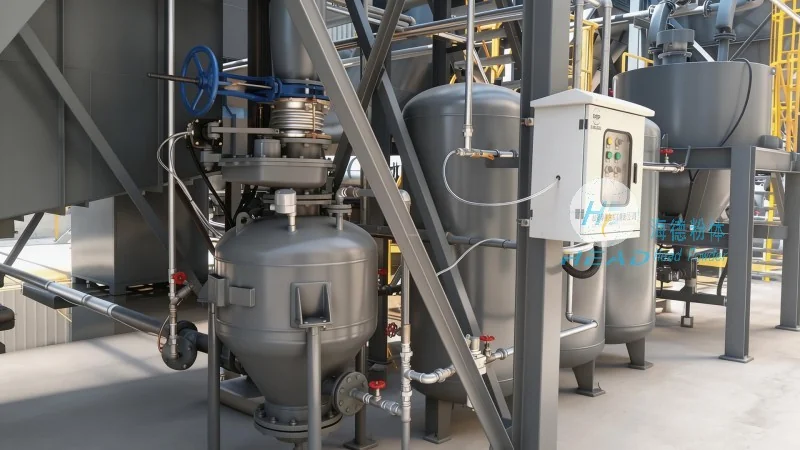
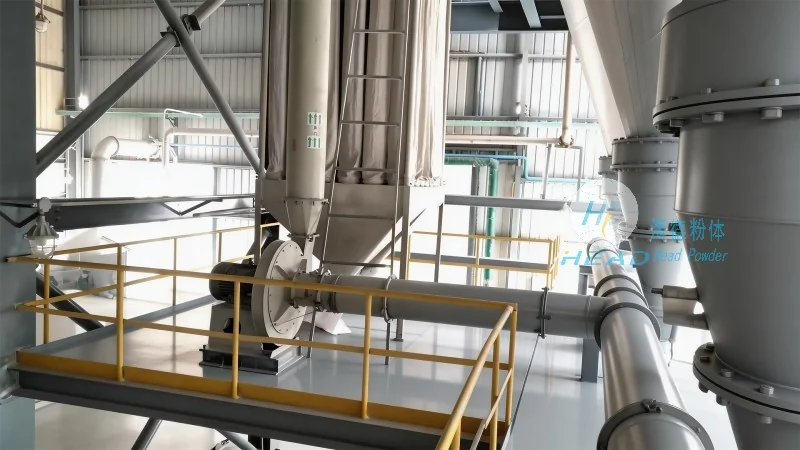
The design of a pneumatic conveying system for quartz stone involves several critical principles to ensure optimal performance. First, the system must be designed to handle the specific properties of quartz stone, such as its particle size, density, and abrasiveness. The pipeline diameter and material must be selected to prevent clogging and ensure smooth flow. For quartz stone, which can be abrasive, high-quality materials like stainless steel or special alloys are often used for the pipeline and components to minimize wear. Second, the air velocity and pressure must be carefully controlled to maintain a stable conveying condition. The system typically operates in either pressure or vacuum mode, with pressure systems being more common for quartz stone due to their ability to handle longer distances and higher material loads. Third, the system must include proper dust collection and filtration to comply with environmental regulations and maintain a clean working environment. HeadPowder's engineers consider all these factors when designing a custom pneumatic conveying system, ensuring that the final solution is both efficient and reliable.
Components and Operation of Quartz Stone Pneumatic Conveying Systems
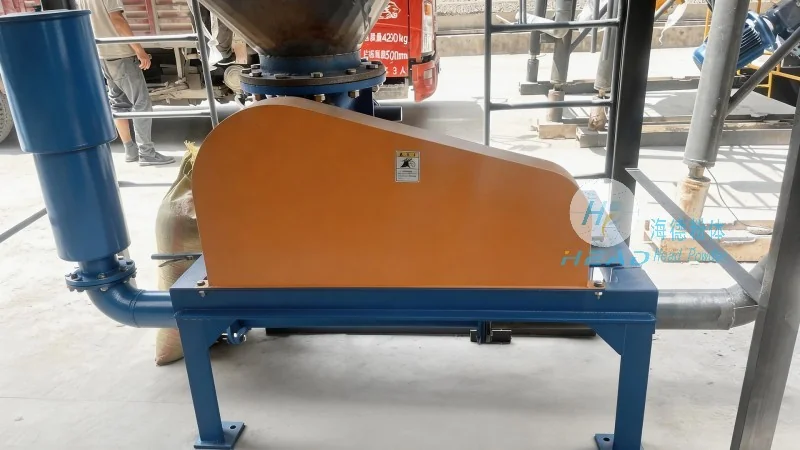
A typical quartz stone pneumatic conveying system consists of several key components, each playing a crucial role in the overall operation. The primary components include the material feed hopper, the conveying pipeline, the air or gas source (usually a blower or compressor), the control system, and the discharge unit. The material feed hopper is designed to hold the quartz stone and feed it into the pipeline at a controlled rate. The pipeline is typically made of durable materials like stainless steel or PVC, with bends and fittings that are carefully designed to minimize pressure loss and prevent material buildup. The air source provides the necessary pressure or vacuum to move the quartz stone through the pipeline. The control system monitors and regulates the flow of material and air, ensuring consistent operation. The discharge unit collects the quartz stone at the end of the pipeline, often with a dust collection system to capture any fine particles. The operation of the system begins with the quartz stone being loaded into the feed hopper. The control system then activates the air source, creating a pressure differential that propels the material through the pipeline. As the quartz stone moves, it is carried by the air stream, and the system continues until the material reaches the discharge point. HeadPowder's systems are designed to operate continuously, with minimal downtime, and are equipped with safety features to prevent overpressure or material blockages.
Advantages of Quartz Stone Pneumatic Conveying
Implementing a pneumatic conveying system for quartz stone offers numerous advantages over traditional transportation methods. One of the most significant benefits is the reduction in labor costs, as the system can operate automatically with minimal human intervention. This also leads to increased productivity, as the system can handle large volumes of material at a consistent rate. Another advantage is the reduction in material handling time and costs, as the system eliminates the need for trucks or conveyor belts, which can be time-consuming and expensive to maintain. Additionally, pneumatic conveying reduces the risk of material contamination, as the system is enclosed and prevents exposure to the environment. This is particularly important for quartz stone, which is often used in high-purity applications like construction or manufacturing. The system also minimizes dust generation, improving workplace safety and reducing the need for extensive dust control measures. Finally, the flexibility of pneumatic conveying systems allows for easy integration with existing production lines, making it a cost-effective solution for many industries.
Customization and Application in Various Industries
HeadPowder understands that each client's needs are unique, and therefore, offers customized pneumatic conveying solutions tailored to specific applications. The company works closely with clients to understand their material requirements, production volume, and operational constraints, then designs a system that meets all these needs. Quartz stone pneumatic conveying systems are widely used in various industries, including construction, where quartz stone is used as a raw material for concrete and other building materials. In manufacturing, the system is used to transport quartz stone to production lines for processing into various products. The system is also used in the decorative stone industry, where quartz stone is used for countertops, tiles, and other architectural elements. HeadPowder's systems have been successfully implemented in these industries, providing reliable and efficient material transport solutions. The company's expertise in custom design ensures that each system is optimized for the specific application, resulting in improved performance and reduced operational costs.
Maintenance and Longevity of Quartz Stone Pneumatic Conveying Systems
Proper maintenance is crucial to ensure the longevity and efficiency of a quartz stone pneumatic conveying system. HeadPowder recommends regular inspections and maintenance to prevent issues before they become major problems. The maintenance schedule typically includes checking the air source for proper operation, inspecting the pipeline for wear or damage, and cleaning the dust collection system. The components of the system, such as the feed hopper and discharge unit, should also be inspected regularly for any signs of wear or clogging. HeadPowder provides maintenance services and spare parts to ensure that clients can keep their systems running smoothly. By following the recommended maintenance procedures, clients can extend the life of their system and minimize downtime. The durability of the system, combined with proper maintenance, ensures that it remains a reliable and cost-effective solution for transporting quartz stone for many years.
Conclusion
Quartz stone material pneumatic conveying is a highly effective and efficient method for transporting quartz stone in industrial applications. The design principles behind such systems are critical to ensuring reliable operation, and companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in designing and manufacturing these systems. By understanding the key design principles and components of a pneumatic conveying system, industries can benefit from reduced costs, increased productivity, and improved safety. HeadPowder's expertise in customizing pneumatic conveying solutions ensures that clients receive a system that meets their specific needs, providing a reliable and efficient solution for their quartz stone transportation requirements.