

Capsule Pneumatic Conveying: An Efficient and Environmentally Friendly Material Handling Solution
Introduction to Capsule Pneumatic Conveying Technology
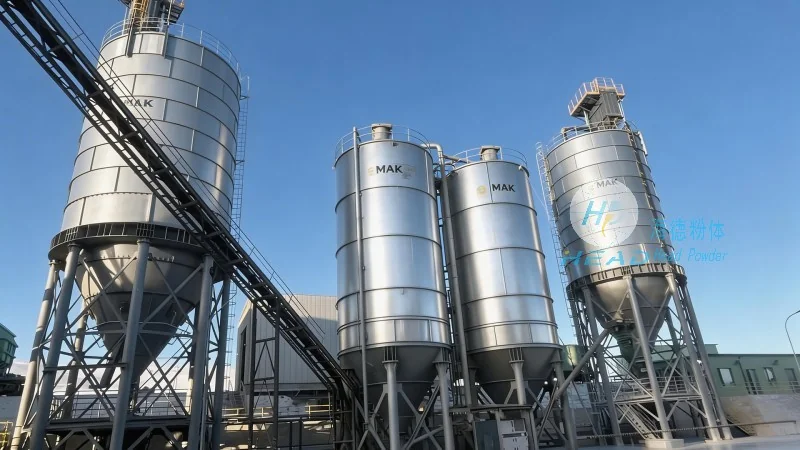
Understanding Capsule Pneumatic Conveying
Capsule pneumatic conveying is a sophisticated material handling system designed to transport bulk materials through a network of pipes using compressed air. Unlike traditional methods like belt conveyors or screw conveyors, this technology employs a unique capsule or hopper mechanism that ensures gentle handling of delicate or abrasive materials. The system operates by creating a low-pressure or high-pressure air flow within the pipeline, which propels the material forward while minimizing wear and tear on both the material and the equipment.
Key Advantages of Capsule Pneumatic Conveying
One of the primary benefits of capsule pneumatic conveying is its efficiency in material transport. By utilizing compressed air to move materials, the system can achieve high throughput rates with minimal downtime. This is particularly advantageous for industries dealing with large volumes of powders or granules, as it reduces the need for multiple transfer points and manual handling. Additionally, the system is highly versatile, capable of handling a wide range of materials, from fine powders to bulk granules, without the risk of clogging or degradation.
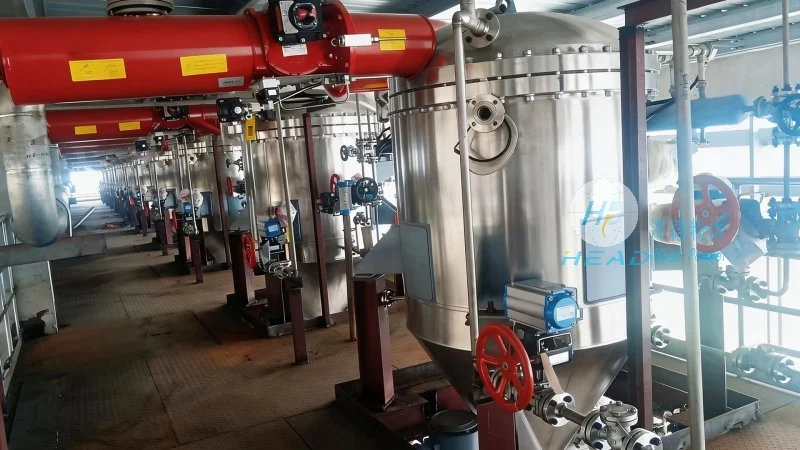
Environmental sustainability is another critical advantage. Unlike traditional conveyor systems that may generate dust or require extensive maintenance, capsule pneumatic conveying operates in a closed-loop system, significantly reducing air pollution and material loss. The enclosed pipeline design ensures that dust and particulates are contained, making it an ideal solution for applications where environmental compliance is a priority. Furthermore, the system’s energy efficiency, as it minimizes energy consumption compared to other bulk material handling methods, contributes to lower operational costs and a smaller carbon footprint.
How Capsule Pneumatic Conveying Works
The operation of a capsule pneumatic conveying system involves several key components. At the source, the material is loaded into a hopper or silo, where it is then fed into a capsule—a flexible or rigid container that carries the material through the pipeline. The capsule travels along the pipeline, propelled by compressed air, and is released at the destination point. The system typically includes a control unit that regulates air pressure and flow, ensuring smooth and consistent material transport. The design allows for easy integration with existing production lines, making it a flexible solution for various industrial applications.
Applications and Industries
Capsule pneumatic conveying is widely used across multiple industries due to its adaptability and efficiency. In the pharmaceutical industry, for example, it is used to transport sensitive powders and granules with minimal contamination, ensuring product quality and safety. The food and beverage industry also benefits from this technology, as it maintains hygiene standards while handling various ingredients. Additionally, in the chemical and mining sectors, capsule pneumatic conveying is employed to transport abrasive or corrosive materials without damaging the equipment or the material itself. The system’s ability to handle diverse materials makes it a preferred choice for industries that require precise and reliable material handling solutions.
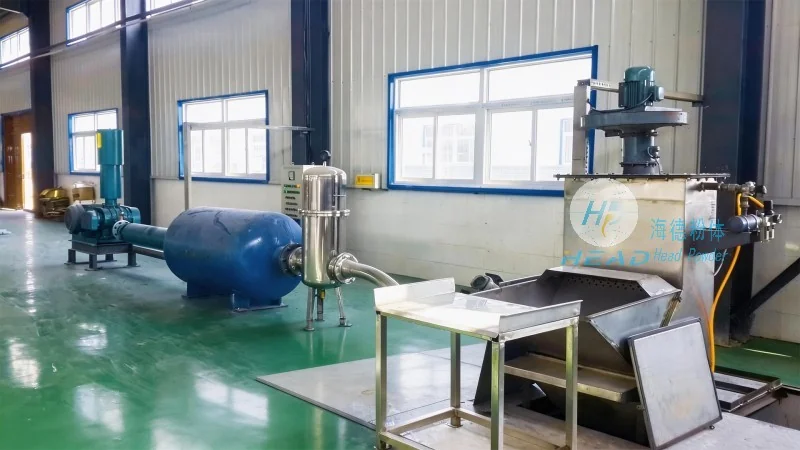
Why Choose Shandong HeadPowder Engineering Co., Ltd. for Capsule Pneumatic Conveying Solutions
For businesses seeking reliable and efficient capsule pneumatic conveying systems, Shandong HeadPowder Engineering Co., Ltd. is a leading provider. With years of experience in the engineering and manufacturing of material handling solutions, the company specializes in designing and installing customized systems tailored to specific industry needs. The team at HeadPowder leverages advanced technology and rigorous quality control to ensure that each system meets the highest standards of performance and durability. By choosing HeadPowder, clients gain access to expert consultation, comprehensive installation services, and ongoing support to optimize their material handling processes. The company’s commitment to innovation and customer satisfaction makes it a trusted partner for industries looking to enhance their operational efficiency and environmental sustainability.
Conclusion
Capsule pneumatic conveying represents a significant advancement in bulk material handling, offering a combination of efficiency, versatility, and environmental responsibility. As industries continue to prioritize operational excellence and sustainability, this technology remains a top choice for businesses seeking reliable solutions. With the expertise and dedication of companies like Shandong HeadPowder Engineering Co., Ltd., the implementation of capsule pneumatic conveying systems has become more accessible and effective, enabling organizations to streamline their material transport processes and achieve their operational goals.