

Principle and Working Scene Characteristics of Manganese Sulfate Powder Conveying System
Exploring the Manganese Sulfate Powder Conveying System: Core Principles and Practical Applications
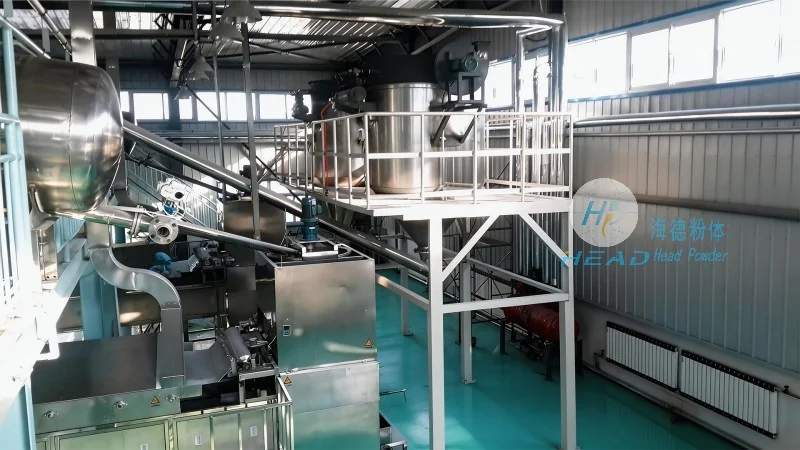
Introduction to Manganese Sulfate Powder Conveying Systems
HeadPowder Engineering, a prominent entity in the field, specializes in the development and deployment of efficient manganese sulfate powder conveying systems. These systems are vital for industries that depend on the precise handling and transportation of manganese sulfate, a key chemical compound utilized in battery manufacturing, fertilizer production, and water treatment. The essence of these systems lies in their ability to transport dry powders while preserving the powder's integrity and ensuring smooth, reliable operation across diverse industrial environments.
Key Principles Underpinning Manganese Sulfate Powder Conveying
The fundamental principle of manganese sulfate powder conveying systems revolves around mechanical or pneumatic methods to move dry powders without compromising quality. Mechanical systems, such as screw conveyors, belt conveyors, and bucket elevators, are employed for bulk handling, offering high efficiency and low maintenance. Pneumatic systems utilize air pressure to transport powder through pipelines, ideal for applications requiring minimal contamination and precise flow control. Both approaches are engineered to maintain the physical properties of manganese sulfate, preventing agglomeration and ensuring consistent particle size distribution.
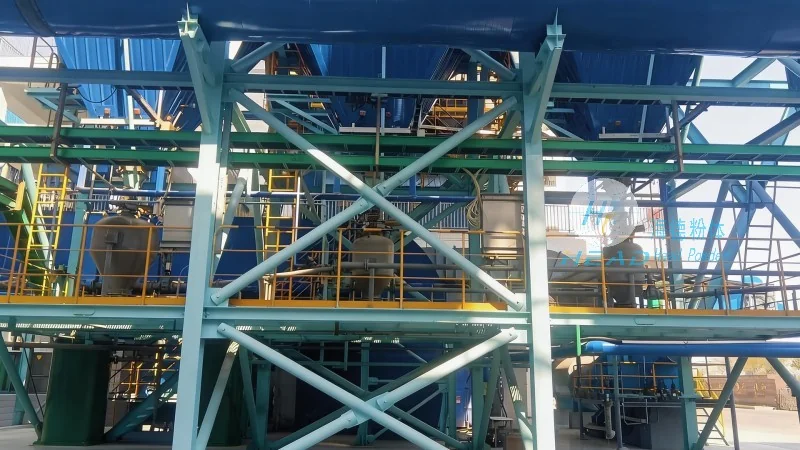
Working Scene Characteristics and Real-World Applications
The working scene characteristics of manganese sulfate powder conveying systems are tailored to specific industrial demands. In battery production facilities, these systems are designed for large-scale, clean handling to avoid dust accumulation and maintain product purity. Fertilizer plants require high-throughput, durable systems operating under continuous, demanding conditions. Water treatment facilities benefit from systems that minimize clogging and ensure consistent dosing for purification. Each application leverages the system's ability to adapt to operational requirements while optimizing material flow and safety.
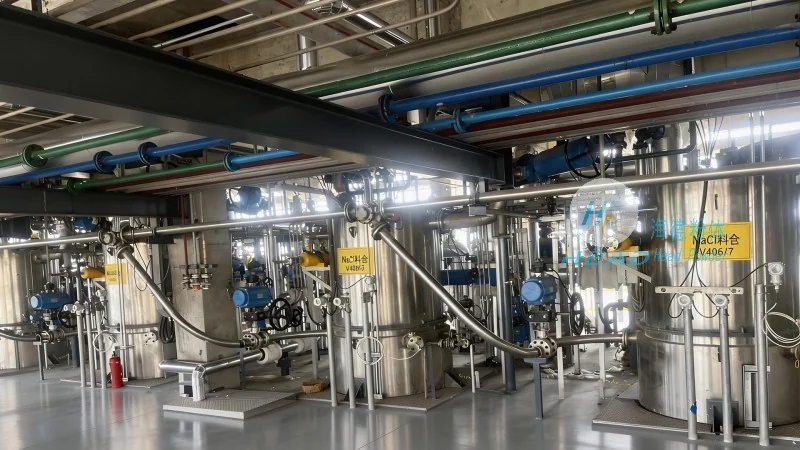
Technical Advantages and Operational Efficiency
HeadPowder Engineering's manganese sulfate powder conveying systems offer advanced technical advantages, including robust material handling, dust suppression, and automated control. These features enhance operational efficiency, reduce downtime, and ensure compliance with industrial standards. The modular design allows seamless integration into existing production lines, providing flexibility for evolving production needs. By prioritizing durability and precision, these systems deliver reliable performance in high-stakes industrial environments.
Conclusion: The Critical Role of Manganese Sulfate Powder Conveying Systems
In summary, manganese sulfate powder conveying systems are indispensable for industries reliant on manganese sulfate. The principles and working scene characteristics, exemplified by HeadPowder Engineering's solutions, underscore their effectiveness in ensuring efficient, safe, and reliable transportation. By aligning system design with specific application requirements, industries can optimize production processes, enhance product quality, and achieve sustainable operational performance.