

Principles and Working Scene Characteristics of the Biological Enzyme Powder Transport System Equipm
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, development, and manufacturing of advanced biological enzyme powder transport systems. Based in Shandong, China, the company has established itself as a trusted provider of innovative solutions tailored to the unique demands of various industrial applications.
Understanding the Core Principles of the Biological Enzyme Powder Transport System
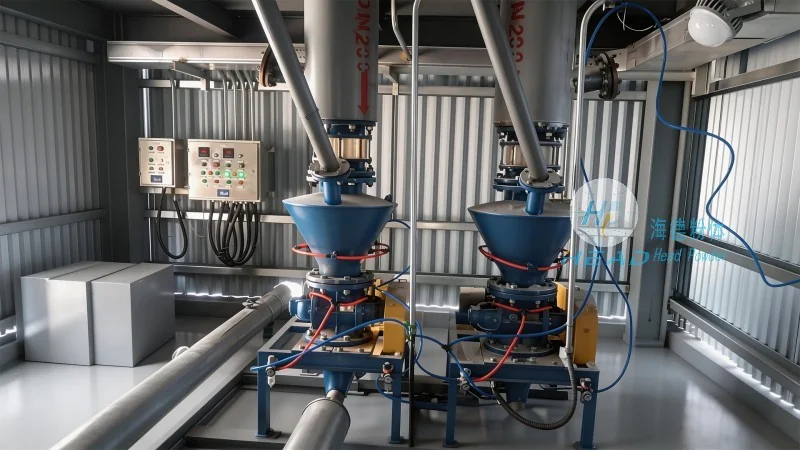
The biological enzyme powder transport system is engineered to efficiently handle and transport powdered materials that contain biological enzymes. This equipment leverages advanced pneumatic conveying technologies, ensuring precise control over the flow, pressure, and velocity of the powder stream. The system incorporates specialized components such as rotary valves, airlocks, and flexible hoses, which work in tandem to maintain the integrity of the enzyme powder while minimizing degradation or contamination. The core principle revolves around the use of compressed air to create a consistent flow, enabling seamless movement of the powder from the source to the destination. This approach not only enhances operational efficiency but also preserves the biological activity of the enzymes, which is critical for applications in pharmaceuticals, food processing, and biotechnology.
Key Working Scene Characteristics and Applications
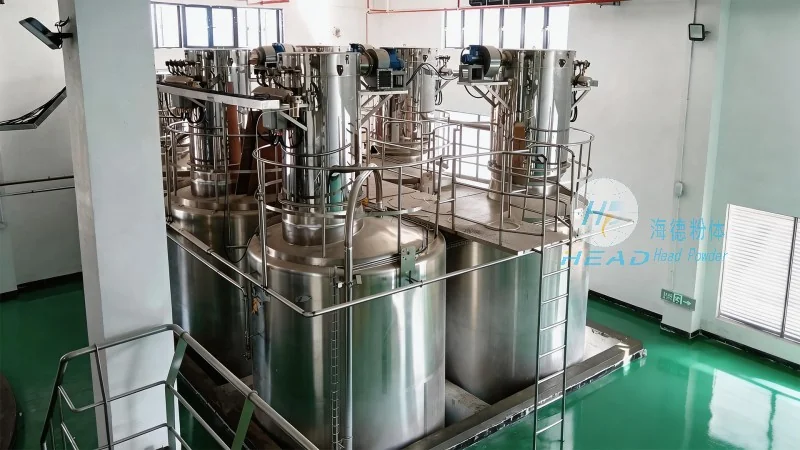
The biological enzyme powder transport system is particularly well-suited for a range of industrial environments where the handling of sensitive biological powders is essential. These systems are commonly deployed in pharmaceutical manufacturing facilities, where the need for sterile and contamination-free transport of enzymes used in drug production is paramount. In the food industry, the equipment is utilized to transport enzymes used in processes like cheese ripening, baking, and protein modification, ensuring that the final products meet stringent quality and safety standards. Additionally, in the biotechnology sector, the system supports the transport of enzymes used in research and development, biocatalysis, and industrial bioprocessing, where maintaining the enzyme's activity is crucial for optimal performance.
Advantages and Technical Specifications
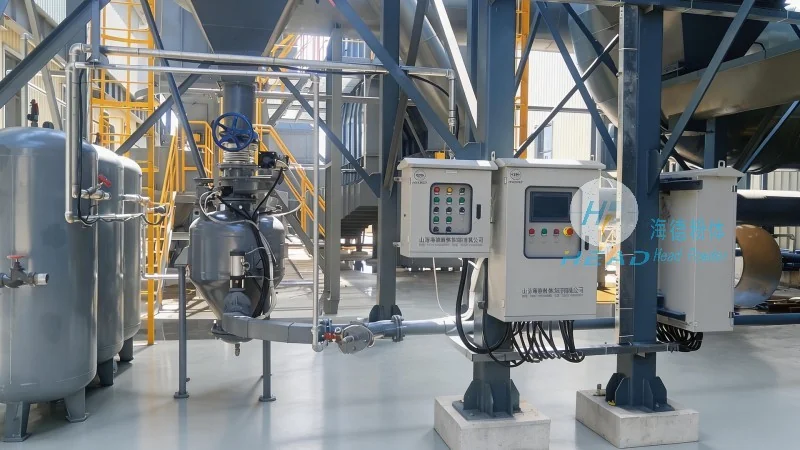
One of the standout features of the HeadPowder biological enzyme powder transport system is its ability to handle a wide variety of powder types, including fine powders, agglomerates, and powders with high moisture content. The system's modular design allows for easy integration into existing production lines, reducing downtime and installation costs. Technical specifications include adjustable conveying velocities, pressure control mechanisms, and customizable hopper sizes to accommodate different batch sizes and material properties. The equipment is also equipped with safety features such as pressure relief valves and overcurrent protection, ensuring reliable operation and compliance with industrial safety regulations. Furthermore, the system's low maintenance requirements and energy-efficient operation contribute to long-term cost savings for users.
Conclusion and Company Commitment
HeadPowder Engineering Co., Ltd. remains committed to delivering high-quality, reliable biological enzyme powder transport systems that meet the evolving needs of modern industries. By combining advanced engineering with a deep understanding of powder handling challenges, the company continues to provide solutions that enhance productivity, ensure product quality, and support sustainable manufacturing practices. With a strong presence in Shandong, China, HeadPowder stands ready to serve clients globally, offering tailored solutions that drive success in the biopharmaceutical, food, and biotechnology sectors.