

Principle and Working Scene Characteristics of Copper Sulfate Material Pneumatic Conveying Machine
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier of industrial conveying equipment. Based in Shandong, China, the company specializes in the design, development, and production of advanced pneumatic conveying systems tailored for various industrial applications.
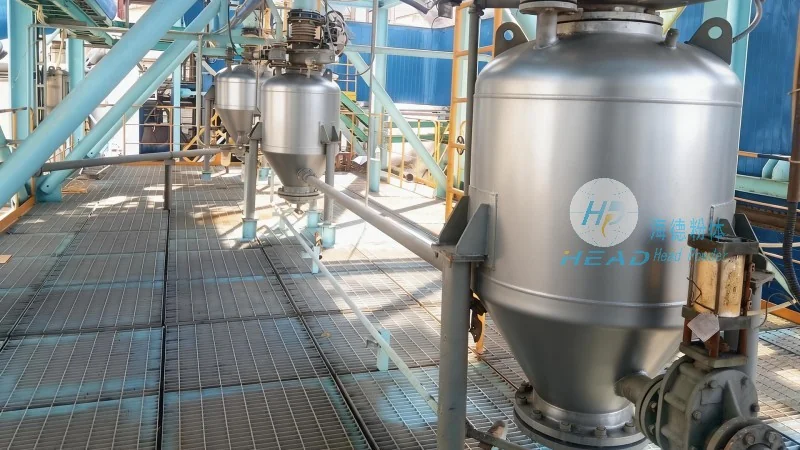
Advanced Copper Sulfate Pneumatic Conveying System
HeadPowder's copper sulfate material pneumatic conveying machine is engineered to efficiently transport copper sulfate, a widely used chemical in industries such as agriculture, water treatment, and chemical manufacturing. This system integrates cutting-edge technology to ensure reliable and safe material handling, addressing the unique challenges associated with copper sulfate's properties, including its hygroscopic nature and potential for dust generation during handling.
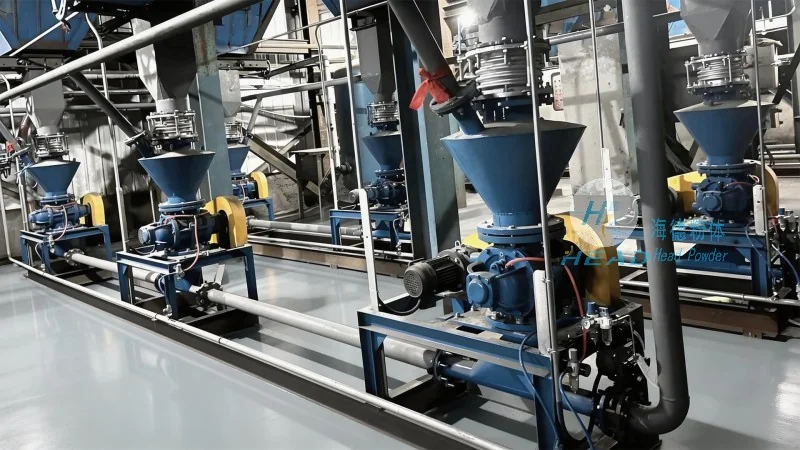
Working Principle of the Pneumatic Conveying Machine
The core of the copper sulfate pneumatic conveying system is the pneumatic conveying mechanism, which utilizes compressed air to transport bulk materials through a pipeline network. The system typically operates on the principle of air-assisted transport, where material is fed into a hopper and then conveyed through a series of pipes by the force of the air flow. Key components include the air compressor, material feeder, conveying line, and dust collector. The air compressor generates the necessary pressure to move the material, while the feeder controls the flow rate to maintain consistent conveying efficiency. The conveying line, often made of corrosion-resistant materials like stainless steel, ensures durability and resistance to the chemical properties of copper sulfate. The dust collector is integrated to capture and filter any airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment.
Characteristics of Working Scenarios
The copper sulfate pneumatic conveying machine is designed for diverse industrial environments, offering flexibility and adaptability to different operational needs. In agricultural settings, it facilitates the efficient distribution of copper sulfate as a fungicide or nutrient supplement, reducing manual handling risks and improving operational efficiency. In water treatment facilities, the system ensures precise dosing of copper sulfate for disinfection and water purification processes, maintaining consistent water quality standards. Additionally, in chemical manufacturing plants, the machine supports seamless integration into production lines, enabling continuous material flow and minimizing downtime. The system's ability to handle varying material flow rates and pressures makes it suitable for both small-scale and large-scale operations, catering to the specific requirements of each application.
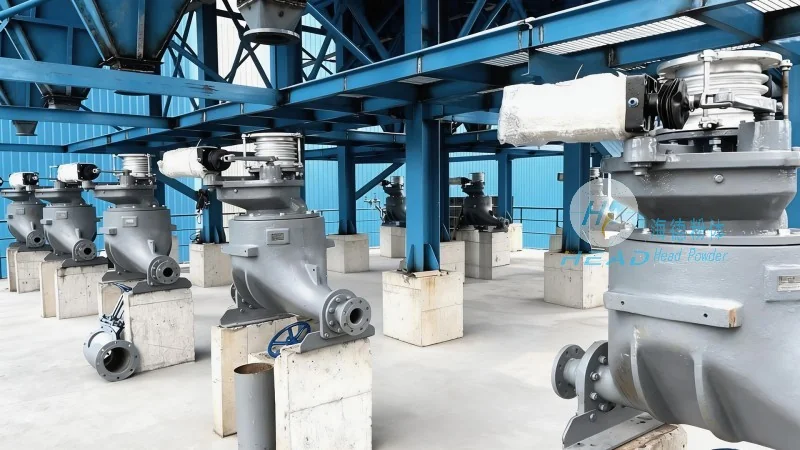
Advantages in Practical Applications
Implementing HeadPowder's copper sulfate pneumatic conveying machine brings several key advantages to industrial operations. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual loading and unloading. This not only improves safety by minimizing exposure to dust and chemical fumes but also enhances productivity through consistent and reliable material transport. Secondly, the system minimizes material loss and contamination, as the enclosed pipeline design prevents dust dispersion and ensures that the material remains in a controlled environment. This is particularly important for copper sulfate, which can be hazardous if inhaled or come into contact with skin. Thirdly, the equipment is designed for easy maintenance and cleaning, with components that can be quickly disassembled and sanitized, reducing downtime and maintenance expenses. The system's energy efficiency is another notable benefit, as modern air compressors and optimized pipe designs minimize energy consumption while maintaining high conveying performance.