

Operation Process and Working Principle of Soda Ash Powder Pneumatic Conveying Machine
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. This article provides a comprehensive overview of the operation process and working principles of a soda ash powder pneumatic conveying machine, highlighting its efficiency, reliability, and the technical aspects that make it a preferred choice in the chemical industry.
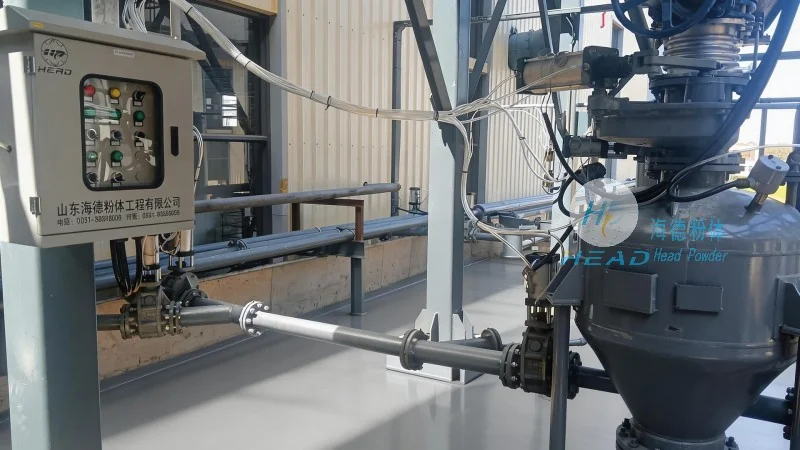
Working Principle of the Pneumatic Conveying System
The core of a soda ash powder pneumatic conveying machine lies in its pneumatic conveying technology, which uses compressed air to transport bulk powder materials. The system typically consists of a hopper, a feeder, a pipeline, and a receiver. The working principle involves several key steps: first, the soda ash powder is fed into the hopper from the storage silo. Then, the feeder regulates the flow rate of the powder into the pipeline. Compressed air is introduced into the pipeline, creating a pressure differential that propels the powder particles forward. The powder and air mixture travels through the pipeline to the receiver, where the powder is separated from the air and collected. The air is then discharged back into the system or vented to the atmosphere, completing the cycle.
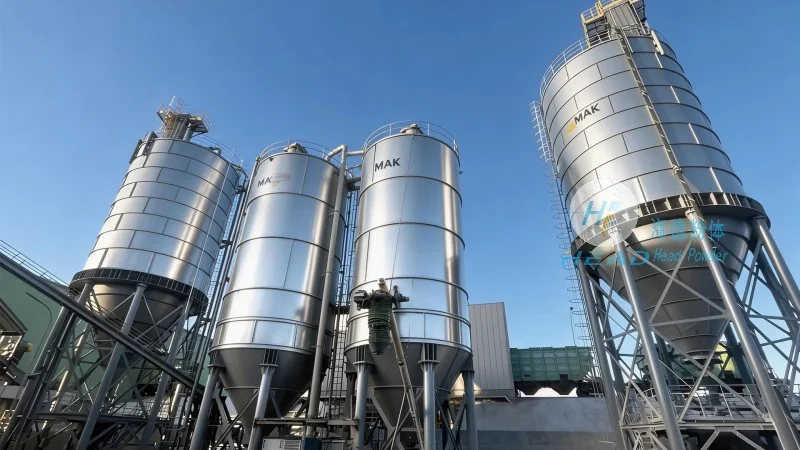
Operation Process of the Machine
The operation process of a soda ash powder pneumatic conveying machine is designed to be automated and efficient, ensuring consistent and reliable material transport. The process begins with the loading of soda ash powder into the hopper. The feeder, often a rotary valve or a screw feeder, controls the discharge rate of the powder into the conveying line. The compressed air system, which is usually connected to an air compressor, provides the necessary pressure to move the powder. The air flow rate is adjusted to match the powder flow rate, maintaining optimal conveying conditions. During operation, the system continuously monitors pressure, flow rate, and temperature to ensure smooth operation. If any issues arise, such as blockages or pressure drops, the system has built-in safety features that automatically shut down the feeder or alert operators. This ensures the safety of the equipment and the quality of the conveyed material.
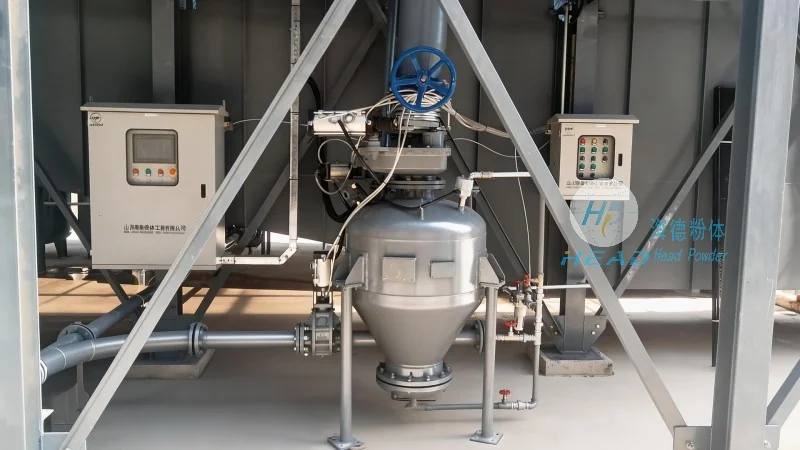
Key Components and Their Functions
Several critical components work together to ensure the effective operation of the soda ash powder pneumatic conveying machine. The hopper serves as the storage and feeding container, holding the soda ash powder and providing a consistent feed to the feeder. The feeder, typically a rotary valve or a star feeder, regulates the flow rate of the powder, preventing overfeeding or underfeeding. The pipeline, made of materials resistant to soda ash powder and air, transports the powder and air mixture. The receiver collects the powder after it is separated from the air, often equipped with a dust collection system to minimize environmental impact. The air compressor and air treatment system provide the compressed air needed for conveying, ensuring it is clean and dry to prevent contamination of the soda ash powder. The control system, which may include sensors and a programmable logic controller (PLC), monitors and controls all aspects of the operation, from feed rate to air pressure.
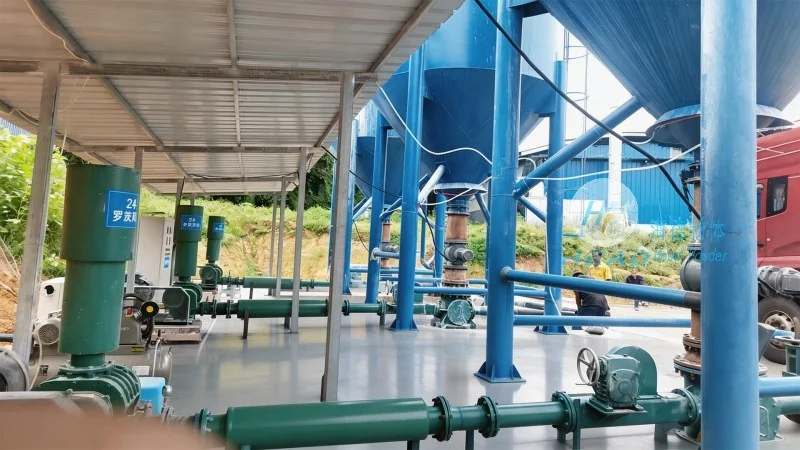
Advantages of Using a Pneumatic Conveying Machine for Soda Ash Powder
Employing a soda ash powder pneumatic conveying machine offers several advantages over traditional methods like belt conveyors or bucket elevators. Firstly, it provides a completely enclosed system, which prevents dust contamination and protects the environment. This is particularly important for soda ash powder, which can be harmful if inhaled. Secondly, the system is highly efficient, with minimal material loss and reduced maintenance requirements. The enclosed design also reduces the risk of product degradation due to exposure to air or moisture. Additionally, the pneumatic conveying system can handle varying particle sizes and flow rates, making it versatile for different production needs. The automated operation reduces labor costs and increases productivity, as the system can run continuously without constant human intervention. Finally, the system is easy to install and integrate into existing production lines, with minimal space requirements compared to other bulk material handling solutions.