

Operation Process and Working Principle of Pneumatic Conveying for Rice Husk Ash Materials
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of efficient pneumatic conveying systems tailored for handling rice husk ash materials. This technology is crucial for industries dealing with bulk solid materials, offering a reliable and cost-effective method to transport these materials over long distances without the need for mechanical components like belts or buckets. The pneumatic conveying system for rice husk ash materials operates by using a stream of air to move the material through a pipeline network, ensuring minimal product degradation and high transfer efficiency.
Key Components of the Pneumatic Conveying System
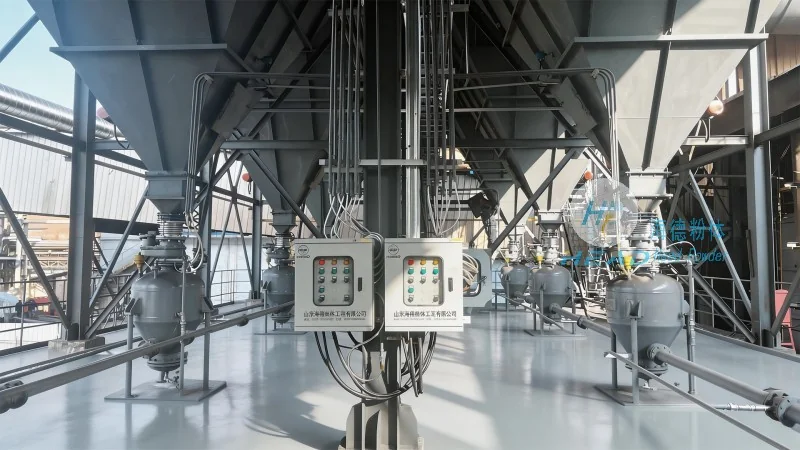
The pneumatic conveying system for rice husk ash materials consists of several critical components that work in tandem to ensure smooth operation. These include the material feed hopper, which stores and feeds the rice husk ash into the system; the air compressor, which generates the necessary air pressure to move the material; the conveying pipeline, which transports the material from the source to the destination; and the discharge equipment, which collects the material at the end of the pipeline. Each component is carefully selected and sized to match the specific characteristics of the rice husk ash, such as its particle size, density, and moisture content, ensuring optimal performance.
Operation Process of the Pneumatic Conveying System
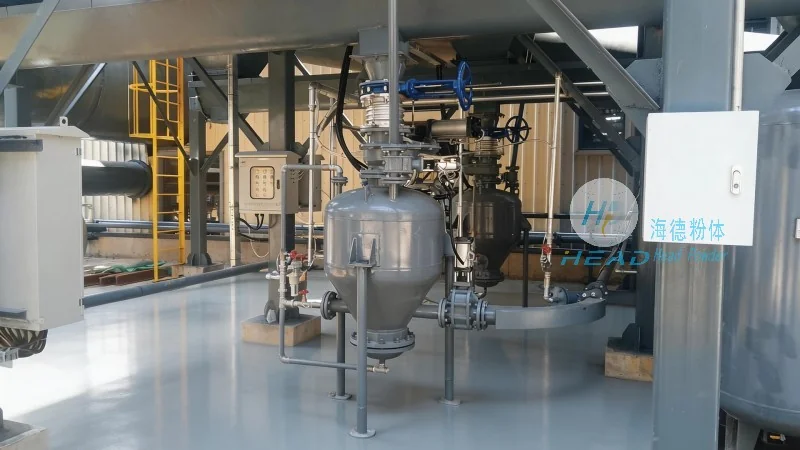
The operation process of the pneumatic conveying system for rice husk ash materials begins with the material being loaded into the feed hopper. The hopper is equipped with a feeder that controls the flow rate of the material into the system. Simultaneously, the air compressor starts and generates a high-pressure air stream. The feeder then releases the rice husk ash into the pipeline, where the air stream lifts and transports the material through the pipeline. The material is carried by the air stream until it reaches the discharge point, where the air velocity decreases, allowing the material to settle and be collected. The system operates continuously, with the air compressor maintaining a consistent pressure to ensure uninterrupted material transfer. The entire process is automated, with sensors monitoring the pressure, flow rate, and material level to ensure the system runs smoothly and efficiently.
Working Principle of the Pneumatic Conveying System
The working principle of the pneumatic conveying system for rice husk ash materials is based on the principle of fluidization and suspension. The air compressor provides a high-pressure air stream that creates a low-pressure zone in the pipeline. As the rice husk ash is introduced into the pipeline, the air stream lifts the particles, suspending them in the air stream. The particles are then transported through the pipeline due to the momentum of the air stream. The velocity of the air stream is carefully controlled to ensure that the particles remain suspended without settling or clogging the pipeline. The system uses either positive pressure or negative pressure (or a combination of both) to move the material, depending on the application requirements. Positive pressure systems are commonly used for short-distance and high-volume applications, while negative pressure systems are used for long-distance and low-volume applications. The choice of system depends on factors such as the distance between the source and destination, the volume of material to be transported, and the cost considerations.
Advantages of Using Pneumatic Conveying for Rice Husk Ash Materials
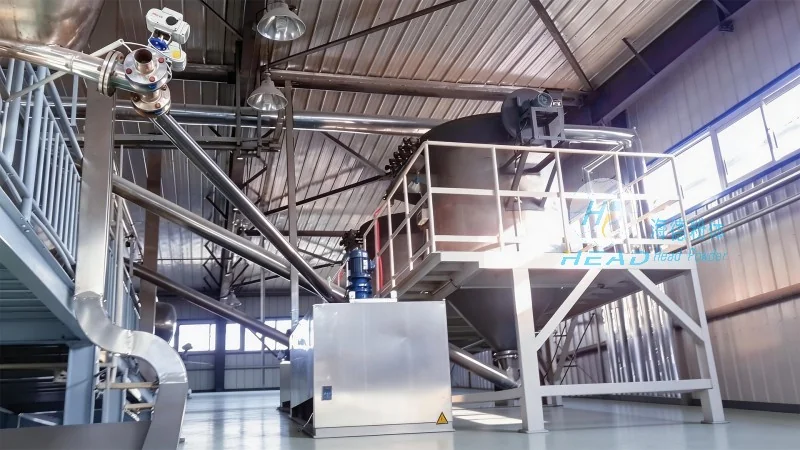
There are several advantages to using pneumatic conveying systems for rice husk ash materials. First, the system is highly efficient, with minimal material loss and high transfer rates. The material is transported in a closed pipeline, which prevents contamination and dust emissions, making it suitable for applications where environmental control is important. Second, the system is flexible, as it can be easily modified to accommodate changes in the material flow rate or the distance between the source and destination. Third, the system is low maintenance, as it has fewer moving parts compared to mechanical conveying systems, reducing the risk of breakdowns and maintenance costs. Fourth, the system is safe, as it eliminates the need for manual handling of the material, reducing the risk of accidents and injuries. Finally, the system is cost-effective, as it reduces the need for additional equipment and labor, resulting in lower operational costs.

Applications of Pneumatic Conveying Systems for Rice Husk Ash Materials
Pneumatic conveying systems for rice husk ash materials are used in a variety of applications, including the transportation of rice husk ash from the processing plant to storage facilities, the transfer of rice husk ash to other processing units, and the delivery of rice husk ash to end-users. The system is also used in the production of rice husk ash-based products, such as activated carbon and biochar, where the material needs to be transported to the production line. The system is suitable for both small and large-scale applications, with the ability to handle high volumes of material over long distances. The flexibility of the system allows it to be integrated into existing production lines, minimizing the disruption to the operation.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of pneumatic conveying systems for rice husk ash materials. The company specializes in the design, manufacturing, and installation of efficient and reliable systems that meet the specific needs of its clients. The company's team of experienced engineers and technicians work closely with clients to understand their requirements and provide customized solutions that optimize the performance and efficiency of the system. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for industries dealing with rice husk ash materials. The company's systems are designed to be durable, low-maintenance, and cost-effective, ensuring that clients receive the best value for their investment. With its headquarters in Shandong, China, HeadPowder serves clients both domestically and internationally, providing high-quality pneumatic conveying systems that meet the highest standards of performance and reliability.