

Introduction to Tonne Bag Unloading Pneumatic Conveying Equipment: Structure and Working Principle E
HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. The company's core focus is on providing efficient and reliable equipment for material handling, particularly in industrial applications where bulk materials need to be transferred from large bags or containers.
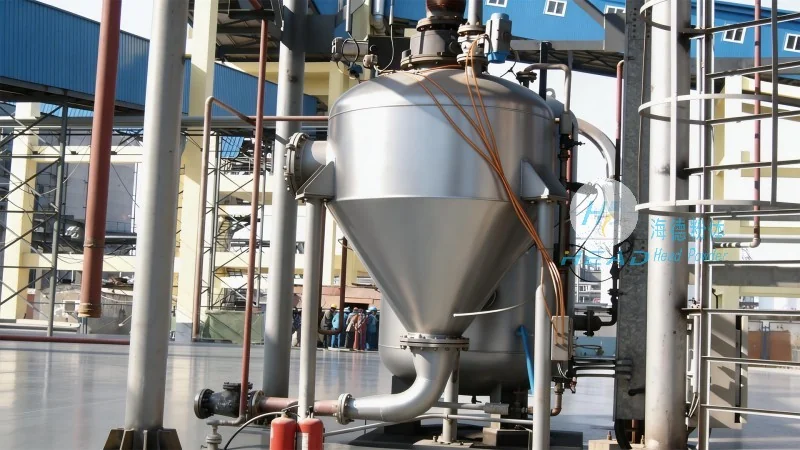
About HeadPowder: A Leading Provider of Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to innovation in material handling technology. With a strong presence in the industry, the company has built a solid reputation for delivering high-quality pneumatic conveying equipment. HeadPowder's headquarters is located in Shandong, China, where the company leverages local manufacturing capabilities and expertise to meet global market demands. The company's commitment to quality, safety, and efficiency has made it a trusted partner for businesses seeking reliable solutions for bulk material transport.
Tonne Bag Unloading Pneumatic Conveying Equipment Overview
The tonne bag unloading pneumatic conveying equipment is a specialized system designed to efficiently transfer bulk materials from large, flexible containers known as tonne bags. This equipment is widely used in industries such as chemicals, food processing, pharmaceuticals, and mining, where handling large volumes of powders or granules is essential. The system combines the advantages of pneumatic conveying with the convenience of automated tonne bag unloading, reducing manual labor and improving operational efficiency.
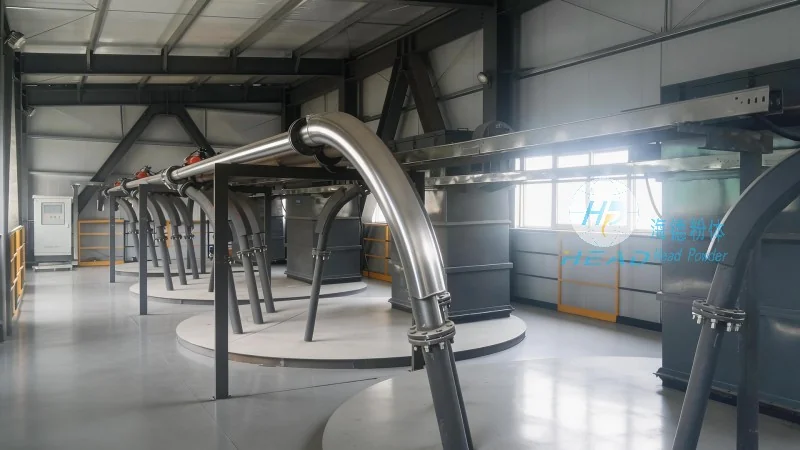
Structural Design and Working Principle of the Equipment
The tonne bag unloading pneumatic conveying equipment consists of several key components, each playing a crucial role in the overall operation. The primary components include a bag opening mechanism, an air intake system, a conveying pipeline, a separation unit, and a discharge outlet. The bag opening mechanism is responsible for safely and effectively opening the tonne bag, ensuring that the material can be accessed without spillage or contamination. The air intake system generates the necessary airflow, either by using a vacuum pump or a pressure blower, to draw the material from the bag into the conveying pipeline.
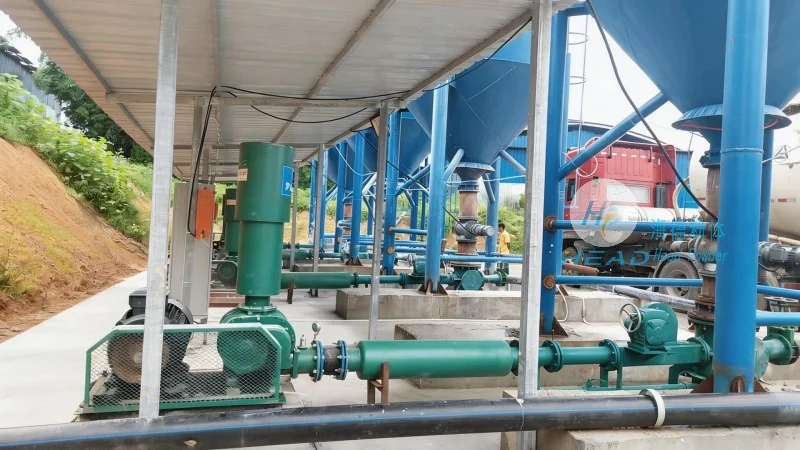
The conveying pipeline is typically made of stainless steel or other corrosion-resistant materials, designed to withstand the demands of various industrial environments. The pipeline connects the bag opening area to the separation unit, which is equipped with filters and cyclones to separate the material from the air. The separated material is then directed to the discharge outlet, where it is collected in a storage bin or processing equipment. The air, now free of particulates, is either filtered and released back into the environment or recirculated for energy efficiency.
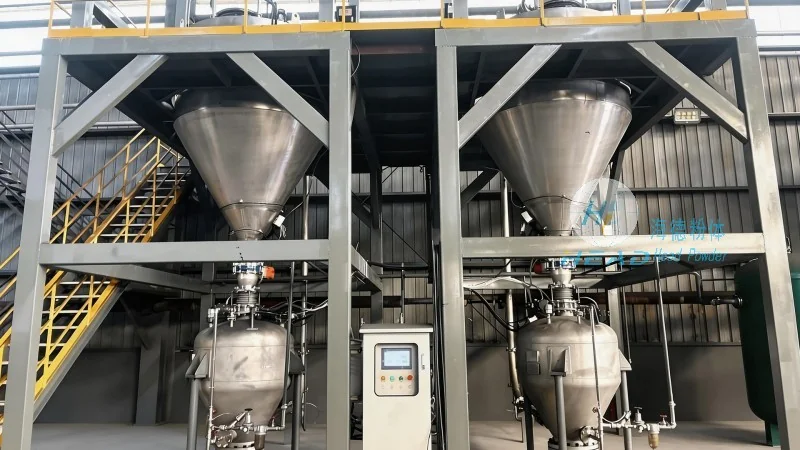
Advantages and Practical Applications
One of the key advantages of the tonne bag unloading pneumatic conveying equipment is its ability to handle a wide range of materials, from fine powders to coarse granules. The system is also highly flexible, allowing for easy integration into existing production lines or new setups. Additionally, the equipment reduces the risk of dust exposure and contamination, which is critical in industries where product purity is paramount. The automated nature of the system minimizes human intervention, leading to increased safety and reduced labor costs.
In practical applications, this equipment is commonly used in chemical plants for the transfer of raw materials and finished products, in food processing facilities for handling ingredients like flour and sugar, and in mining operations for transporting ore and minerals. The system's ability to handle large volumes efficiently makes it an ideal solution for businesses looking to streamline their material handling processes and improve overall productivity.