

Introduction to the Structure and Working Principle of the Dust-Free Bag-In Bulk Material Feeding St
For industrial applications requiring efficient and dust-free material handling, the dust-free bag-in bulk material feeding station with pneumatic conveying equipment offers a reliable solution. This equipment is designed to streamline the process of transferring bulk materials from sealed bags into processing systems, ensuring minimal contamination and enhanced operational safety.
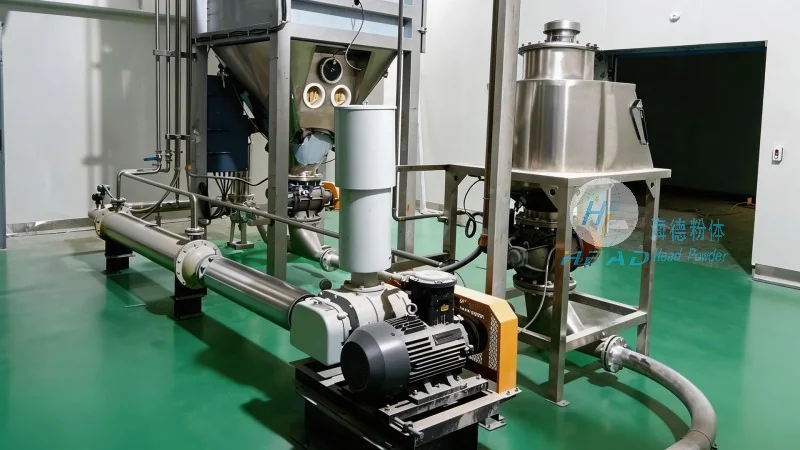
Overview of the Dust-Free Bag-In Bulk Material Feeding Station with Pneumatic Conveying
The dust-free bag-in bulk material feeding station is a specialized system engineered to handle bulk materials from bagged sources without exposing the environment to dust or contaminants. It integrates advanced pneumatic conveying technology to facilitate the transfer of materials such as powders, granules, and other bulk substances. The station typically includes a hopper, a bag opening mechanism, and a pneumatic conveying unit that works together to ensure a clean and efficient feeding process.
Working Principle of the Pneumatic Conveying System
The core of the dust-free bag-in bulk material feeding station is the pneumatic conveying system, which operates on the principle of using air to transport materials. The system can be categorized into two main types: suction and pressure systems. In a suction system, a vacuum is created to draw materials from the bag into the hopper, while a pressure system uses compressed air to push materials through the conveying lines. The chosen system depends on the material characteristics, such as density and flowability, as well as the distance and layout of the conveying path.
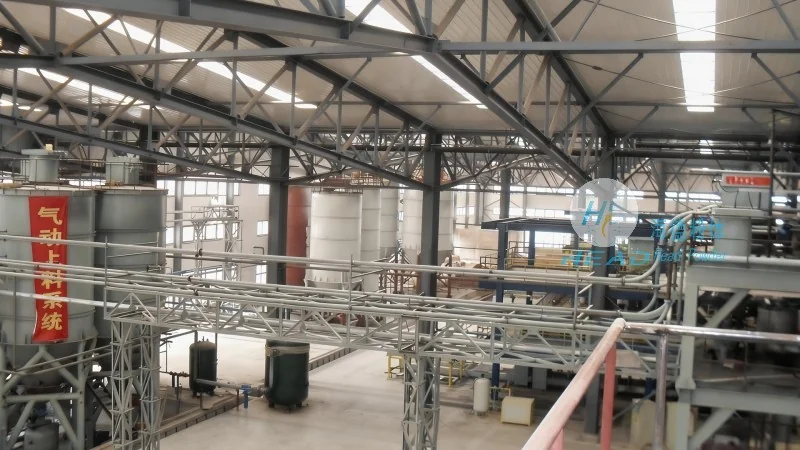
Key Components and Their Functions
The dust-free bag-in bulk material feeding station comprises several critical components, each playing a vital role in the overall operation. The primary components include:
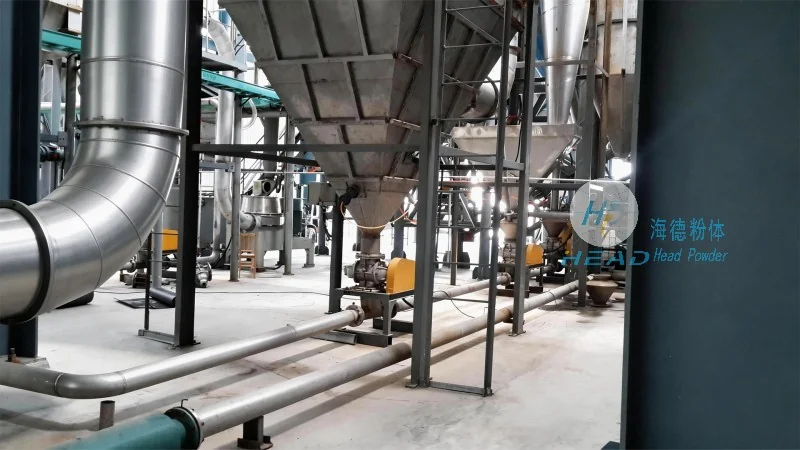
- Hopper: A container that collects the material from the bag and stores it before it is conveyed. The hopper is designed with a smooth interior to prevent material buildup and ensure easy discharge.
- Bag Opening Mechanism: This component is responsible for opening the bag and releasing the material into the hopper. It may include a cutting tool or a vacuum-assisted opening system to ensure the bag is opened without spilling the contents.
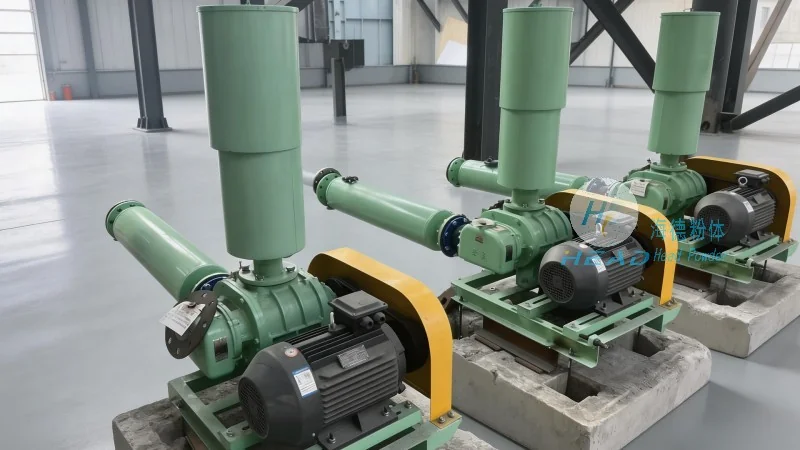
- Pneumatic Conveying Unit: This unit consists of a blower or compressor that generates the air flow necessary for conveying the material. It includes a filter to remove dust from the air, ensuring the system remains clean and compliant with environmental regulations.
- Conveying Lines and Valves: The system uses flexible or rigid pipes to transport the material from the hopper to the processing equipment. Control valves are integrated to regulate the flow rate and direction of the material, allowing for precise control over the feeding process.
Each component is carefully designed and manufactured to work in harmony, ensuring the entire system operates efficiently and reliably. The integration of these parts allows for a seamless transfer of bulk materials, minimizing downtime and maximizing productivity.
Company Information and Contact Details
The dust-free bag-in bulk material feeding station with pneumatic conveying equipment is manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading company in the field of powder handling technology. HeadPowder specializes in providing high-quality industrial equipment tailored to meet the specific needs of various industries, including pharmaceuticals, food processing, and chemical manufacturing.
HeadPowder is committed to delivering innovative solutions that enhance operational efficiency, improve product quality, and ensure compliance with industry standards. The company’s headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and a dedicated team of engineers and technicians.