

[Corn Pneumatic Conveying System Principles]
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of corn pneumatic conveying systems, dedicated to delivering high-performance solutions for the agricultural and food processing sectors. Our expertise lies in understanding the unique challenges of corn handling, from raw material reception to storage and distribution. The core of our systems is the pneumatic conveying technology, which utilizes air to transport corn particles through a sealed pipeline system. This approach not only enhances efficiency but also ensures minimal product degradation and contamination, making it ideal for applications where quality and hygiene are paramount.
Principles of Pneumatic Conveying
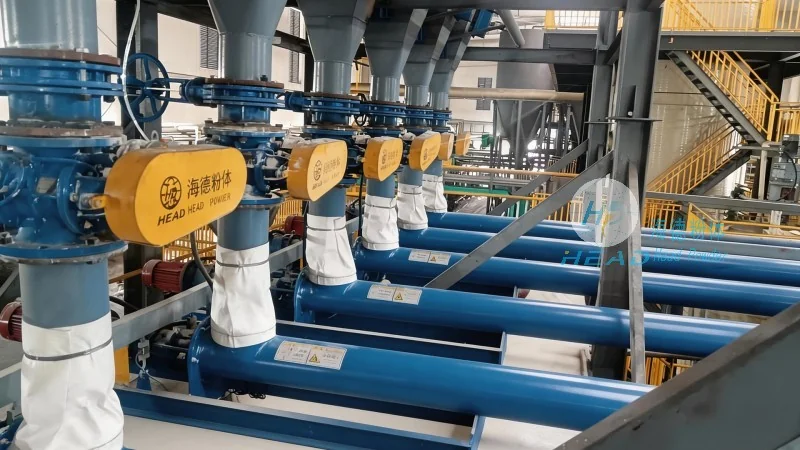
The fundamental principle of corn pneumatic conveying involves creating a pressure differential within a pipeline to move the material. There are two primary types of systems: suction (or vacuum) and pressure systems. Suction systems use a vacuum at the inlet to draw corn into the pipeline, while pressure systems use compressed air to push the material forward. Each type has its own advantages and is selected based on the specific requirements of the application, such as the distance to be covered, the volume of material, and the need for gentle handling.
Different Types of Pneumatic Conveying Systems
For corn, several system configurations are commonly used, each tailored to different operational needs. The most common is the dilute-phase system, where the corn particles are suspended in a high-velocity air stream, allowing for long-distance transport with minimal pressure drop. In contrast, dense-phase systems use lower air velocities and higher material concentrations, resulting in gentler material handling and reduced wear on equipment. Another option is the hybrid system, which combines elements of both dilute and dense-phase operation to optimize performance for specific applications. These variations ensure that our systems can be customized to meet the exact demands of each customer, whether for small-scale operations or large industrial facilities.
Key Components and Their Function
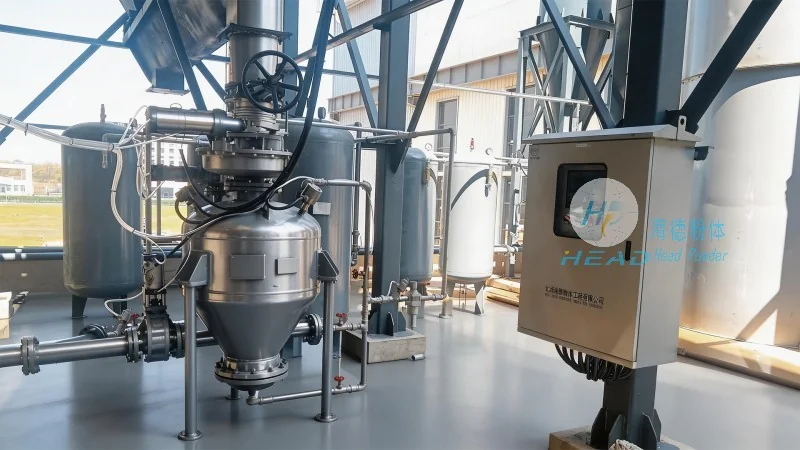
Every corn pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. The primary components include the material feed hopper, which stores and feeds the corn into the system; the air compressor or vacuum pump, which provides the necessary pressure or vacuum; the conveying pipeline, which transports the material; and the discharge hopper or silo, where the corn is collected. Additionally, control systems are integrated to regulate the flow rate, pressure, and air volume, ensuring smooth and efficient operation. These components work in harmony to create a seamless process from intake to delivery, minimizing downtime and maximizing productivity.
Advantages of Using Pneumatic Conveying for Corn
Implementing a corn pneumatic conveying system offers numerous benefits that make it a preferred choice in the industry. First, it provides a completely enclosed system, preventing dust and contamination from entering the environment or the product itself. This is particularly important for corn, which is often used in food products where purity is essential. Second, the system allows for gentle handling of the corn kernels, reducing breakage and maintaining the quality of the grain. Third, it offers high throughput capabilities, enabling large volumes of corn to be transported quickly and efficiently. Fourth, the flexibility of the system allows for easy integration with existing processing lines, and the ability to change the direction of the pipeline makes it adaptable to various facility layouts. These advantages collectively contribute to improved operational efficiency and cost savings for our clients.
Customization and Application Examples
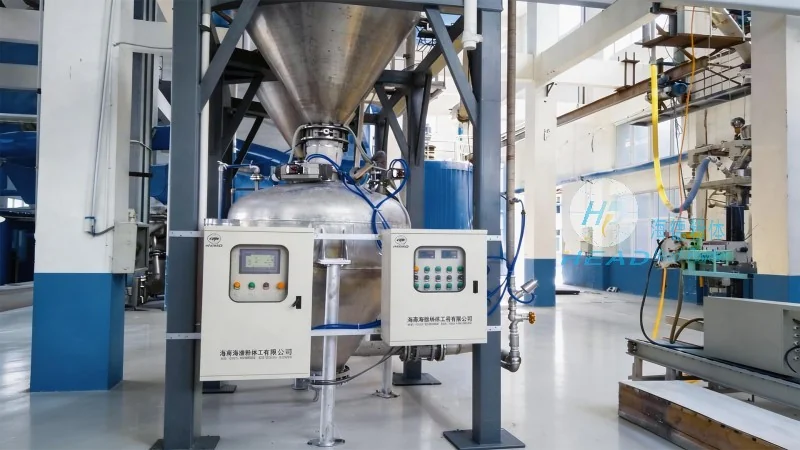
At Shandong HeadPowder Engineering Co., Ltd., we understand that every corn handling operation is unique. Therefore, we offer customized solutions tailored to the specific needs of each client. For example, in a grain elevator, our system can be designed to transport corn from the reception area to storage silos, ensuring a smooth flow of material. In a food processing plant, the system can be integrated with milling or grinding equipment, providing a continuous supply of corn for production. In agricultural settings, the system can be used to move corn from fields to storage facilities, reducing manual labor and increasing productivity. Our team of engineers works closely with clients to assess their requirements, design the optimal system, and provide installation and maintenance support, ensuring long-term reliability and performance.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative and reliable corn pneumatic conveying systems that meet the highest standards of performance and efficiency. With our expertise in the field and a focus on customer satisfaction, we continue to deliver solutions that enhance the productivity and quality of corn handling operations. Our systems are built to withstand the demands of industrial use, ensuring durability and low maintenance costs. Based in Shandong, China, we serve clients both domestically and internationally, offering comprehensive support from design to installation and beyond. Whether you are a small-scale farmer or a large industrial processor, our corn pneumatic conveying systems can help you achieve your operational goals with confidence.