

What is a Coal and Stone Powder Pneumatic Conveying System? And What Are Its Design Principles?
A coal and stone powder pneumatic conveying system is a specialized industrial equipment designed to transport fine powders, such as coal dust or stone powders, through a pipeline using air pressure. This system is widely used in various industries, including mining, power generation, and construction, due to its efficiency in handling bulk materials over long distances without the need for mechanical components like belts or buckets. The core of this system lies in its ability to move powders through a sealed pipeline, ensuring minimal environmental impact and operational safety.
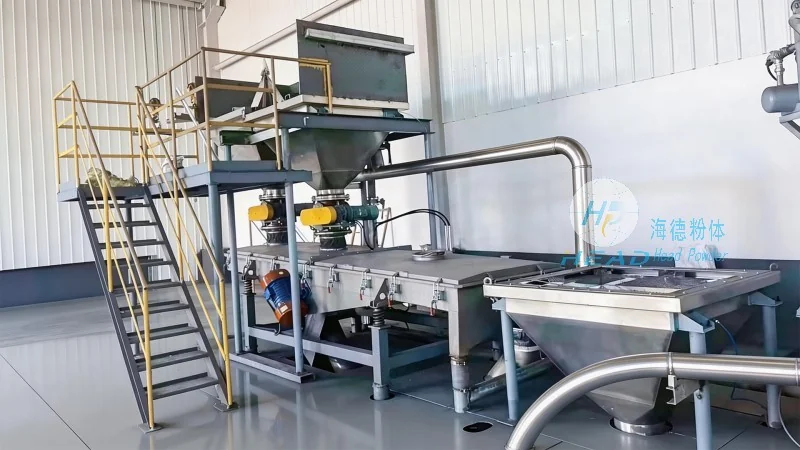
Core Components of the Pneumatic Conveying System
The coal and stone powder pneumatic conveying system consists of several key components that work in tandem to ensure smooth material transport. These components include the material hopper, which holds the powder; the air compressor or blower, which generates the necessary air pressure; the pipeline network, which carries the powder and air mixture; and the discharge unit, where the material is released. Each component plays a crucial role in maintaining the system's efficiency and reliability. For instance, the material hopper is designed to prevent material bridging and ensure consistent feeding, while the air compressor provides the required pressure to move the powder through the pipeline. The pipeline network, typically made of stainless steel or other corrosion-resistant materials, is carefully designed to minimize pressure drop and ensure the powder remains suspended in the air stream. The discharge unit, such as a rotary valve or a venturi, controls the release of the material at the destination point, preventing backflow and ensuring a controlled discharge process.
Design Principles and Operational Mechanisms
The design principles of a coal and stone powder pneumatic conveying system are centered around the principles of fluidization and suspension. The system operates by creating a high-velocity air stream that lifts and transports the powder particles through the pipeline. The key design considerations include the air velocity, which must be sufficient to keep the powder particles suspended without causing excessive wear on the pipeline or components. The system's design also takes into account the particle size and density of the material, as these factors influence the required air pressure and velocity. For example, finer powders may require higher air velocities to maintain suspension, while larger particles may need a different approach to ensure efficient transport. Additionally, the system's design incorporates features to minimize pressure losses, such as smooth pipeline surfaces and appropriate bends and fittings, to ensure the system operates efficiently over long distances. The use of a venturi or other pressure-reducing devices at the discharge point helps to control the flow rate and prevent material buildup, further enhancing the system's performance.
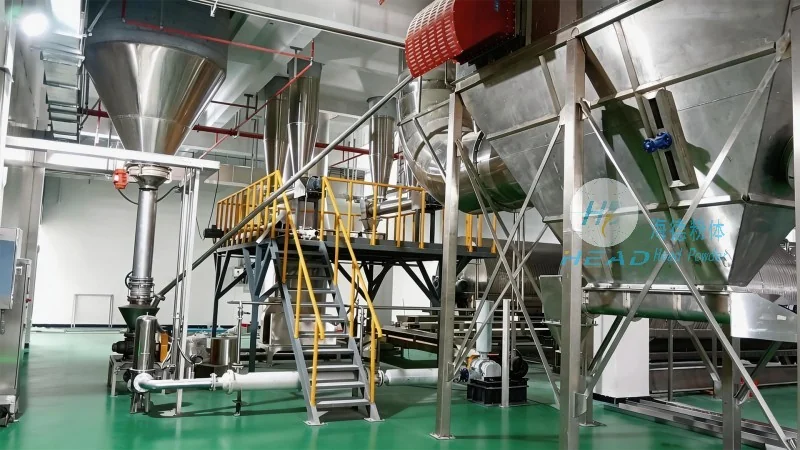
Advantages of Using a Pneumatic Conveying System for Coal and Stone Powders
Implementing a coal and stone powder pneumatic conveying system offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in material handling costs, as the system eliminates the need for manual labor or mechanical components like conveyor belts. This not only reduces operational expenses but also minimizes the risk of material spillage and environmental contamination. Another advantage is the improved safety and hygiene, as the system operates in a sealed environment, preventing dust emissions and ensuring a cleaner working environment. The system also allows for flexible and scalable operations, as the pipeline network can be easily expanded or modified to accommodate changes in production requirements. Furthermore, the system's ability to transport materials over long distances without the need for intermediate storage points enhances overall operational efficiency and reduces downtime. These advantages make the pneumatic conveying system an ideal choice for industries dealing with fine powders, where efficiency, safety, and cost-effectiveness are critical.
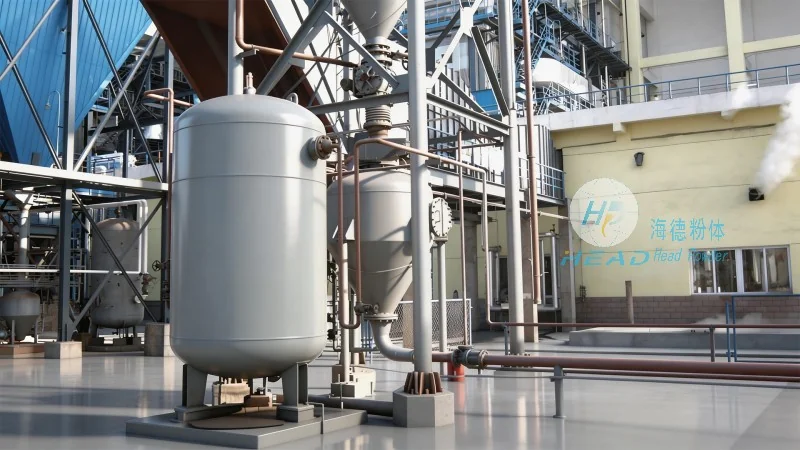
Applications in Different Industries
The coal and stone powder pneumatic conveying system finds applications in a wide range of industries, each benefiting from its unique capabilities. In the power generation industry, this system is used to transport coal from storage silos to boilers, ensuring a continuous and efficient fuel supply. The mining industry utilizes the system to transport ore powders from processing plants to storage facilities, facilitating the smooth flow of materials. In the construction industry, the system is employed to transport stone powders for concrete production, providing a consistent and high-quality material input. Additionally, the system is used in the chemical and pharmaceutical industries to transport fine powders, where maintaining product purity and preventing contamination is paramount. Each application leverages the system's ability to handle bulk materials efficiently and safely, contributing to improved productivity and operational performance.
Conclusion and Company Information
Coal and stone powder pneumatic conveying systems are essential equipment for industries dealing with fine powders, offering efficient, safe, and cost-effective material transport solutions. The design principles and operational mechanisms of these systems ensure reliable performance, while the various components work together to maintain optimal operation. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and customer satisfaction, HeadPowder delivers solutions that enhance operational efficiency and reduce costs for businesses across various industries. Based in Shandong, China, HeadPowder leverages its expertise and experience to provide reliable and durable pneumatic conveying systems that meet the highest industry standards. Whether for coal or stone powders, the company's systems are designed to deliver consistent performance and long-term value, supporting the growth and success of its clients.