

What is a Tonne Bag Quantitative Feeding Pneumatic Conveying Equipment? And What Are Its Design Prin
For industries that require precise material handling and efficient bulk material transfer, the tonne bag quantitative feeding pneumatic conveying equipment has emerged as a critical solution. This equipment is specifically designed to handle large volumes of bulk materials, such as powders, granules, and other dry substances, from tonne bags with high accuracy and reliability. Understanding the functionality and design principles of this equipment is essential for optimizing material processing workflows and ensuring operational efficiency.
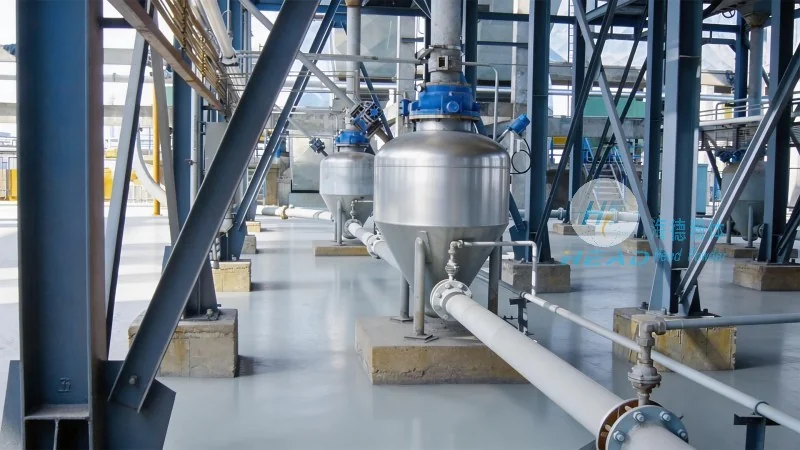
Key Components and Working Principle
The tonne bag quantitative feeding pneumatic conveying equipment typically consists of several key components that work in harmony to achieve precise material transfer. The primary components include a hopper for receiving material from the tonne bag, a rotary valve or feeder for controlling the flow rate, a pneumatic conveying system with a blower or compressor to generate the air flow, and a discharge outlet for delivering the material to the next processing stage. The working principle involves the following steps: First, the tonne bag is positioned above the hopper, and the material is released into the hopper. Then, the rotary valve or feeder regulates the material flow into the pneumatic conveying line. The blower or compressor then generates a high-pressure air stream that carries the material particles through the pipeline to the discharge point. The design ensures that the material is conveyed in a controlled manner, minimizing segregation and ensuring consistent flow rates.
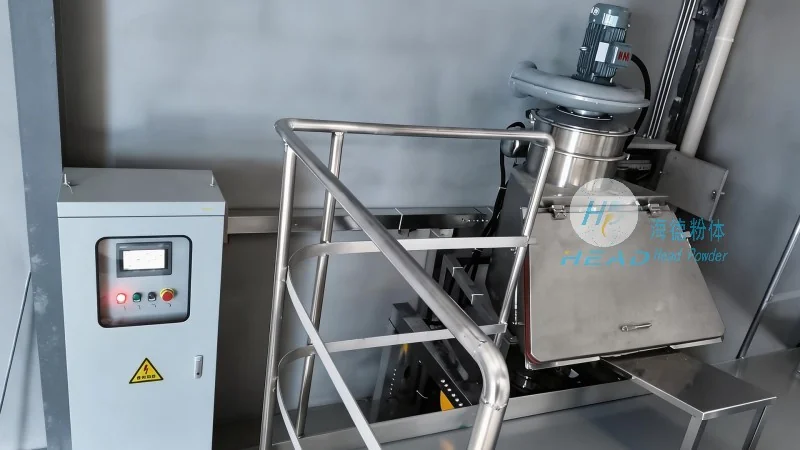
Design Principles for Precision and Efficiency
The design of tonne bag quantitative feeding pneumatic conveying equipment is centered on several key principles to ensure high accuracy and operational efficiency. One of the primary principles is the use of a precise feeding mechanism, such as a rotary valve or a volumetric feeder, which allows for accurate control of the material flow rate. This is crucial for applications where exact dosing is required, such as in pharmaceuticals, food processing, or chemical manufacturing. Another important principle is the integration of a robust pneumatic conveying system with appropriate air flow management. The system must be capable of handling the specific characteristics of the material, including particle size, density, and moisture content, to prevent blockages and ensure smooth operation. Additionally, the equipment is designed with features like air filtration and separation systems to maintain material purity and prevent contamination. The overall design emphasizes durability, low maintenance, and ease of cleaning, which are essential for industries with strict hygiene and quality control requirements.
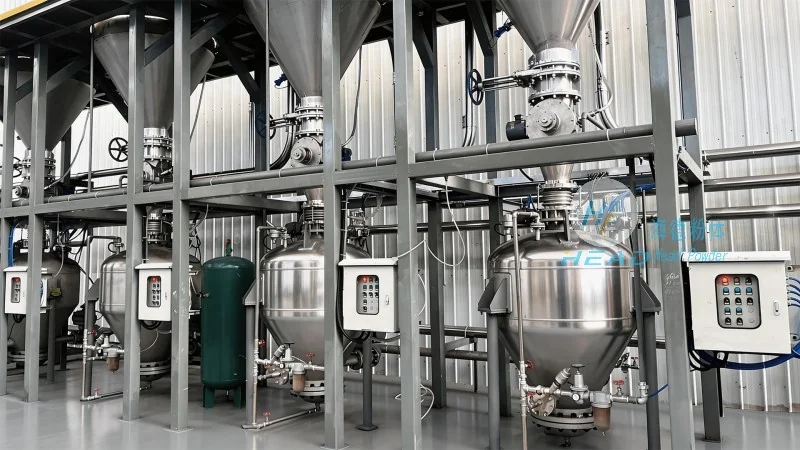
Applications and Benefits in Industrial Settings
Tonne bag quantitative feeding pneumatic conveying equipment is widely used in various industrial sectors due to its versatility and efficiency. In the pharmaceutical industry, it is used for handling active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the correct dosage is delivered to the next stage of production. In the food processing industry, it is employed for conveying ingredients like flour, sugar, and spices, maintaining product quality and consistency. The chemical industry also benefits from this equipment for handling raw materials and intermediates, particularly in processes that require controlled dosing and minimal contamination. The primary benefits of using this equipment include improved material handling accuracy, reduced labor costs, increased production throughput, and enhanced safety by minimizing manual handling of bulk materials. Additionally, the equipment helps in reducing material waste and improving overall operational efficiency, making it a valuable asset for modern industrial operations.
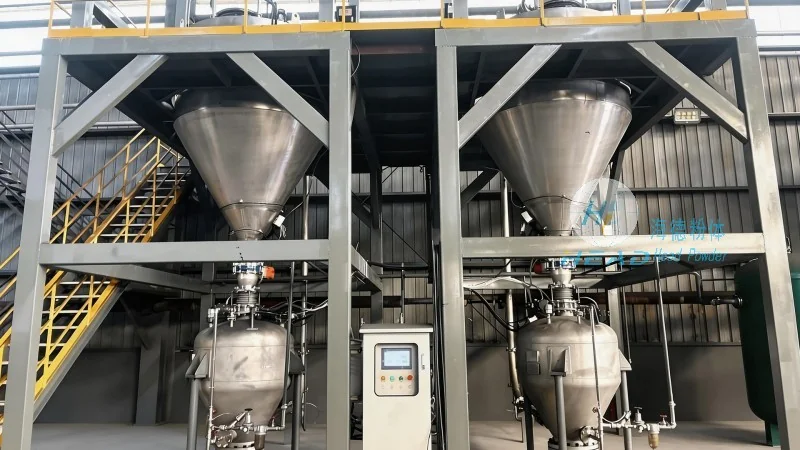
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling equipment. With a strong focus on innovation and quality, HeadPowder specializes in designing and producing tonne bag quantitative feeding pneumatic conveying equipment tailored to the specific needs of various industries. The company is committed to providing reliable and efficient solutions that enhance operational performance and meet the highest standards of quality and safety. HeadPowder's products are engineered with precision and durability in mind, ensuring long-term performance and minimal maintenance requirements. The company's team of experts works closely with clients to understand their unique requirements and develop customized solutions that optimize material handling processes. HeadPowder is dedicated to delivering exceptional customer service and support, ensuring that clients receive the best possible solutions for their material handling needs.