

What is a Coke Pneumatic Conveyor? What is its Design Principle?
Understanding the technology behind coke pneumatic conveyors is essential for industries that rely on efficient material handling. This article explores the fundamental aspects of coke pneumatic conveyors, including their design principles and operational capabilities, as presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
Introduction to Coke Pneumatic Conveyors
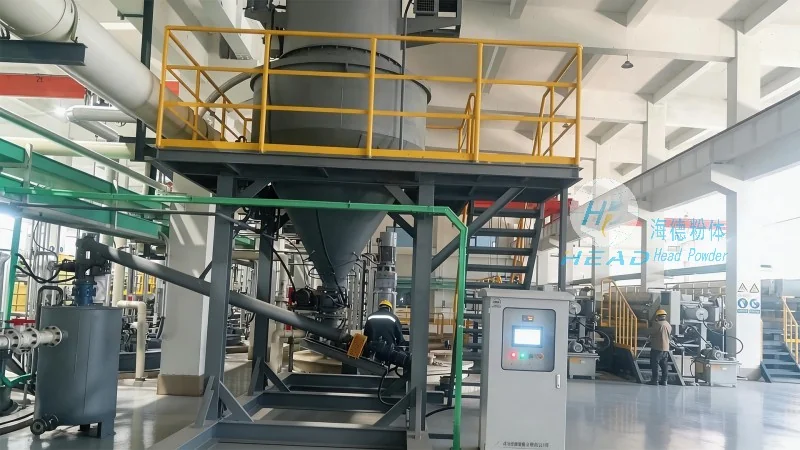
A coke pneumatic conveyor is a specialized system designed to transport coke, a byproduct of the coking process used in the steel industry, from one location to another using air pressure or suction. These systems are critical in modern industrial settings, where the efficient movement of bulk materials is paramount to maintaining production efficiency and safety standards. The technology behind these conveyors combines mechanical engineering with pneumatic principles to create a reliable and versatile material handling solution.
Key Components of a Coke Pneumatic Conveyor
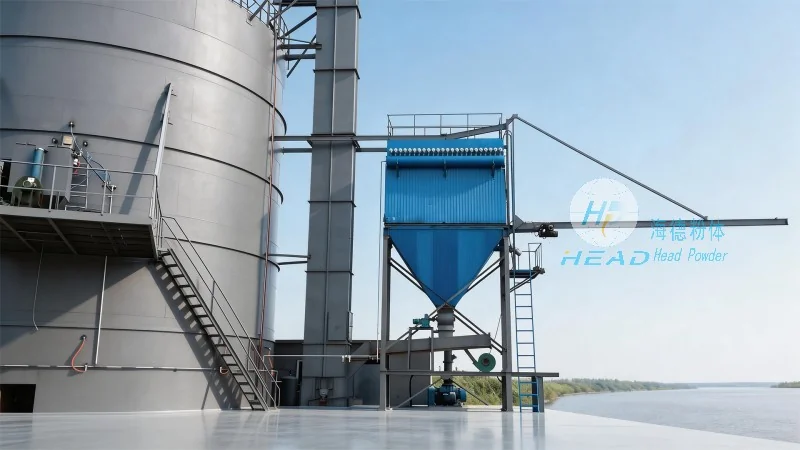
The design of a coke pneumatic conveyor involves several key components that work in tandem to ensure effective material transport. These components include the hopper or feed hopper, which collects and stores the coke; the conveyor line, which can be either positive pressure or negative pressure based on the system design; and the discharge unit, which delivers the coke to its final destination. Additionally, the system may incorporate filters, silencers, and pressure regulators to manage air flow and maintain operational efficiency. Each component is engineered to withstand the abrasive nature of coke and the high pressures involved in the conveying process.
Design Principles and Operational Mechanisms
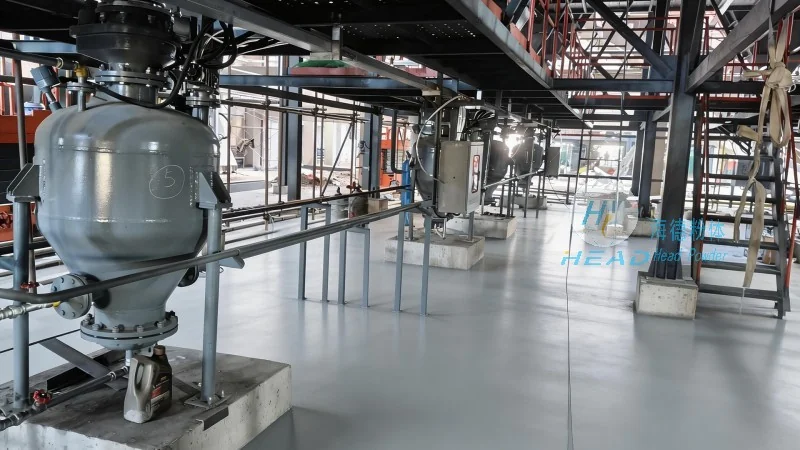
The core design principle of a coke pneumatic conveyor is to use air as the medium for transporting solid particles. In positive pressure systems, compressed air is introduced into the conveyor line, pushing the coke forward through the pipeline. In contrast, negative pressure systems create a vacuum that draws the coke into the line. The choice between these two mechanisms depends on factors such as the distance to be covered, the material's characteristics, and the required flow rate. The design also considers the velocity of the air and the particle size distribution to prevent blockages and ensure consistent performance. Engineers at Shandong HeadPowder Engineering Co., Ltd. specialize in tailoring these principles to meet specific customer requirements, ensuring optimal performance and reliability.
Advantages of Using Coke Pneumatic Conveyors
Implementing a coke pneumatic conveyor offers several advantages over traditional material handling methods. These systems are highly flexible, allowing for vertical, horizontal, or inclined transport without the need for complex machinery or extensive infrastructure modifications. They also provide a dust-free environment, which enhances workplace safety and reduces the risk of fire hazards associated with coke dust. Furthermore, the enclosed design minimizes material loss and contamination, preserving the quality of the coke. The energy efficiency of these systems, particularly when optimized for low air consumption, contributes to cost savings and environmental sustainability. Shandong HeadPowder Engineering Co., Ltd. emphasizes these benefits in their product offerings, providing customized solutions that address the unique needs of each client.
Applications and Industry Impact
Coke pneumatic conveyors are widely used in the steel industry, where they play a crucial role in the supply chain from coke production to its use in blast furnaces. The systems are also applicable in other industries that handle bulk solid materials, such as chemical processing and mining. The reliability and efficiency of these conveyors contribute to improved production throughput and reduced downtime, which are critical for maintaining competitive advantages in today's market. Shandong HeadPowder Engineering Co., Ltd. has extensive experience in designing and manufacturing these systems, serving clients across China and beyond with tailored solutions that enhance operational performance.
Conclusion and Company Overview
In summary, coke pneumatic conveyors are sophisticated systems that leverage pneumatic technology to efficiently transport coke, a vital material in the steel industry. The design principles, including the choice of positive or negative pressure, component selection, and operational parameters, are carefully engineered to ensure optimal performance. The advantages of these systems, such as flexibility, dust control, and energy efficiency, make them an essential part of modern material handling strategies. Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a trusted provider of these systems, offering customized solutions that meet the specific needs of industrial clients. By understanding the technology and benefits of coke pneumatic conveyors, industries can enhance their operational efficiency and maintain a competitive edge in the market.