

What is a Refractory Material Pneumatic Conveying System? What Are Its Design Principles?
Refractory material pneumatic conveying systems are specialized equipment designed to transport refractory materials, such as powders and granules, through a pipeline using air or gas as the conveying medium. These systems are widely used in various industrial sectors, including the refractory industry, ceramics, and chemical processing, where efficient and safe material handling is crucial. The design of such systems involves several key principles that ensure optimal performance, reliability, and efficiency.
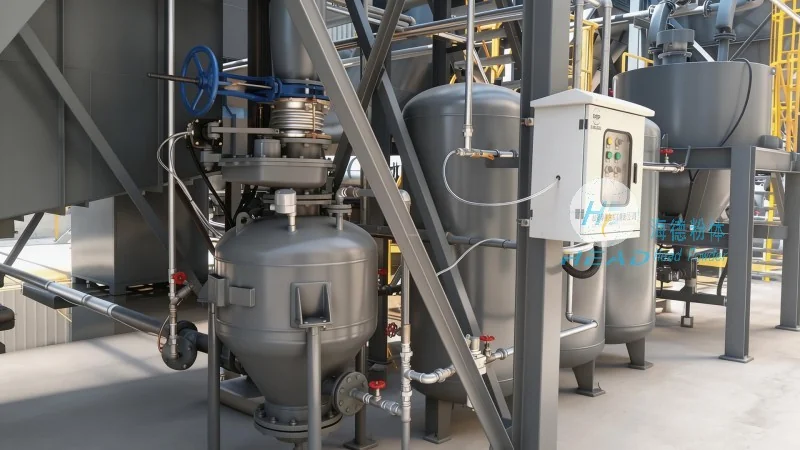
Understanding Refractory Material Pneumatic Conveying Systems
At the core of a refractory material pneumatic conveying system is the ability to transport abrasive and often temperature-sensitive materials without causing degradation or contamination. The system typically consists of a hopper for material storage, a conveying line, a blower or compressor to generate the air flow, and a receiver for the discharged material. The choice of conveying method—such as dilute phase or dense phase—depends on the material characteristics, required distance, and desired flow rate.
Key Design Principles for Efficient Operation
The design principles of a refractory material pneumatic conveying system focus on several critical aspects to ensure smooth and reliable operation. First, the system must be constructed from materials that can withstand the abrasive nature of refractory powders, often using stainless steel or specialized alloys to prevent wear and corrosion. Second, the air flow rate and pressure must be precisely controlled to maintain consistent material transport without causing blockages or excessive energy consumption. This involves careful selection of the blower or compressor capacity, as well as the diameter and length of the conveying line.
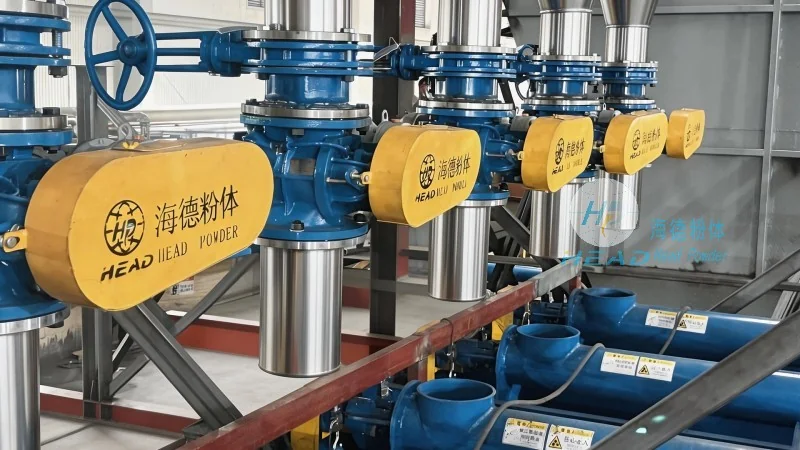
Third, the system incorporates features to handle variations in material properties, such as moisture content or particle size distribution. For example, some systems use a pre-drying or conditioning step to improve material flowability, while others employ pulse or rotary valves to regulate the material discharge and prevent clogging. Additionally, the design considers the need for dust collection and filtration to maintain air quality and comply with environmental regulations, which is particularly important when handling fine refractory powders.
Applications and Benefits in Industrial Settings
Refractory material pneumatic conveying systems offer significant advantages in industrial applications. They enable the safe and efficient transfer of materials over long distances, often in environments where traditional mechanical conveyors may be impractical due to space constraints or the need to avoid contamination. The systems are also capable of handling materials with high temperatures or aggressive chemical properties, making them suitable for high-temperature processes like furnace loading or kiln operation.
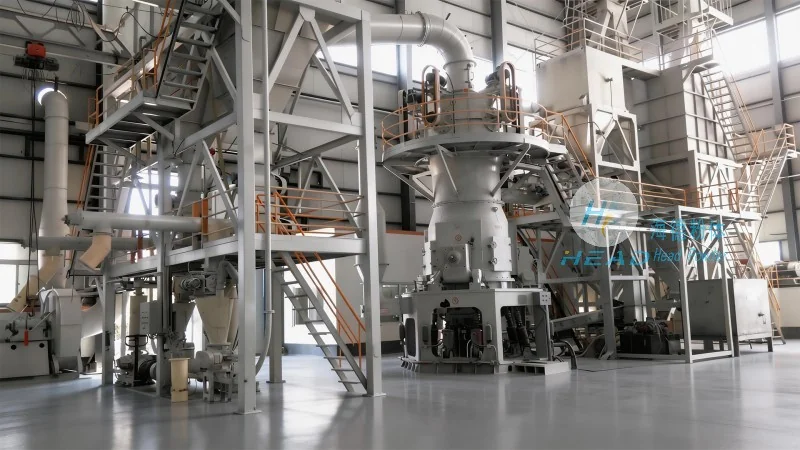
Furthermore, these systems contribute to improved operational efficiency by reducing downtime and maintenance costs. By minimizing material handling errors and ensuring consistent material flow, they help maintain production continuity and quality control. The compact design of many pneumatic conveying systems also allows for integration into existing industrial facilities without requiring extensive modifications.
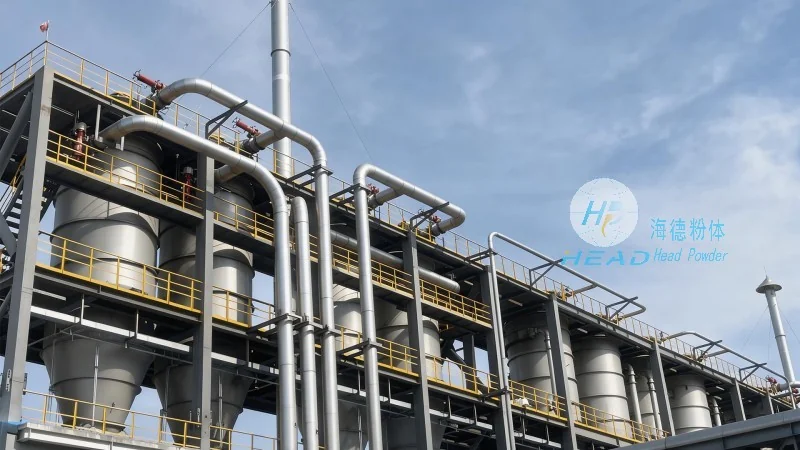
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized industrial equipment, including refractory material pneumatic conveying systems. With a focus on innovation and quality, HeadPowder has established itself as a trusted partner in the refractory and related industries. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing technologies and a team of experienced engineers to develop and produce high-performance conveying solutions tailored to customer needs.
HeadPowder's commitment to customer satisfaction and product excellence is reflected in its comprehensive product line and after-sales support services. The company works closely with clients to understand their specific operational requirements and provides customized solutions that enhance productivity and reduce operational costs. By adhering to strict quality standards and adhering to industry best practices, HeadPowder ensures that its pneumatic conveying systems meet the highest performance and reliability expectations.