

What is a Baking Soda Pneumatic Conveying System Equipment? What Are Its Design Principles?
Baking soda, also known as sodium bicarbonate, is a common chemical used in various industries for its buffering properties and neutralizing capabilities. When it comes to handling this material efficiently, especially in bulk, a specialized system is required. The Baking Soda Pneumatic Conveying System Equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered to address the unique challenges of transporting this fine powder while ensuring minimal loss and optimal performance. This equipment is designed to integrate seamlessly into production lines, offering a reliable solution for industries that rely on consistent and safe delivery of baking soda.
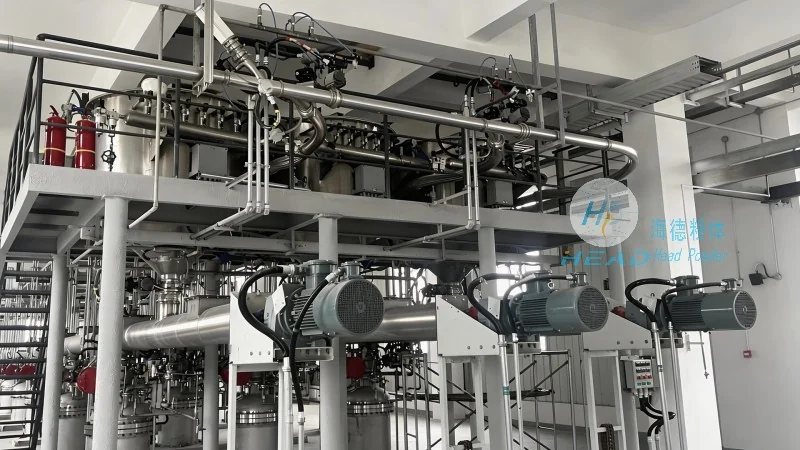
Understanding the Core Design Principles
The design of a pneumatic conveying system for baking soda is built on several key principles that ensure efficiency, safety, and durability. First, the system must handle the physical properties of the material, such as its particle size, density, and flow characteristics. Baking soda is typically a fine powder, which can lead to issues like caking or blockages if not managed properly. The system incorporates features like aeration and pressure control to maintain a consistent flow. Second, the equipment must adhere to safety standards, as pneumatic systems can pose risks related to pressure and material handling. The design includes pressure relief valves, explosion-proof components, and proper ventilation to mitigate these risks. Third, the system is built for scalability and adaptability, allowing it to be customized for different production volumes and operational needs. The engineering team at Shandong HeadPowder Engineering Co., Ltd. leverages advanced technology and industry expertise to develop systems that meet these criteria, ensuring that each component is optimized for the specific requirements of baking soda transportation.
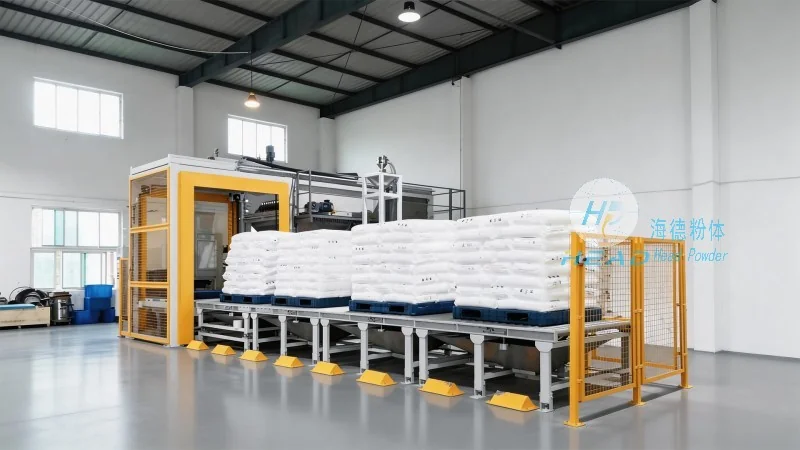
Key Components and Their Functions
The Baking Soda Pneumatic Conveying System Equipment consists of several critical components, each playing a vital role in the overall operation. The hopper or silo is the primary storage unit, designed to hold the baking soda in a way that prevents agglomeration and allows for smooth discharge. The feeder, often a rotary valve or a screw feeder, regulates the flow of the material into the conveying line, ensuring a consistent feed rate. The conveying line itself is typically made of stainless steel or other corrosion-resistant materials, suitable for handling the chemical properties of baking soda. The air compressor or blower provides the necessary pressure to move the material through the system, with adjustable settings to control the flow rate. The control panel allows operators to monitor and adjust the system parameters in real-time, enhancing operational efficiency. Each component is carefully selected and integrated to work in harmony, minimizing downtime and maximizing productivity. The engineering team at Shandong HeadPowder Engineering Co., Ltd. ensures that all parts are compatible and durable, reducing the need for frequent maintenance and repairs.
Advantages of Using a Pneumatic Conveying System for Baking Soda
Implementing a pneumatic conveying system for baking soda offers numerous advantages over traditional methods like bucket elevators or belt conveyors. One of the most significant benefits is the reduction in material loss and contamination. Pneumatic systems can transport the material with minimal spillage, as the material is enclosed within the conveying line. This is particularly important for baking soda, which is often used in food and pharmaceutical applications where purity is paramount. Another advantage is the ability to handle the material in a closed system, preventing dust emissions and maintaining a clean working environment. This not only improves safety for operators but also complies with environmental regulations. Additionally, pneumatic conveying systems are more flexible in terms of layout, allowing for vertical, horizontal, or even inclined transport paths. This flexibility enables the system to be integrated into existing production facilities without major structural changes. The system also offers better control over the flow rate, which is crucial for maintaining consistent product quality. By using a pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd., industries can achieve higher efficiency, lower operational costs, and improved product quality.
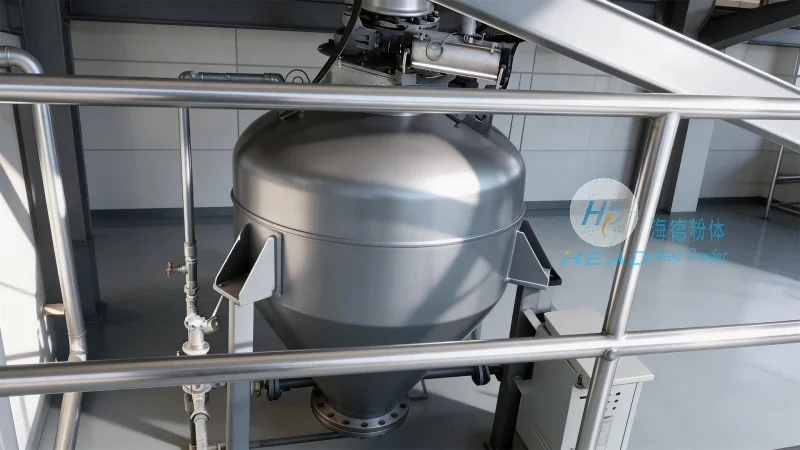
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd. understands that each client has unique operational requirements, which is why their Baking Soda Pneumatic Conveying System Equipment is highly customizable. The company offers tailored solutions based on the specific needs of the client, including the capacity of the system, the type of material handling, and the desired layout. Whether a client needs a small-scale system for a laboratory or a large-scale system for an industrial plant, the engineering team can design a solution that meets their exact specifications. The system can be scaled up or down to accommodate changes in production volume, ensuring that the investment remains efficient and cost-effective over time. The company also provides after-sales support, including maintenance services and technical assistance, to ensure that the system operates at peak performance throughout its lifespan. This commitment to customization and scalability makes the Baking Soda Pneumatic Conveying System Equipment a reliable choice for businesses looking to optimize their material handling processes.