

What is an Automatic Weighing Powder Conveying System? What Are Its Design Principles?
An automatic weighing powder conveying system is a sophisticated industrial solution designed to handle the precise and efficient transportation of bulk powders while simultaneously measuring their weight. This technology integrates advanced sensors, control systems, and material handling mechanisms to ensure accurate dosing and consistent flow, making it indispensable in various industries such as pharmaceuticals, food processing, and chemical manufacturing.
Understanding the Core Components and Functionality
The system typically comprises several key components that work in tandem to achieve its objectives. At its heart is a high-precision load cell or weighing sensor, which provides real-time data on the weight of the material being conveyed. This sensor is often integrated with a conveyor system, such as a screw conveyor, pneumatic conveyor, or belt conveyor, depending on the specific application and material characteristics. The conveyor transports the powder from a storage hopper or silo to the processing unit, while the weighing system continuously monitors the mass flow rate.
Control logic, usually managed by a programmable logic controller (PLC) or a dedicated industrial computer, processes the weight data from the sensor. This control unit adjusts the conveyor speed or the flow rate of the powder to maintain the desired weight output. For instance, if the target weight is 100 kg, the system will modulate the conveyor speed until the measured weight reaches the setpoint. This closed-loop control ensures high accuracy and repeatability, minimizing variations in the final product.
The Design Principles Behind the System
The design principles of an automatic weighing powder conveying system are centered on precision, reliability, and adaptability. Engineers must consider several factors to optimize the system for different powder types and operational requirements. One critical principle is the selection of appropriate conveying equipment based on the powder's flowability and particle size. For cohesive or low-flowability powders, a screw conveyor with a variable speed drive might be preferred, as it can handle sticky materials without blockages. Conversely, free-flowing powders may benefit from a pneumatic conveyor, which uses air pressure to move the material, reducing friction and wear.
Another key design principle is the integration of multiple weighing points or stages. In some applications, the system may include a primary weigh hopper that accumulates the powder and a secondary discharge mechanism that releases it in controlled batches. This multi-stage approach allows for higher throughput while maintaining accuracy. The control system must coordinate the timing of each stage to prevent overfilling or underfilling, ensuring that the final product meets strict quality standards.
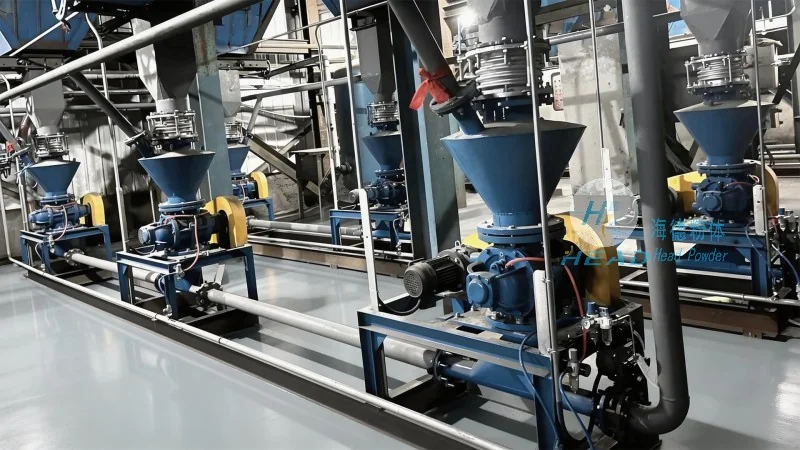
Material handling and safety are also paramount in the design. The system must be constructed from materials compatible with the conveyed powders, such as stainless steel or food-grade plastics, to prevent contamination. Additionally, safety features like emergency stop buttons, overload protection, and dust suppression systems are incorporated to protect operators and the environment. The design also considers maintenance accessibility, with easy-to-remove components and clear labeling for troubleshooting.
About HeadPowder: A Leader in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a renowned manufacturer specializing in advanced powder handling systems. With headquarters in Shandong, China, the company has built a strong reputation for delivering high-quality, reliable equipment tailored to the needs of various industries. HeadPowder's team of engineers and technicians leverages years of experience to design and develop systems that meet stringent international standards, ensuring durability and performance in demanding environments.
The company's commitment to innovation is evident in its continuous investment in research and development. HeadPowder stays at the forefront of technological advancements, incorporating the latest sensors, control technologies, and materials in its products. This dedication to excellence has enabled the company to serve a diverse clientele, from small-scale manufacturers to large-scale industrial operations. By focusing on customer needs and providing comprehensive support, HeadPowder has established itself as a trusted partner in the powder handling industry.
HeadPowder's products, including automatic weighing powder conveying systems, are designed to enhance operational efficiency, reduce waste, and improve product quality. The company's expertise in material science and process engineering allows it to address the unique challenges faced by each client, whether it's handling sensitive pharmaceutical powders or abrasive chemical materials. With a strong emphasis on quality control and customer satisfaction, HeadPowder continues to be a leader in providing solutions that drive industrial productivity and success.