

What is a Baking Soda Powder Conveying System? What Are Its Design Principles?
Baking soda, also known as sodium bicarbonate, is a widely used chemical in various industries, including food processing, pharmaceuticals, and manufacturing. Efficient and reliable transportation of this powder is crucial for maintaining product quality and operational efficiency. This article explores the concept of a baking soda powder conveying system and delves into its fundamental design principles, highlighting the key components and operational mechanisms that ensure effective powder handling.
Understanding the Core Components of a Baking Soda Powder Conveying System
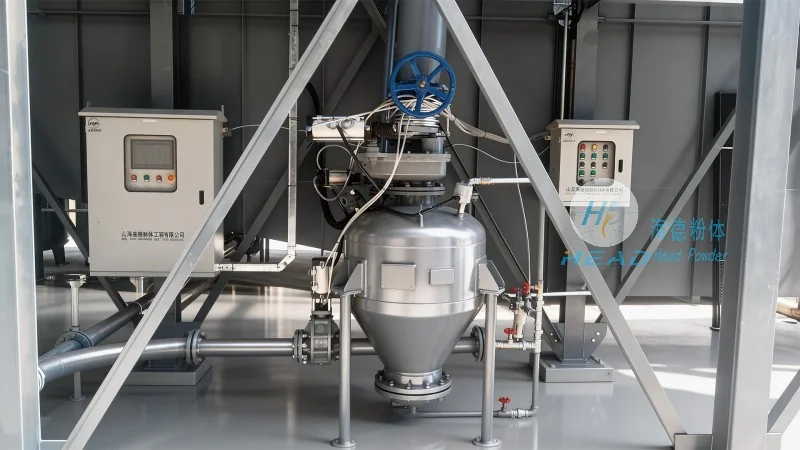
The design of a baking soda powder conveying system is built around several critical components that work in tandem to move the material from one location to another. The primary components typically include a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw or pneumatic system), and a discharge outlet for the final delivery. Each component plays a vital role in ensuring the system operates smoothly and efficiently. The hopper is designed to hold a sufficient quantity of baking soda, allowing for consistent feeding without interruptions. The feeder, often a rotary valve or a screw feeder, regulates the flow of powder into the conveyor, preventing overloading and maintaining a steady supply. The conveyor mechanism, which can be either mechanical (like a screw conveyor) or pneumatic (using air pressure to transport the powder), moves the material through the system. Finally, the discharge outlet delivers the baking soda to the intended destination, such as a processing line or storage container.
Design Principles for Optimal Performance
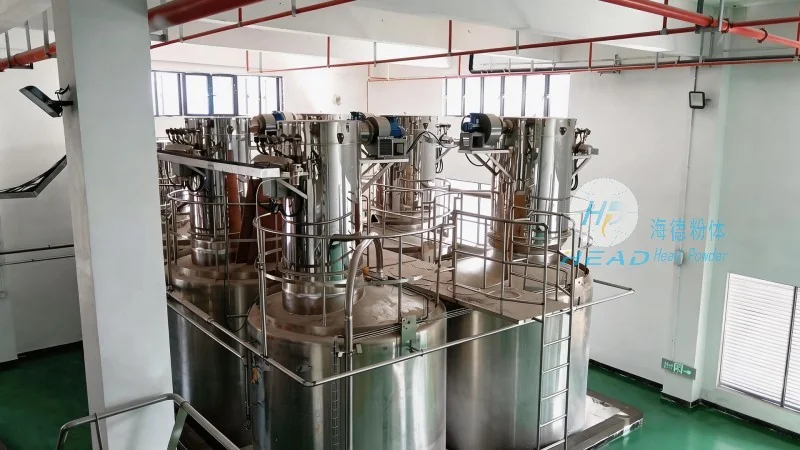
The design principles of a baking soda powder conveying system are centered on ensuring minimal product degradation, preventing caking or bridging, and maintaining high operational efficiency. One of the key design considerations is the prevention of material degradation, which can occur due to friction, impact, or exposure to air. To address this, the system is often constructed with materials that are non-reactive and smooth, reducing the risk of particle damage. Additionally, the design incorporates features to prevent caking or bridging, which can block the conveyor and disrupt the flow. This includes using appropriate hopper angles, vibration systems, or air knives to keep the powder in a free-flowing state. Another critical principle is the control of air flow and pressure in pneumatic systems, as improper air management can lead to uneven material distribution or loss of product. The system must also be designed for easy maintenance and cleaning, as baking soda can leave residue that may affect performance over time. By adhering to these design principles, the conveying system ensures consistent and reliable operation, minimizing downtime and maximizing productivity.
HeadPowder's Expertise in Baking Soda Powder Conveying Solutions
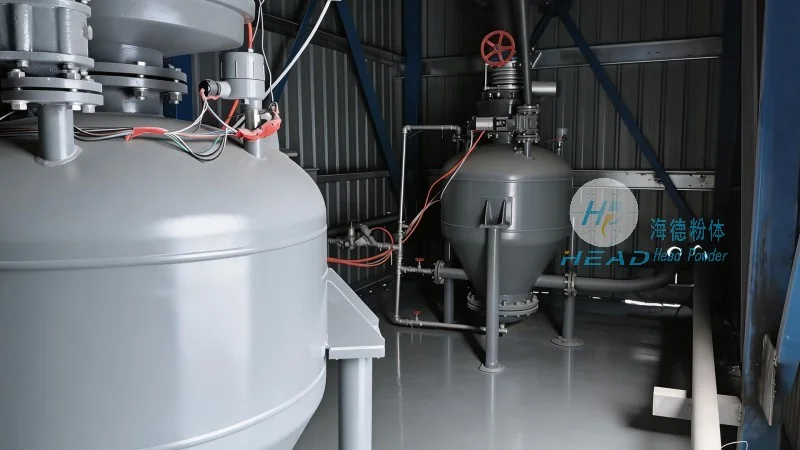
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of advanced powder conveying systems tailored to the unique needs of baking soda and other similar materials. With years of experience in the industry, HeadPowder has developed a comprehensive range of solutions that address the specific challenges of handling fine powders like baking soda. The company's expertise lies in understanding the material properties of baking soda, such as its flow characteristics and potential for caking, and translating this knowledge into effective system designs. HeadPowder's systems are engineered to provide high accuracy in flow control, ensuring that the correct amount of powder is delivered to the next stage of production. The company also focuses on durability and longevity, using high-quality materials and robust construction to withstand the demands of continuous operation. Furthermore, HeadPowder offers customized solutions, allowing clients to tailor the system to their specific operational requirements, whether it's for small-scale or large-scale production. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking reliable powder conveying solutions.