

What is an Industrial Alkali Powder Handling System? And What Are Its Design Principles?
Industrial alkali powder handling systems are critical components in various industrial processes, particularly in sectors dealing with caustic substances like sodium hydroxide or potassium hydroxide. These systems are engineered to safely and efficiently transport, store, and manage alkali powders, ensuring operational safety and product integrity. Understanding the design principles behind such systems is essential for industries that rely on these materials for manufacturing, chemical processing, or other applications.
HeadPowder, a leading provider of specialized engineering solutions, is dedicated to delivering high-quality industrial equipment tailored to the unique needs of alkali powder handling. With a strong presence in China, specifically in Shandong, the company leverages years of expertise to develop systems that meet stringent safety and performance standards.
Understanding the Core Components of Alkali Powder Handling Systems
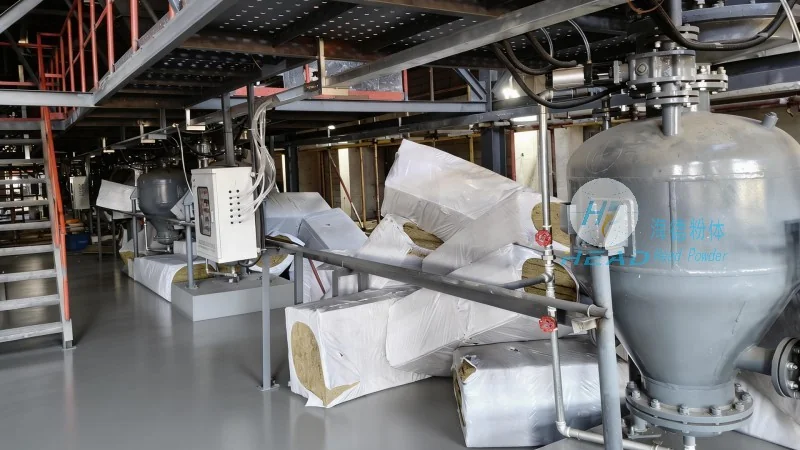
At the heart of any industrial alkali powder handling system are several key components that work in tandem to ensure smooth operation. The primary elements include storage silos or hoppers, which are designed to hold large quantities of alkali powder while minimizing exposure to air and moisture. These containers are typically made from corrosion-resistant materials, such as stainless steel or specialized alloys, to withstand the chemical properties of the powders.
From the storage silos, the powder is transferred to the processing or packaging areas via a network of conveying equipment. Common types of conveyors used in alkali powder handling include pneumatic conveying systems, screw conveyors, and bucket elevators. Pneumatic systems use air pressure to move powder through pipelines, while screw and bucket elevators rely on mechanical motion to transport material vertically or horizontally. Each type of conveyor has its advantages and is selected based on factors like the powder's bulk density, flowability, and the system's layout.
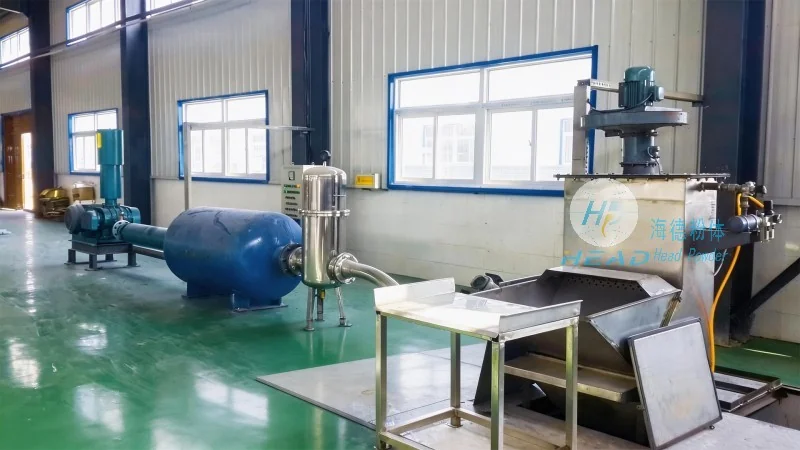
Another critical component is the feeding and metering equipment. These devices control the flow rate of the alkali powder from the storage silo to the processing line, ensuring precise dosing for applications like chemical reactions or product formulation. Proper metering is vital to maintain consistent product quality and prevent overloading or underloading of downstream equipment.
Additionally, the system includes control and monitoring systems that track the level of powder in the silos, the flow rate of the conveyor, and any potential issues like blockages or leaks. Sensors and automation controls help operators maintain optimal operating conditions and respond quickly to any deviations, enhancing overall system reliability.
Design Principles for Efficient Alkali Powder Handling
The design of an industrial alkali powder handling system follows several fundamental principles aimed at maximizing efficiency, safety, and durability. First and foremost, the system must prioritize safety due to the caustic nature of alkali powders. This includes features like airtight seals, explosion-proof components, and emergency shutdown mechanisms to prevent accidental release or exposure to personnel.
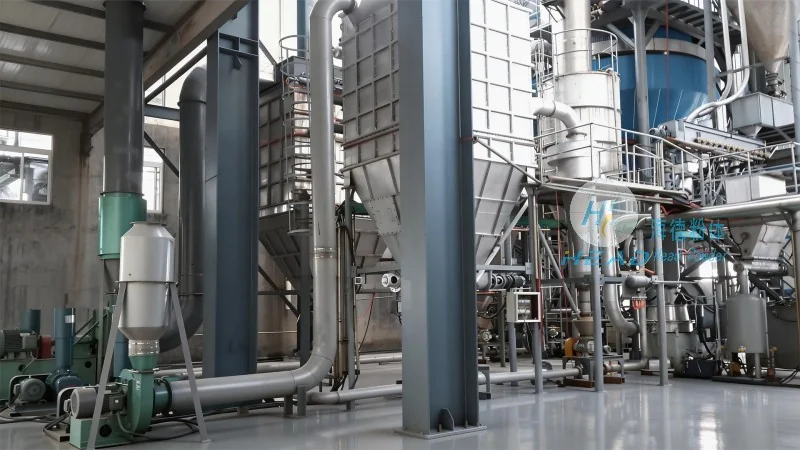
Material selection is another critical design consideration. Components that come into direct contact with the alkali powder, such as hoppers, conveyors, and storage tanks, are constructed from materials that resist corrosion and chemical degradation. Stainless steel, Hastelloy, or other specialized alloys are commonly used to ensure long-term performance and minimize maintenance costs.
Flowability and dust control are also key design aspects. Alkali powders can be hygroscopic, meaning they absorb moisture from the air, which can lead to clumping or caking. Therefore, systems often incorporate anti-static measures and moisture-proofing to maintain the powder's flowability. Additionally, dust collection systems are integrated to capture any airborne particles, protecting the environment and preventing dust-related hazards.
Energy efficiency is a modern design principle that many manufacturers now prioritize. By optimizing conveyor speeds, reducing friction in moving parts, and using energy-efficient motors, systems can operate with lower power consumption while maintaining performance. This not only reduces operational costs but also aligns with sustainability goals in industrial operations.
The Role of HeadPowder in Industrial Alkali Powder Handling Solutions
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in the design, manufacturing, and installation of custom alkali powder handling systems. The company's team of engineers and technicians works closely with clients to understand their specific requirements, whether it's for small-scale laboratory applications or large-scale industrial production lines.
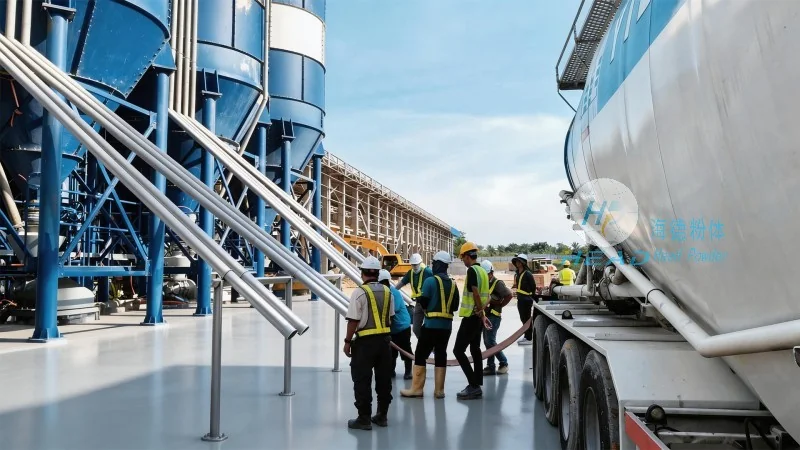
HeadPowder's solutions are tailored to meet the unique challenges of each project. For example, in a chemical manufacturing plant, the system might need to handle high volumes of sodium hydroxide while maintaining strict temperature and humidity controls. The company's engineers design custom silos and conveyors that can handle these conditions, ensuring the powder remains in a stable state throughout the process.
One of the key advantages of working with HeadPowder is their focus on integration and automation. The company integrates control systems that allow for real-time monitoring and remote operation, enabling operators to manage the system from a central control room. This not only improves efficiency but also enhances safety by reducing the need for manual handling of hazardous materials.
HeadPowder also provides comprehensive after-sales support, including maintenance services and spare parts availability. This ensures that clients can rely on their systems for long-term operation, minimizing downtime and maximizing productivity. By combining technical expertise with a customer-centric approach, HeadPowder has established itself as a trusted partner in the industrial alkali powder handling industry.