

What is a Tonne Bag Discharge Bulk Powder Handling Equipment? And What Are Its Design Principles?
When it comes to efficiently handling and transporting bulk powders in industrial settings, the tonne bag discharge bulk powder handling equipment emerges as a critical solution. This specialized machinery is designed to streamline the process of unloading and conveying powders from tonne bags, which are commonly used for storing and transporting large quantities of dry bulk materials. Understanding the functionality and design principles behind this equipment is essential for industries that rely on consistent and reliable powder handling operations.
Introducing the Tonne Bag Discharge Bulk Powder Handling Equipment
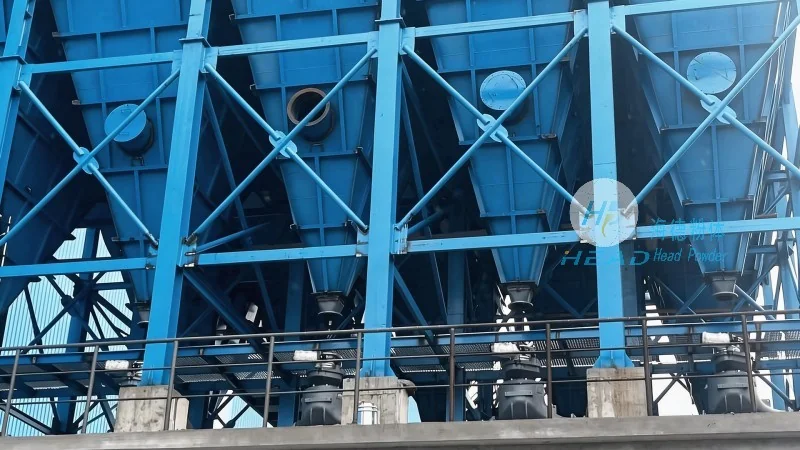
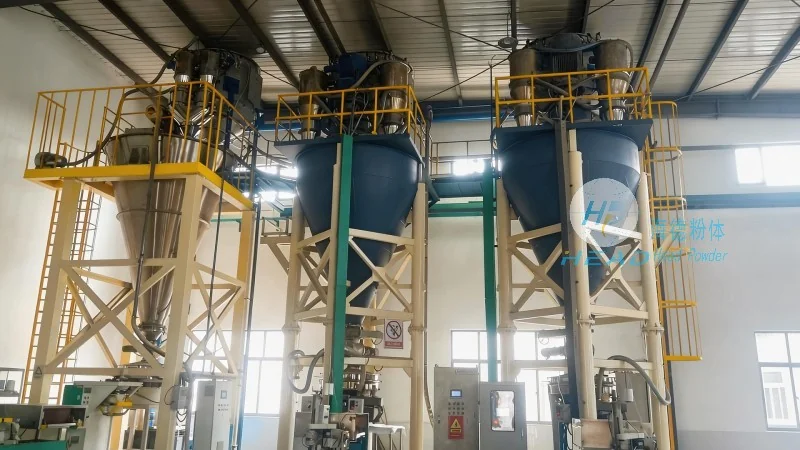
At the core of many bulk material handling systems is the tonne bag discharge equipment, a device engineered to facilitate the smooth transfer of powders from tonne bags into processing lines, storage silos, or other handling equipment. The equipment typically consists of a hopper or receiving chamber that accommodates the tonne bag, a discharge mechanism that opens the bag to release the material, and a conveyor system that transports the powder to its destination. This integrated approach ensures that the entire process—from bag opening to material transfer—is carried out in a controlled and efficient manner.
Key Components and Their Functions
The tonne bag discharge bulk powder handling equipment comprises several key components, each playing a vital role in the overall operation. The first component is the bag support and sealing system, which secures the tonne bag in place and prevents material spillage during discharge. This system often includes a clamping or sealing mechanism that holds the bag open while the powder is being released. The second component is the discharge valve or opening mechanism, which may be mechanical, pneumatic, or hydraulic, depending on the specific design. This mechanism is responsible for breaking the seal of the tonne bag and allowing the powder to flow out. The third component is the conveyor system, which can be a screw conveyor, belt conveyor, or pneumatic conveyor, depending on the material characteristics and application requirements. This system transports the discharged powder to the next stage of the process, such as a silo or processing machine. Additionally, the equipment may include a dust collection system to control airborne particles and maintain a safe working environment.
Design Principles Behind the Equipment
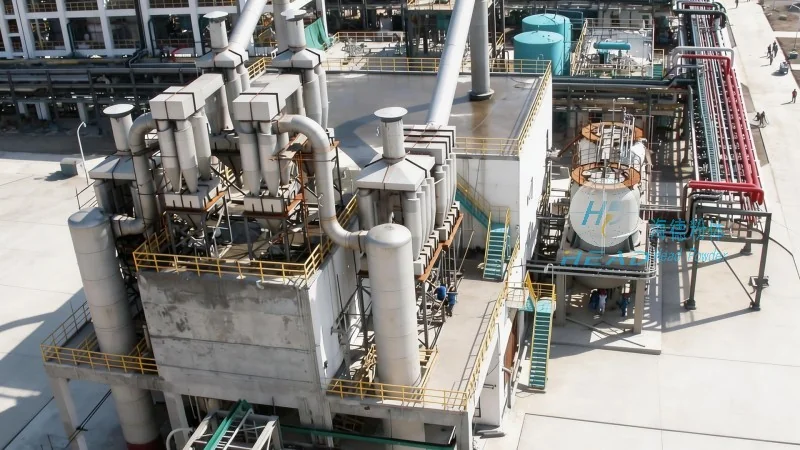
The design of tonne bag discharge bulk powder handling equipment is guided by several fundamental principles aimed at maximizing efficiency, safety, and reliability. One of the primary principles is the minimization of material loss and spillage. This is achieved through precise control of the discharge process, ensuring that the entire contents of the tonne bag are transferred without waste. Another key principle is the prevention of dust generation and inhalation hazards. The equipment is equipped with dust collection systems, such as cyclones or bag filters, which capture airborne particles and return them to the material stream or safely dispose of them. This not only improves workplace safety but also maintains the quality of the powder by preventing contamination from external sources. A third principle is the adaptability to different material types and bag sizes. The design allows for flexibility in handling various powders, including fine, cohesive, or abrasive materials, and accommodates different tonne bag dimensions, ensuring compatibility with existing storage and processing systems. Furthermore, the equipment is built for durability and ease of maintenance, with components that can withstand the rigors of continuous operation and are designed for quick replacement or servicing.
Applications and Industries
The tonne bag discharge bulk powder handling equipment finds extensive application across a wide range of industries that handle bulk powders. In the chemical industry, it is used for the transfer of raw materials and finished products, such as fertilizers, pigments, and pharmaceutical powders. In the food and beverage industry, it is employed for handling ingredients like flour, sugar, and spices, ensuring hygienic and efficient processing. The pharmaceutical industry relies on this equipment for the handling of active pharmaceutical ingredients (APIs) and other sensitive powders, where contamination control is paramount. In the agricultural sector, it is used for the transfer of fertilizers and pesticides, facilitating efficient distribution to farms. Additionally, in the mining and mineral processing industries, it is utilized for the handling of ores and other bulk materials, contributing to the overall efficiency of the extraction and processing operations.
Benefits of Using Tonne Bag Discharge Equipment
Implementing tonne bag discharge bulk powder handling equipment offers numerous benefits to industrial operations. Firstly, it significantly improves operational efficiency by reducing the time and labor required for manual bag handling. The automated discharge process allows for continuous operation, minimizing downtime and increasing overall productivity. Secondly, it enhances safety by eliminating the need for manual handling of heavy tonne bags, which can cause injuries and strain. The equipment also reduces the risk of dust-related health issues through effective dust control measures. Thirdly, it improves material quality by preventing contamination and loss during transfer. The controlled discharge process ensures that the powder remains in its original state, maintaining its purity and characteristics. Fourthly, it provides cost savings through reduced material waste and lower labor costs. The equipment is designed to transfer the entire contents of the tonne bag, minimizing waste and lowering the cost of raw materials. Additionally, the durability and low maintenance requirements of the equipment contribute to long-term cost savings.
Conclusion
In conclusion, the tonne bag discharge bulk powder handling equipment is a vital component in modern industrial operations, designed to efficiently and safely handle bulk powders from tonne bags. Its design principles, which prioritize efficiency, safety, and adaptability, make it an essential tool for industries that rely on consistent and reliable powder handling. By understanding the functionality and benefits of this equipment, businesses can enhance their operational performance, reduce costs, and improve workplace safety. As a leading provider of bulk powder handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality tonne bag discharge equipment tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder continues to deliver reliable and efficient solutions for bulk powder handling challenges.