

What is a Tote Bag Dust-Free Loading Station for Powder Material Handling? What are its Design Princ
For industrial applications that require the safe and efficient handling of bulk powders, a tote bag dust-free loading station represents a critical piece of equipment. This system is engineered to minimize dust emissions, ensure material integrity, and streamline the transfer of powders from bulk storage to processing lines. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of specialized powder handling equipment, specializes in designing and manufacturing such systems to meet the stringent requirements of industries like pharmaceuticals, food processing, chemicals, and plastics.
Understanding the Tote Bag Dust-Free Loading Station
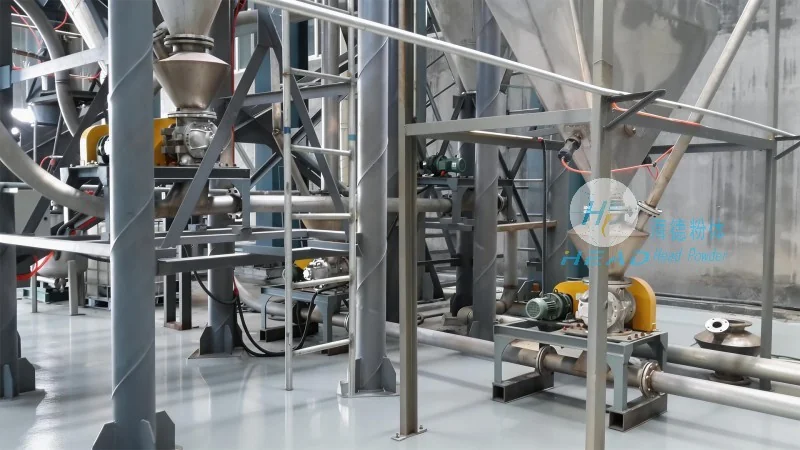
A tote bag dust-free loading station is a specialized system designed to facilitate the transfer of bulk powders from a tote bag (or bulk bag) into a processing or storage system while maintaining a controlled, dust-free environment. The primary goal is to prevent the release of airborne particles, which can be hazardous to workers and compromise product quality. These stations are commonly used in industries such as pharmaceuticals, food processing, chemicals, and plastics, where powder purity and worker safety are paramount.
Key Components of the Tote Bag Dust-Free Loading Station
The effectiveness of a tote bag dust-free loading station is attributed to its integrated components, each playing a crucial role in maintaining a clean and efficient operation. The main components typically include:
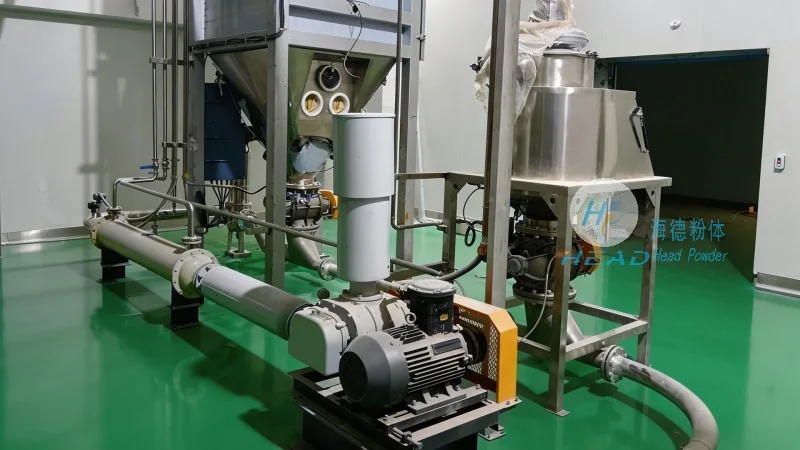
- Tote Bag Discharge System: This component is responsible for opening the tote bag and controlling the flow of powder. It often features a valve or spout that can be operated remotely to regulate the discharge rate, preventing overloading or underflow.
- Dust Extraction and Filtration: A critical feature is the integrated dust extraction system, which captures airborne particles during the discharge process. High-efficiency particulate air (HEPA) filters or other filtration technologies are employed to ensure that the exhaust air is clean and compliant with environmental regulations.
- Airlock or Rotary Valve: To prevent backflow and maintain a sealed environment, an airlock or rotary valve is used. This component allows the powder to pass through while keeping the system pressurized or under vacuum, preventing dust from entering the workspace.
- Enclosure and Ventilation: The entire system is enclosed in a robust, dust-tight housing. This enclosure is equipped with ventilation systems that draw air through the filtration unit, ensuring that the internal environment remains clean and free from contaminants.
- Control Panel: A user-friendly control panel allows operators to manage the discharge process, monitor system performance, and adjust settings as needed. This feature enhances operational efficiency and safety.
Design Principles for Optimal Performance
The design of a tote bag dust-free loading station is guided by several key principles to ensure reliability, safety, and efficiency. These principles are tailored to meet the specific requirements of different industries and applications:
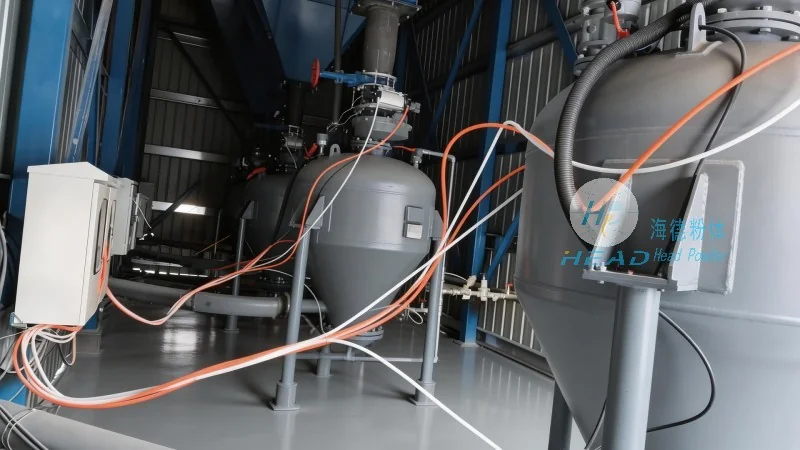
- Seal Integrity: The system is designed with tight seals at all points of contact, including the tote bag opening and the discharge line. This prevents dust leakage and maintains a controlled environment.
- Material Compatibility: Components are selected to be compatible with the specific powder being handled. For example, in pharmaceutical applications, materials must meet stringent sanitary and cleanroom standards.
- Airflow Management: The design incorporates optimized airflow patterns to ensure thorough dust capture and prevent the buildup of particles within the system. This includes the use of positive or negative pressure systems to control air movement.
- Modularity and Scalability: The system is designed to be modular, allowing for easy integration with existing processing lines and scalability to accommodate different tote bag sizes and powder volumes.
Applications and Benefits
Tote bag dust-free loading stations are widely used across various industries due to their ability to handle bulk powders safely and efficiently. The benefits of implementing such a system include:
- Enhanced Worker Safety: By containing dust emissions, the system reduces the risk of respiratory issues and other health hazards associated with powder handling.
- Improved Product Quality: Maintaining a dust-free environment ensures that the powder remains uncontaminated, preserving its quality and meeting regulatory standards.
- Increased Operational Efficiency: The controlled discharge process allows for precise material transfer, reducing waste and optimizing production throughput.
- Compliance with Regulations: The system is designed to meet environmental and occupational health regulations, ensuring that operations are legally compliant.
Conclusion
A tote bag dust-free loading station is a sophisticated piece of equipment that combines advanced engineering and design principles to address the challenges of bulk powder handling. By integrating dust extraction, airlock systems, and robust enclosures, these stations provide a safe, efficient, and compliant solution for industries that rely on powder materials. The design principles and components work in harmony to ensure that the transfer of powders is performed with minimal risk and maximum efficiency, making them an essential investment for modern industrial operations.