

What is Sodium Bicarbonate Powder Handling Equipment? And What Are Its Design Principles?
Understanding the specialized equipment designed for handling sodium bicarbonate powder is crucial for industries that rely on this chemical. Sodium bicarbonate, commonly known as baking soda, is a white crystalline powder with a slightly alkaline taste. It is widely used in food processing, pharmaceuticals, and chemical manufacturing. However, due to its fine particle size and potential for dust generation, specialized equipment is required to ensure safe and efficient handling. This article explores the types of equipment used for sodium bicarbonate powder handling and the underlying design principles that make these systems effective.
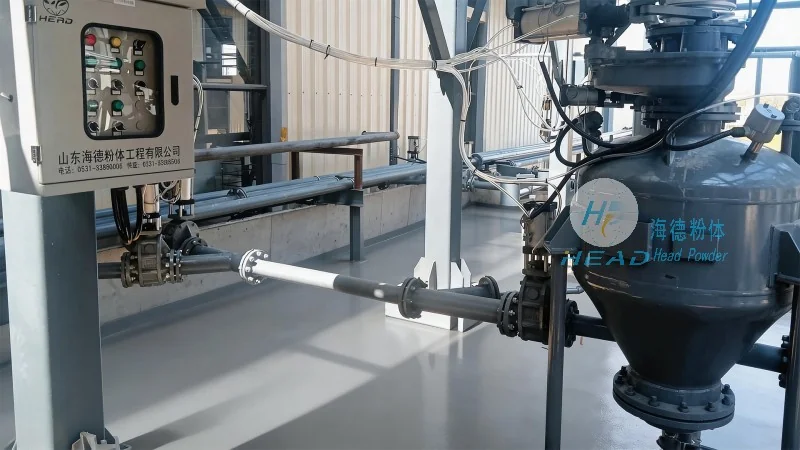
Introduction to Sodium Bicarbonate Powder Handling Equipment
Sodium bicarbonate powder handling equipment is engineered to manage the unique properties of this chemical. The primary goal is to prevent dust contamination, ensure product purity, and maintain operational safety. These systems are typically designed with features that address the challenges posed by fine powders, such as dust generation, caking, and the need for hygienic conditions. The equipment is often customized to meet the specific requirements of the application, whether it's for bulk storage, conveying, or processing.
Key Design Principles for Sodium Bicarbonate Powder Handling Systems
The design of sodium bicarbonate powder handling equipment is guided by several critical principles to ensure optimal performance. One of the most important is the emphasis on airtight and dust-tight construction. This prevents the release of fine particles into the environment, which is essential for both safety and regulatory compliance. The equipment is also designed to minimize the risk of caking, which can occur when the powder is exposed to moisture or air. This is achieved through features like anti-static coatings and proper ventilation systems.
Another key principle is the use of appropriate conveying methods. For sodium bicarbonate, pneumatic conveying systems are often preferred due to their ability to handle fine powders efficiently. These systems use air to transport the powder through a network of pipes, reducing the need for mechanical components that could cause wear or contamination. Alternatively, mechanical conveyors like screw conveyors may be used for applications where a more direct, low-pressure transport is required. The choice of conveying method depends on factors such as the volume of material, the distance to be covered, and the need for product purity.
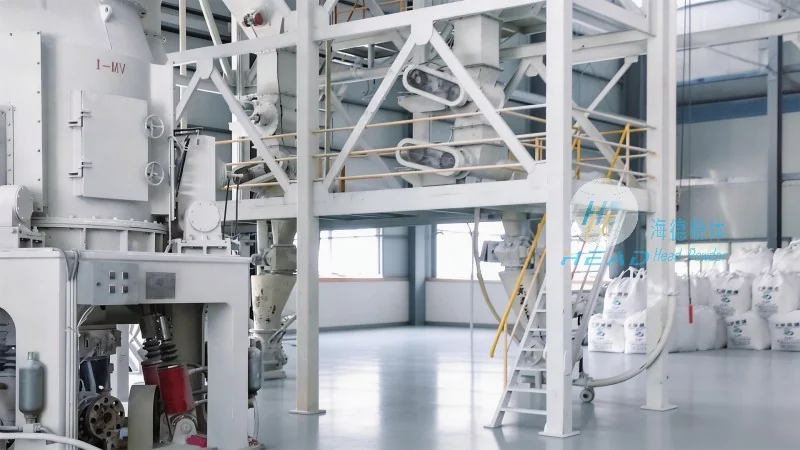
Components and Features of Sodium Bicarbonate Powder Handling Equipment
Sodium bicarbonate powder handling equipment typically includes several key components that work together to ensure efficient operation. These components may include hoppers for bulk storage, feeders to control the flow of powder, and conveyors to transport the material. The hoppers are often designed with smooth, sloped surfaces to prevent caking and ensure uniform discharge. Feeders, such as rotary valves or vibratory feeders, are used to regulate the flow rate, preventing overloading or underloading of the conveying system.
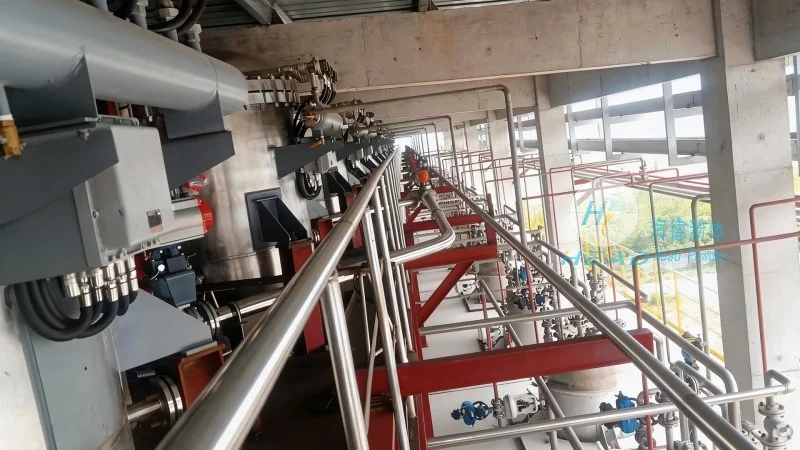
Conveyors, whether pneumatic or mechanical, are designed to handle the specific characteristics of sodium bicarbonate. Pneumatic systems use positive or negative pressure to move the powder, with positive pressure being more common for handling fine powders. The pipelines are often made of materials like stainless steel or polyethylene to resist corrosion and prevent contamination. Mechanical conveyors, such as screw conveyors, use rotating screws to push the powder through the system, providing a continuous and reliable flow.
The Role of HeadPowder Engineering in Sodium Bicarbonate Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of specialized powder handling equipment. With a focus on quality and innovation, HeadPowder provides tailored solutions for industries that require efficient and safe handling of sodium bicarbonate. The company's expertise lies in understanding the unique challenges of handling fine powders and designing systems that address these challenges effectively. Their equipment is built to meet international standards for safety and hygiene, ensuring that it is suitable for use in food, pharmaceutical, and chemical applications.
HeadPowder's approach to sodium bicarbonate powder handling equipment involves a comprehensive understanding of the material's properties and the operational requirements of the client. The company works closely with customers to assess their specific needs, from bulk storage to processing, and designs equipment that maximizes efficiency while minimizing downtime and maintenance. Their products are known for their durability, reliability, and ease of maintenance, making them a preferred choice for industries that demand high-performance powder handling solutions.
Benefits of Using Specialized Sodium Bicarbonate Powder Handling Equipment
Investing in specialized sodium bicarbonate powder handling equipment offers several benefits for businesses. First, it improves operational efficiency by ensuring a consistent and reliable flow of material. This reduces downtime and increases productivity, which is critical for meeting production targets. Second, it enhances safety by preventing dust exposure and minimizing the risk of accidents. This is particularly important in industries where worker safety is a top priority. Third, it maintains product quality by preventing contamination and ensuring that the powder remains pure throughout the handling process. This is essential for applications where product purity is non-negotiable, such as in food and pharmaceutical manufacturing.
Additionally, specialized equipment can help reduce costs in the long run. By minimizing material loss due to dust and caking, businesses can save on raw material costs. The efficient design of the equipment also reduces energy consumption, leading to lower operational costs. Furthermore, the durability and reliability of the equipment mean that maintenance and repair costs are kept to a minimum, contributing to overall cost savings.
Conclusion
In conclusion, sodium bicarbonate powder handling equipment is a critical component for industries that rely on this versatile chemical. The design principles behind these systems focus on safety, efficiency, and product purity. By understanding the unique properties of sodium bicarbonate and applying appropriate design features, manufacturers can create equipment that meets the needs of various applications. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these specialized solutions, helping businesses to improve their operations and maintain high standards of safety and quality.