

What is a Ton Bag Powder Conveying System Equipment? What is its Design Principle?
Ton bag powder conveying systems are specialized industrial equipment designed to handle and transport bulk powders from ton bags into processing facilities. These systems are essential in industries such as pharmaceuticals, food processing, chemical manufacturing, and more, where efficient and safe material handling is critical. The equipment is engineered to automate the transfer of powders, reducing manual labor and minimizing the risk of contamination or spills.
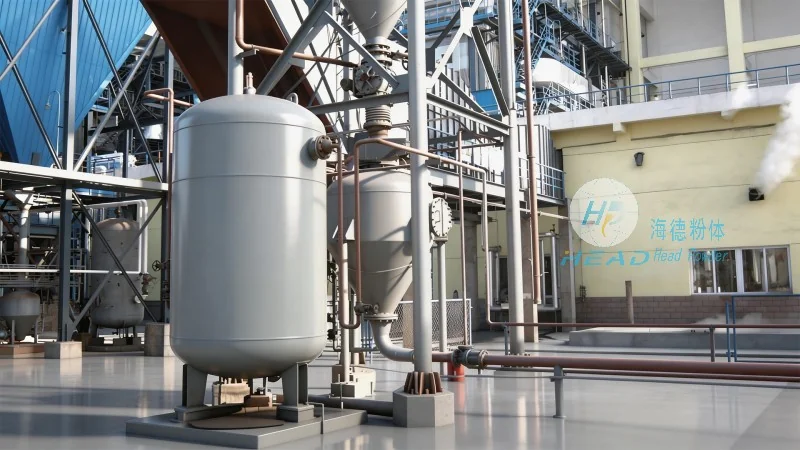
About HeadPowder: Your Expert in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced powder handling equipment. With a strong presence in China, particularly in Shandong, the company specializes in developing customized solutions for various industrial applications. Their expertise lies in creating reliable, efficient, and user-friendly systems that meet the specific needs of clients across different sectors.
Key Components of Ton Bag Powder Conveying Systems
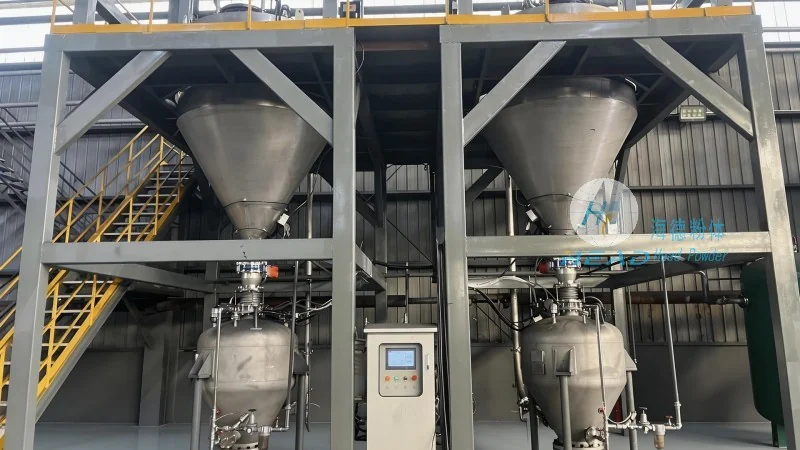
The ton bag powder conveying system typically consists of several key components that work together to ensure smooth operation. These include the ton bag discharging mechanism, a hopper or receiving tank, a conveyor system (such as a screw conveyor or pneumatic conveyor), and control panels. The ton bag discharging mechanism is designed to safely open and empty the ton bag, while the hopper collects the material and feeds it into the conveyor. The conveyor then transports the powder to the processing area or storage location. Each component is engineered to handle the specific characteristics of the powder, such as particle size, moisture content, and flowability.
Design Principles Behind Ton Bag Powder Conveying Systems
The design of ton bag powder conveying systems follows several fundamental principles to ensure optimal performance and safety. One of the primary principles is the use of airtight and sealed systems to prevent dust emissions and maintain a clean environment. This is crucial in industries where dust can be hazardous or affect product quality. The systems are also designed with material compatibility in mind, ensuring that all components can withstand the chemical and physical properties of the powders being handled. Another key principle is the integration of automation and control systems, which allow for precise control over the conveying process, including flow rates, pressure, and temperature. This not only enhances efficiency but also reduces the risk of human error.
Advantages of Using Ton Bag Powder Conveying Systems
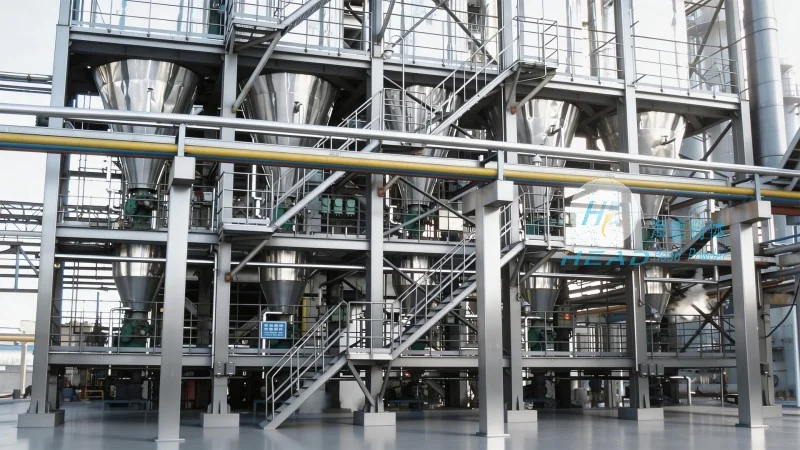
Implementing a ton bag powder conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves operational efficiency by automating the material handling process, reducing downtime and labor costs. The systems are designed to handle large quantities of powder, making them ideal for high-volume production environments. Secondly, they enhance safety by minimizing the risk of manual handling, which can lead to accidents or exposure to hazardous materials. The sealed and airtight design also helps in maintaining a clean and controlled environment, which is essential in industries like pharmaceuticals and food processing. Additionally, these systems are highly customizable, allowing companies to tailor the equipment to their specific requirements, ensuring optimal performance and cost-effectiveness.
Applications and Industries Benefiting from Ton Bag Powder Conveying Systems
Ton bag powder conveying systems are widely used across various industries due to their versatility and efficiency. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are transferred without contamination. In the food processing industry, they are used to transport ingredients such as flour, sugar, and spices, maintaining the quality and safety of the products. The chemical manufacturing industry also benefits from these systems, as they can handle a wide range of chemical powders, including those that are corrosive or reactive. Additionally, in the agricultural sector, ton bag powder conveying systems are used to transport fertilizers and other agricultural chemicals, improving the efficiency of farm operations.
Conclusion: Choosing the Right Ton Bag Powder Conveying System
When selecting a ton bag powder conveying system, it is essential to consider the specific requirements of your operation, including the type of powder, volume, and industry regulations. HeadPowder, with its expertise and experience, offers a range of high-quality systems that are designed to meet these needs. By investing in a reliable ton bag powder conveying system, companies can enhance their operational efficiency, improve safety, and maintain the quality of their products. The design principles and components of these systems ensure that they are robust, efficient, and suitable for various industrial applications.