

What Are Food Additive Material Handling Equipment? And What Are Their Design Principles?
Food additive material handling equipment plays a crucial role in the food processing industry, particularly in the storage, transport, and distribution of various food additives. These specialized machines are designed to ensure the safe and efficient movement of ingredients such as preservatives, colorants, flavor enhancers, and other additives that are essential for food production. The design principles behind these equipment are centered on maintaining product integrity, preventing contamination, and optimizing operational efficiency.
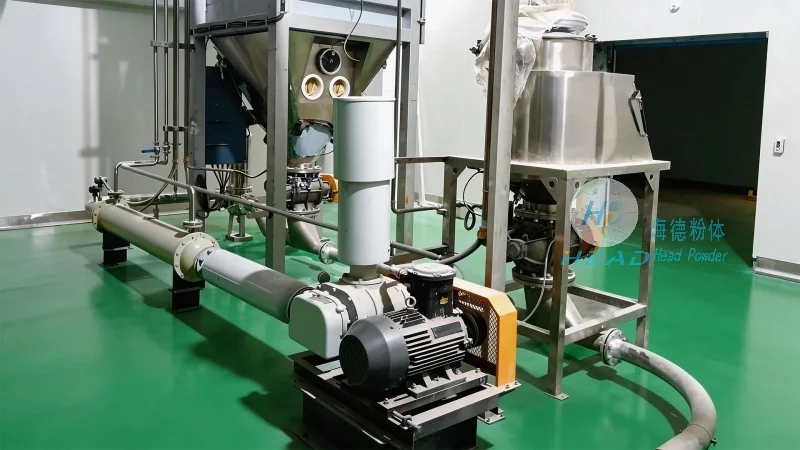
Key Components and Functions of Material Handling Equipment for Food Additives
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of high-quality material handling systems tailored for food additive applications. The core components of these systems typically include conveyors, hoppers, feeding mechanisms, and control panels. Conveyors, such as belt conveyors or screw conveyors, are commonly used to transport bulk food additives from storage silos to processing lines. Hoppers are used to store and feed the additives in a controlled manner, ensuring a steady flow of material. Feeding mechanisms, like rotary valves or vibratory feeders, regulate the quantity of additives released, while control panels allow operators to monitor and adjust the system parameters in real-time. The integration of these components ensures that the material handling process is precise, consistent, and meets stringent industry standards.
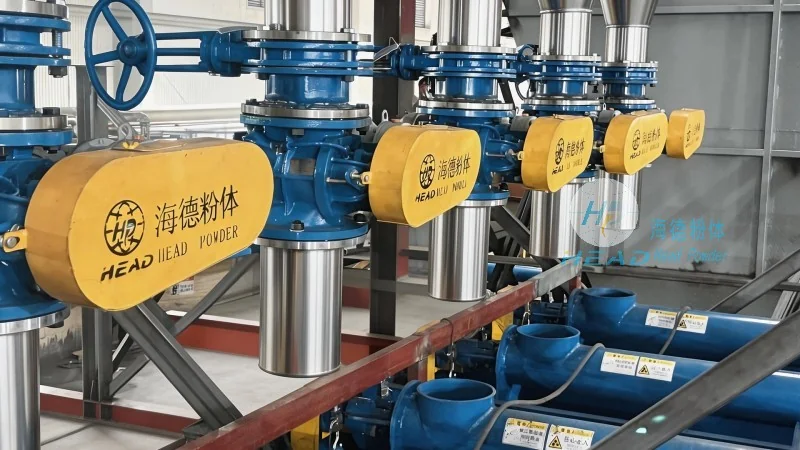
Design Principles for Ensuring Safety and Compliance
The design of food additive material handling equipment adheres to strict safety and regulatory requirements. One of the primary principles is the prevention of cross-contamination. Materials are often separated by using stainless steel construction, which is non-porous and easy to clean. Additionally, the equipment is designed with smooth surfaces and minimal dead zones to facilitate thorough sanitation. Another critical principle is the maintenance of product integrity. Temperature control systems are incorporated to prevent heat-sensitive additives from degrading during transport. For example, some systems use insulated conveyors to maintain the temperature of perishable additives. The design also considers the hygienic handling of powders, with features like dust collection systems to minimize airborne particles and ensure a clean working environment. These principles are essential to comply with food safety regulations, such as those set by the FDA and EU food safety directives.
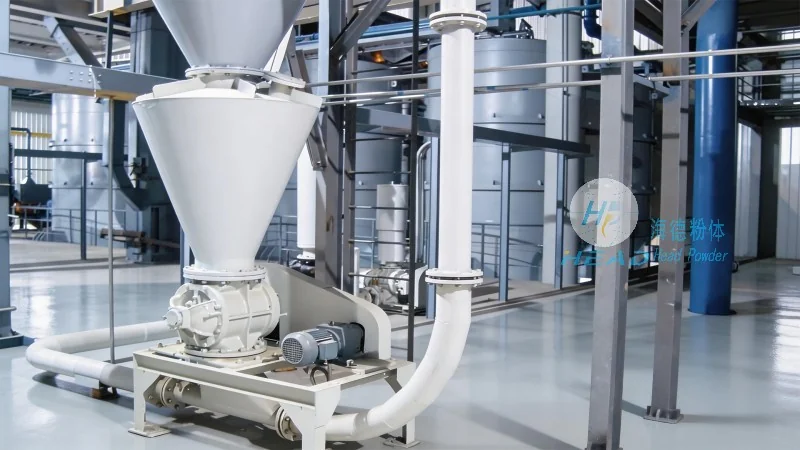
Operational Efficiency and Customization in Material Handling Solutions
HeadPowder’s material handling equipment is engineered to enhance operational efficiency in food additive processing. The systems are designed to handle a wide range of additive types, from fine powders to granules, with adjustable settings that can be tailored to specific product characteristics. For instance, the speed of the conveyor can be adjusted to control the flow rate of fine powders, preventing clogging and ensuring smooth operation. The feeding mechanisms are equipped with sensors that detect the level of material in the hopper, automatically adjusting the feed rate to maintain a consistent output. This automation reduces labor costs and minimizes the risk of human error. Furthermore, the equipment is modular, allowing for easy integration with existing production lines. This flexibility enables food processing companies to scale their operations as needed without significant modifications to the infrastructure. The company’s expertise in customizing solutions ensures that each system is optimized for the specific needs of the client, whether it’s for a small-scale production facility or a large industrial plant.
Conclusion: The Importance of Reliable Material Handling Equipment
In conclusion, food additive material handling equipment is a vital component of modern food processing operations. The design principles behind these systems prioritize safety, compliance, and efficiency, ensuring that food additives are handled in a manner that maintains their quality and meets regulatory standards. HeadPowder, with its headquarters in Shandong, China, has established itself as a trusted provider of these specialized equipment, offering customized solutions that cater to the diverse needs of the food industry. By investing in high-quality material handling systems, food processing companies can enhance their operational performance, reduce costs, and ensure the consistent delivery of high-quality food additives to their customers.