

What is a Nitrogen-Protected Powder Conveyor? Understanding Its Design Principles
For industries dealing with sensitive powders, the choice of material handling equipment is critical. A nitrogen-protected powder conveyor is a specialized system designed to maintain an inert atmosphere during the transport of powders, preventing oxidation, moisture absorption, and other contaminants that could compromise product quality. This article delves into what a nitrogen-protected powder conveyor is and explores the key design principles that make it effective.
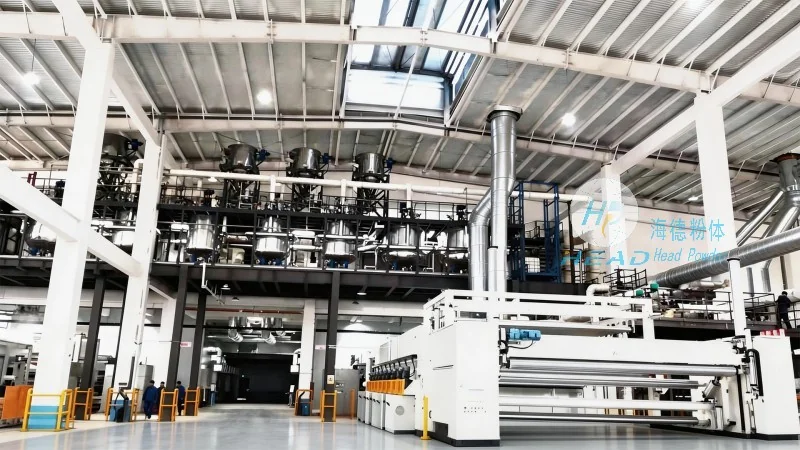
Introduction to Nitrogen-Protected Powder Conveyors
In many industrial applications, powders such as pharmaceuticals, food ingredients, and specialty chemicals are highly reactive to air and moisture. Conventional conveyor systems expose these materials to the ambient environment, leading to degradation, caking, or contamination. To address these challenges, nitrogen-protected powder conveyors are engineered to create and maintain a controlled inert atmosphere, typically using nitrogen gas to displace oxygen and moisture from the system. This ensures that the powder remains stable and pure throughout the handling process.
Key Design Principles of Nitrogen-Protected Powder Conveyors
The effectiveness of a nitrogen-protected powder conveyor hinges on several critical design elements that work in concert to preserve the integrity of the material. These principles include:
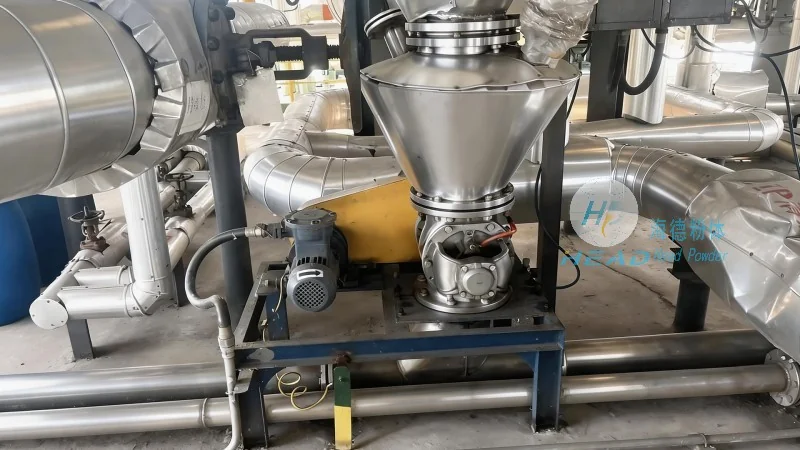
1. Airtight Sealing and Enclosure - The entire conveyor system, including hoppers, pipes, and transfer points, is constructed with high-quality, airtight materials. Seals and gaskets are used to prevent any air infiltration, ensuring that the nitrogen atmosphere remains stable. This design minimizes the risk of oxygen or moisture entering the system and affecting the powder.
2. Nitrogen Gas Supply and Purification - A continuous supply of high-purity nitrogen gas is essential. The system includes a nitrogen generator or supply line that maintains a slight positive pressure within the conveyor. This positive pressure helps to push out any contaminants and prevents external air from entering. The nitrogen is often filtered to remove particulates and moisture, ensuring it is clean and effective.
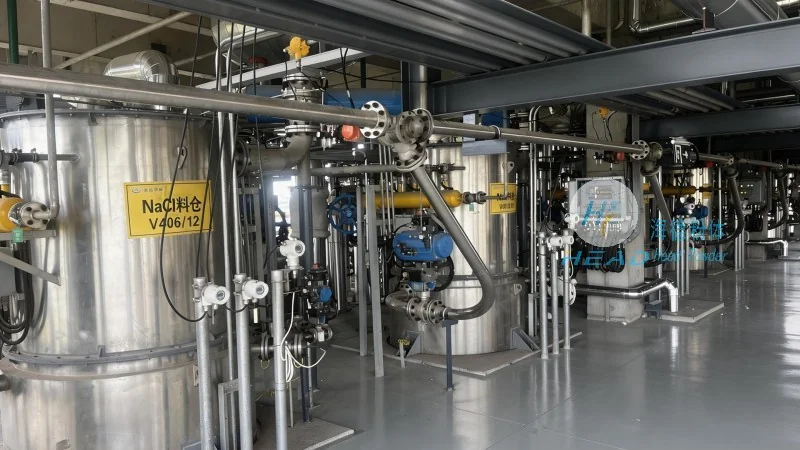
3. Material Compatibility - All components in contact with the powder, such as hoppers, pipes, and valves, are made from materials that are chemically inert and non-reactive. Common choices include stainless steel, PTFE, or specialized polymers that do not absorb moisture or react with the powder. This prevents contamination and ensures the system's longevity.
4. Controlled Flow and Minimal Friction - The design of the conveyor, including the choice of conveyor type (e.g., pneumatic or mechanical) and the use of smooth surfaces, minimizes friction and particle degradation. This is crucial for maintaining the powder's properties and preventing caking or agglomeration. The system may also include vibration or agitation features to ensure consistent flow without damaging the material.
5. Monitoring and Safety Features - Modern nitrogen-protected powder conveyors are equipped with monitoring systems to track pressure, temperature, and gas purity. These features provide real-time feedback on the system's performance and alert operators to any deviations from the desired conditions. Safety interlocks and emergency shut-off valves are also integrated to prevent accidents and protect both the equipment and the material.
Applications and Benefits
Nitrogen-protected powder conveyors are widely used in industries where product purity and stability are paramount. Some common applications include:
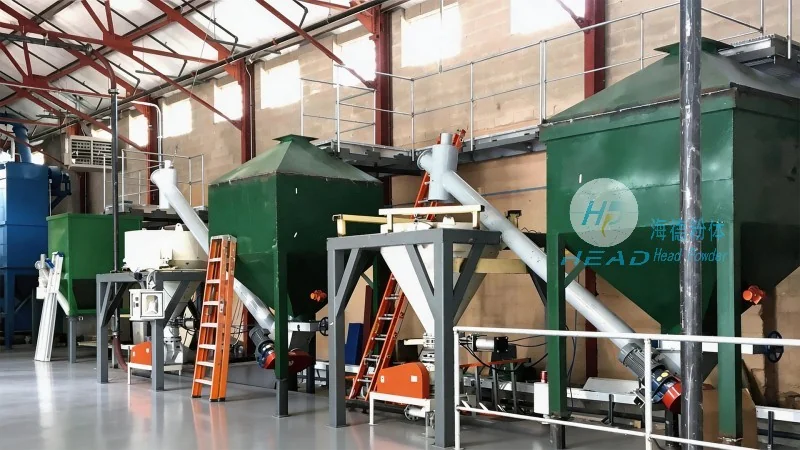
- Pharmaceutical Manufacturing: For handling active pharmaceutical ingredients (APIs) and excipients, where contamination can lead to product recalls or safety issues.
- Food and Beverage Industry: For transporting ingredients like spices, flour, or powdered milk, where moisture and oxidation can affect flavor and shelf life.
- Chemical Processing: For handling reactive chemicals or specialty powders that require an inert environment to prevent reactions or degradation.
By implementing these design principles, nitrogen-protected powder conveyors offer several key benefits:
- Preservation of Product Quality: Maintaining the powder's original properties, ensuring consistent performance and reducing waste.
- Enhanced Safety: Reducing the risk of fire, explosion, or chemical reactions caused by oxygen exposure.
- Increased Efficiency: Minimizing downtime due to caking or contamination and improving overall process flow.
- Compliance with Regulations: Meeting stringent industry standards for product purity and handling, which is critical for regulatory compliance.
Conclusion
A nitrogen-protected powder conveyor is a sophisticated system designed to handle sensitive powders while preserving their quality and integrity. Through careful design, including airtight sealing, nitrogen gas management, material compatibility, controlled flow, and monitoring systems, these conveyors provide a reliable solution for industries where product purity is non-negotiable. As a leader in powder handling technology, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing such systems, ensuring that clients receive equipment tailored to their specific needs. With a focus on innovation and quality, HeadPowder continues to advance the capabilities of nitrogen-protected powder conveyors, supporting industries in maintaining the highest standards of product quality and safety.