

What is a Multi-functional Powder Conveying System Equipment? And What Are Its Design Principles?
Multi-functional powder conveying systems are critical in various industrial sectors, offering efficient and reliable methods for transporting bulk materials. These systems are engineered to handle a wide array of powder types, from fine powders to bulkier granules, ensuring smooth and controlled movement through processing lines. Understanding the components and design principles behind such equipment is essential for optimizing operational efficiency and maintaining product quality.
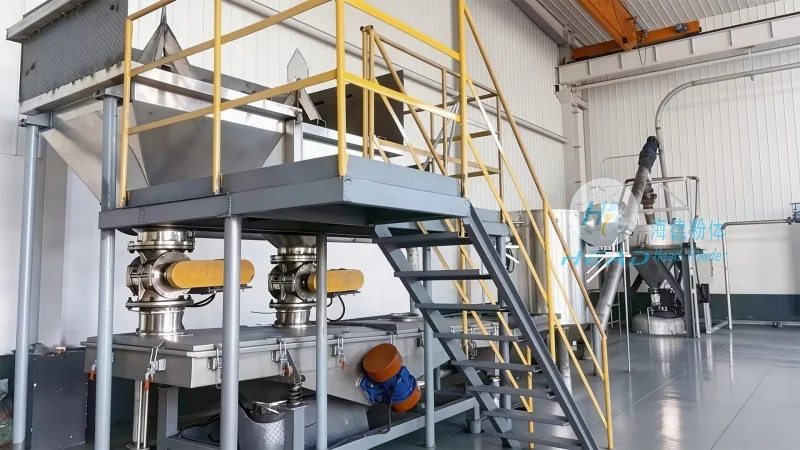
Company Introduction: HeadPowder
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in advanced powder handling solutions. With headquarters located in Shandong, China, the company has established itself as a trusted provider of high-quality conveying equipment tailored to meet diverse industrial needs. HeadPowder’s commitment to innovation and customer satisfaction drives its continuous development of cutting-edge technologies in powder processing and material transport.
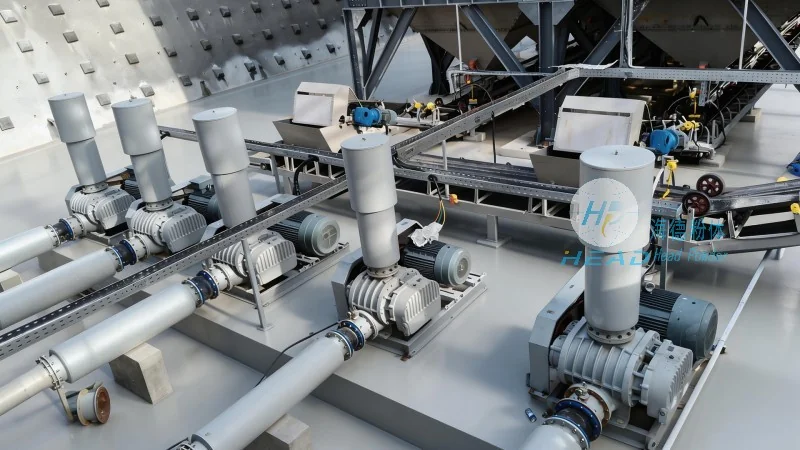
Design Principles of Multi-functional Powder Conveying Systems
The design of a multi-functional powder conveying system involves a comprehensive approach that integrates mechanical engineering, fluid dynamics, and material science. Key design principles include ensuring uniform material flow, minimizing product degradation, and maximizing energy efficiency. The system typically consists of several core components, each playing a critical role in the overall operation. For instance, the feed mechanism is responsible for accurately metering the powder, while the conveying section uses appropriate technologies like pneumatic or mechanical methods to transport the material. The control system, often equipped with advanced sensors and automation, monitors and adjusts the process parameters in real-time to maintain optimal performance.
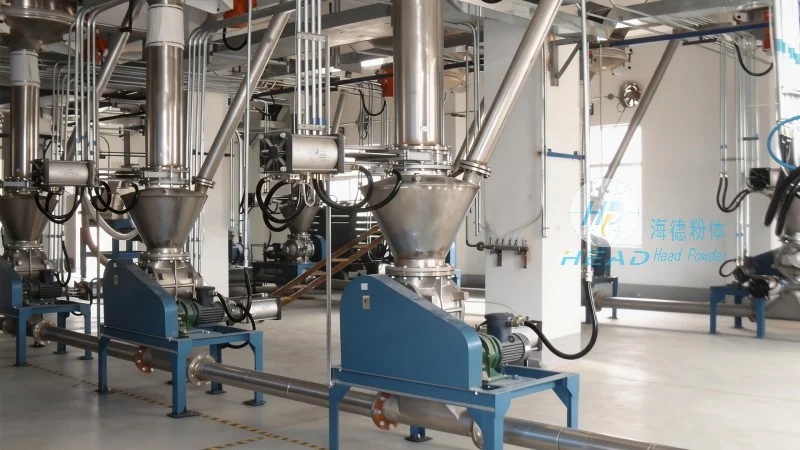
Key Features and Technical Specifications
Multi-functional powder conveying systems from HeadPowder are engineered with several distinctive features that enhance their performance and adaptability. These systems are designed to handle a broad spectrum of powder characteristics, including varying particle sizes, densities, and flowability. The equipment incorporates robust materials and precision manufacturing to ensure durability and long-term reliability. Additionally, the systems are equipped with user-friendly interfaces and modular designs, allowing for easy integration into existing production lines and future scalability. Technical specifications may vary based on specific application requirements, but common features include adjustable speed controls, pressure monitoring, and safety interlocks to prevent operational hazards.
Applications and Operational Benefits
These conveying systems find extensive applications across multiple industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical sector, for example, the systems are used to transport active ingredients and excipients with strict purity standards, ensuring no contamination or degradation. In food processing, they handle ingredients like flour, sugar, and spices, maintaining product freshness and quality. The operational benefits of using such systems include improved process control, reduced downtime, and enhanced safety for operators. By optimizing material transport, companies can achieve higher production throughput and lower operational costs, making these systems a valuable investment for any industrial operation.
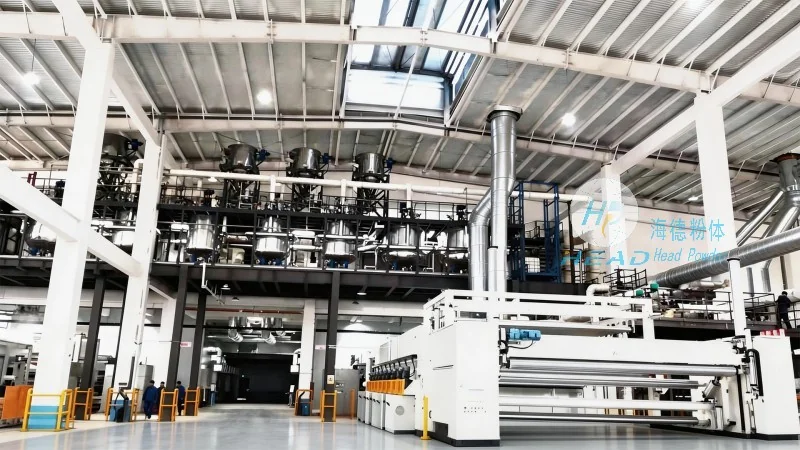
Conclusion and Company Commitment
Multi-functional powder conveying systems represent a sophisticated solution for efficient bulk material handling, combining advanced engineering with practical application. HeadPowder, as a reputable manufacturer based in Shandong, China, continues to innovate and refine its products to meet the evolving demands of the industry. By adhering to rigorous design principles and quality standards, HeadPowder ensures that its conveying systems deliver reliable performance and contribute to the success of its clients’ operations. For businesses seeking to enhance their material handling capabilities, investing in a well-designed powder conveying system is a strategic move toward improved efficiency and productivity.