

What is a Dust-Free Measuring Powder Conveying System Equipment? What are its Design Principles?
Understanding dust-free measuring powder conveying systems is crucial for industries that handle fine powders, as these systems are designed to ensure precise measurement and safe transport of powders without generating dust or contamination. This article delves into the core components, operational principles, and benefits of such systems, providing a comprehensive overview for professionals in the field.
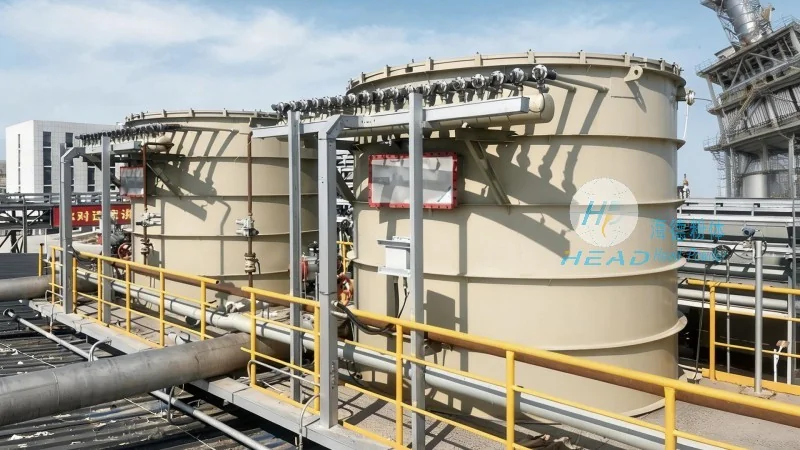
Key Components and Design Principles
A dust-free measuring powder conveying system typically consists of several critical components, each playing a vital role in maintaining a clean and efficient operation. The primary components include a dust collector, a conveying mechanism (such as a screw or pneumatic system), a measuring device (often a gravimetric or volumetric sensor), and a control unit. The design principles focus on minimizing particle loss, preventing cross-contamination, and ensuring consistent flow rates. For instance, the system may incorporate sealed hoppers and enclosed conveying lines to prevent dust from escaping into the environment. Additionally, the use of high-quality materials, such as stainless steel or food-grade plastics, ensures durability and compliance with industry standards.
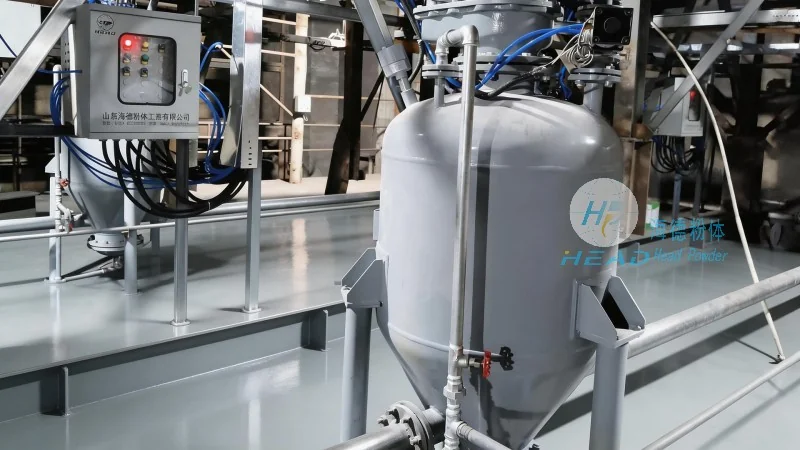
How the System Works: A Step-by-Step Overview
The operation of a dust-free measuring powder conveying system involves a series of coordinated steps to achieve accurate measurement and transport. First, the powder is fed into the system from a storage container, usually through a sealed hopper. The system then uses a conveying mechanism to move the powder to the measuring device. The measuring device, often a gravimetric scale, continuously monitors the weight of the powder passing through, providing real-time data on the flow rate. The control unit processes this data and adjusts the conveying speed to maintain the desired flow rate. This closed-loop system ensures that the powder is delivered to the destination with minimal variation, making it ideal for applications where precision is paramount.
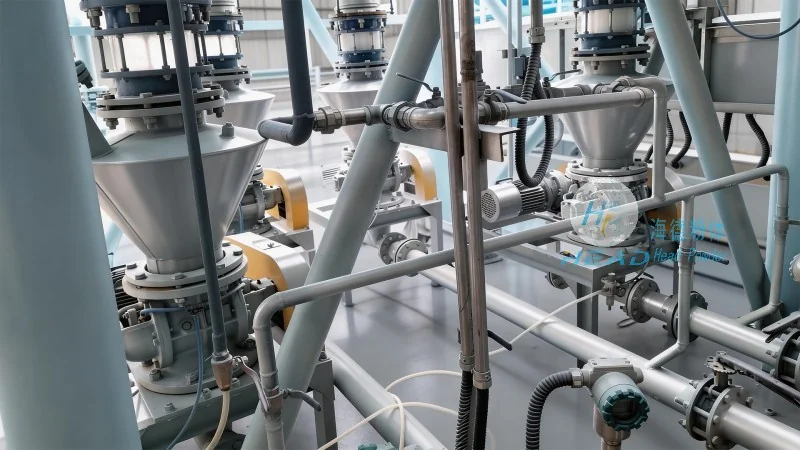
Benefits of Using a Dust-Free Measuring Powder Conveying System
Implementing a dust-free measuring powder conveying system offers numerous advantages for businesses. One of the most significant benefits is the reduction of dust exposure, which improves workplace safety and compliance with environmental regulations. By containing the powder within a sealed system, the risk of inhalation or contamination is minimized. Additionally, the system enhances product quality by preventing cross-contamination between different powders, which is critical in industries like pharmaceuticals and food processing. Another key benefit is the improved efficiency and accuracy of powder measurement. Unlike traditional methods, which may suffer from variations due to human error or equipment wear, this system provides consistent and reliable measurements, leading to better inventory management and reduced waste. Furthermore, the sealed design reduces maintenance needs by minimizing the buildup of dust on components, extending the lifespan of the equipment.
Applications and Industries That Benefit from This Technology
Dust-free measuring powder conveying systems are widely used across various industries that rely on precise powder handling. In the pharmaceutical industry, these systems are essential for ensuring the purity and consistency of active ingredients, as even small amounts of contamination can affect the efficacy of medications. Similarly, in the food and beverage industry, the systems help maintain product safety by preventing cross-contamination and ensuring that powders like flour or sugar are handled hygienically. The chemical industry also benefits from these systems, as they help manage hazardous powders while minimizing the risk of dust explosions. Additionally, in the manufacturing sector, these systems are used for handling raw materials in processes such as coating, compounding, and blending. The versatility of the system makes it suitable for a wide range of applications, from small-scale production to large industrial operations.
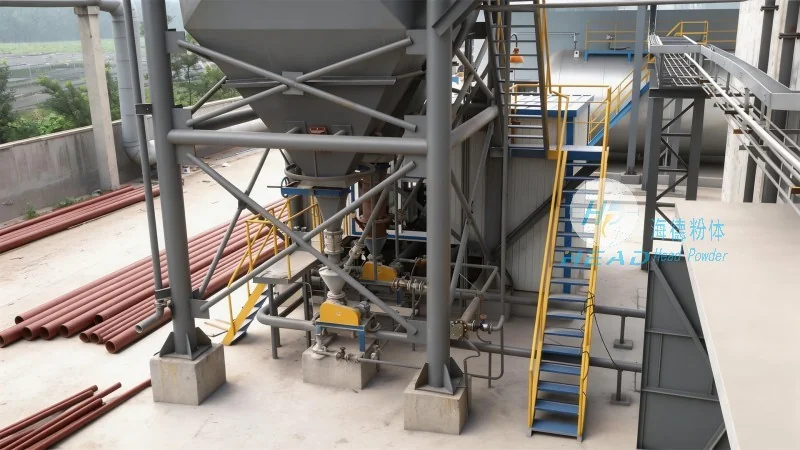
The Role of Shandong HeadPowder Engineering Co., Ltd. in Providing These Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design and production of dust-free measuring powder conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses seeking reliable and efficient powder handling solutions. Based in Shandong, China, headpowder leverages advanced technology and years of industry experience to develop systems that meet the unique needs of each client. The company’s products are designed to be customizable, allowing for integration with existing production lines and tailored to specific industry requirements. Whether for pharmaceutical, food, or chemical applications, headpowder’s systems are built to deliver precision, safety, and durability. By partnering with headpowder, businesses can enhance their operational efficiency, improve product quality, and ensure compliance with industry standards, making it a valuable investment for long-term success.