

What is a Coal and Stone Powder Material Handling System? What are the Design Principles?
Coal and stone powder material handling systems are critical components in industrial operations, particularly in the mining, power generation, and processing sectors. These systems are engineered to efficiently transport bulk materials like coal, stone powders, and other fine particulates from one location to another. Understanding the core components and design principles behind such systems is essential for optimizing material flow, reducing operational costs, and ensuring safety in industrial environments.
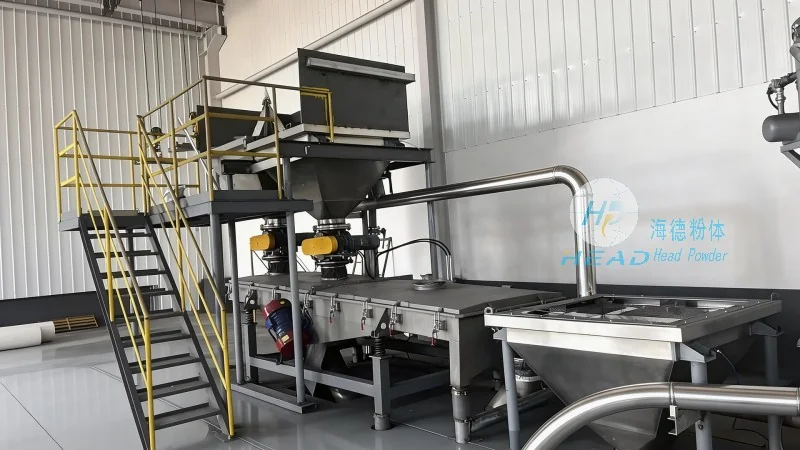
Understanding the Coal and Stone Powder Material Handling System
A coal and stone powder material handling system typically consists of several key elements, including feeders, conveyors, storage silos, and control systems. The primary function is to move raw materials from their source to processing or storage areas. For example, in a coal-fired power plant, these systems transport coal from stockpiles to the boiler, ensuring a continuous and reliable supply. The design of the system must account for the physical properties of the materials, such as particle size, density, and moisture content, to prevent issues like blockages or material degradation.
Key Design Principles for Efficient Material Transport
The design of a coal and stone powder material handling system is guided by several fundamental principles aimed at maximizing efficiency and reliability. One of the most critical principles is the selection of appropriate equipment based on the material's characteristics. For instance, screw conveyors are often used for handling dry, free-flowing powders, while belt conveyors may be more suitable for larger or bulkier materials. The system's layout is also crucial, as it must minimize the number of transfer points and ensure smooth material flow to reduce energy consumption and wear on components.
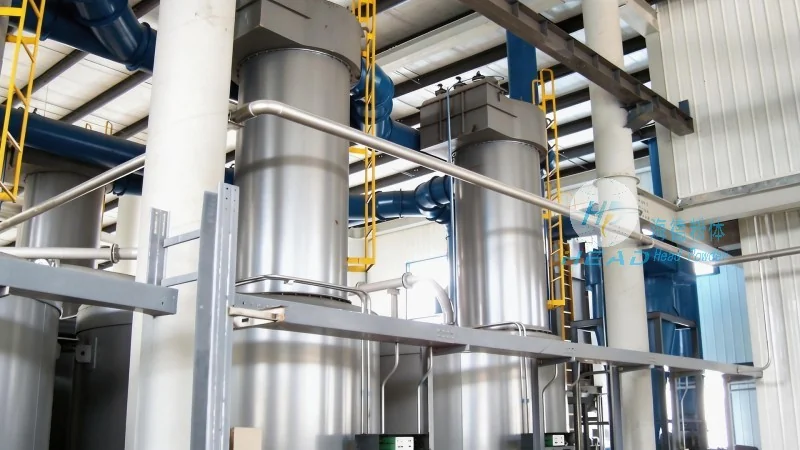
Another key principle is the integration of control systems that monitor and regulate the material flow. Modern systems often incorporate sensors and automation to detect blockages, adjust conveyor speeds, and maintain consistent material levels in storage silos. This not only improves operational efficiency but also enhances safety by preventing overfilling or underfilling of equipment. Additionally, the design must consider the environmental impact, such as dust control measures, to comply with regulations and protect the surrounding environment.
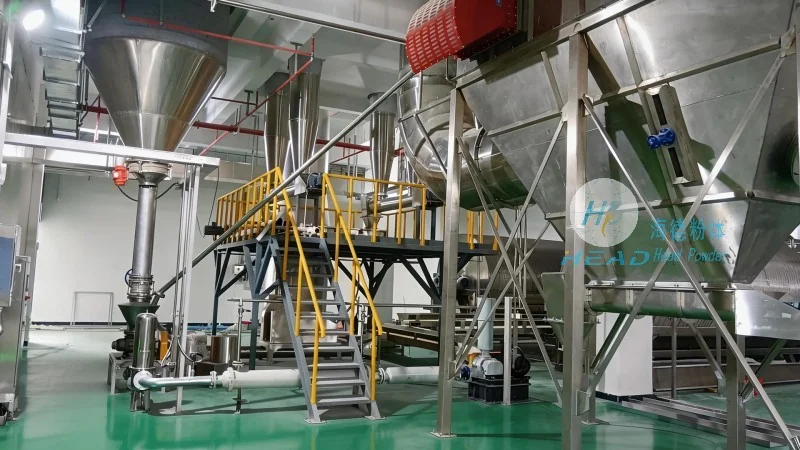
Role of Shandong HeadPowder Engineering Co., Ltd. in Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing coal and stone powder material handling systems tailored to the specific needs of industrial clients. With a strong focus on innovation and customer satisfaction, the company leverages advanced engineering techniques to develop systems that meet the highest standards of performance and reliability. HeadPowder's expertise lies in understanding the unique challenges of handling coal and stone powders, such as their abrasive nature and tendency to cause wear on equipment. By incorporating durable materials and robust design features, their systems ensure long-term operational efficiency and minimal maintenance costs.
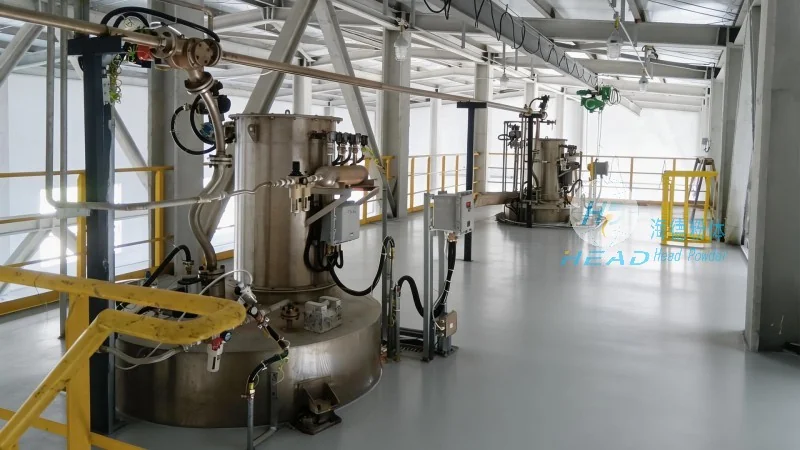
The company's headquarters is located in Shandong, China, where they maintain state-of-the-art manufacturing facilities and a team of experienced engineers dedicated to developing cutting-edge material handling solutions. HeadPowder's commitment to quality is evident in their adherence to international standards and rigorous testing protocols for all products. This ensures that their coal and stone powder material handling systems are not only effective but also safe and environmentally friendly, aligning with the evolving demands of the industry.
Conclusion: The Importance of Well-Designed Material Handling Systems
In conclusion, coal and stone powder material handling systems are indispensable in modern industrial operations, and their design plays a pivotal role in the overall efficiency and success of material transport processes. By adhering to key principles such as material-specific equipment selection, optimized system layout, and advanced control technologies, these systems can achieve high levels of performance and reliability. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in delivering tailored solutions that address the unique challenges of handling coal and stone powders, contributing to the sustainable and efficient operation of industrial facilities worldwide.