

What is a Positive Pressure Dilute Phase Pneumatic Conveying System? And What Are Its Design Princip
For industrial operations dealing with bulk materials, efficient and reliable material handling is crucial. One of the advanced solutions in this field is the positive pressure dilute phase pneumatic conveying system. This technology offers a flexible and effective method for transporting powders and granules over long distances, ensuring minimal product degradation and operational efficiency. In this article, we will explore what this system entails and delve into its core design principles.
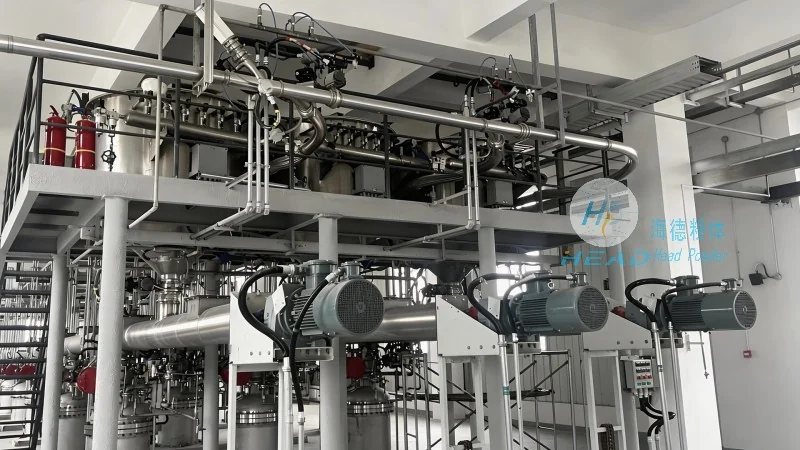
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of such systems. With a strong presence in China, particularly in Shandong, the company leverages years of expertise to deliver customized solutions tailored to various industrial needs. The following sections will provide a comprehensive overview of the system's functionality and design considerations.
Understanding the Positive Pressure Dilute Phase Pneumatic Conveying System
A positive pressure dilute phase pneumatic conveying system operates by using compressed air to transport particulate materials. Unlike negative pressure systems, which draw material into a vacuum, positive pressure systems push material through a sealed pipeline using high-pressure air. This approach ensures that the material remains in a suspended state, reducing the risk of blockages and ensuring consistent flow rates. The system typically consists of several key components, including a material feeder, a positive displacement blower or compressor, a pipeline network, and a discharge unit.
The material feeder is responsible for introducing the bulk material into the system. It can be a hopper or a rotary valve, depending on the material's characteristics and the required flow rate. The feeder ensures a steady supply of material, preventing any interruptions in the conveying process. The positive displacement blower or compressor then generates the necessary pressure to move the material through the pipeline. These devices are designed to handle high volumes of air while maintaining the required pressure levels, ensuring efficient material transport.
Core Design Principles of the System
The design of a positive pressure dilute phase pneumatic conveying system is governed by several critical principles that ensure optimal performance and reliability. One of the primary considerations is the selection of the appropriate air velocity. The air velocity must be high enough to keep the material suspended in the air stream but low enough to prevent excessive wear on the pipeline and components. This balance is crucial for maintaining the system's efficiency and longevity.
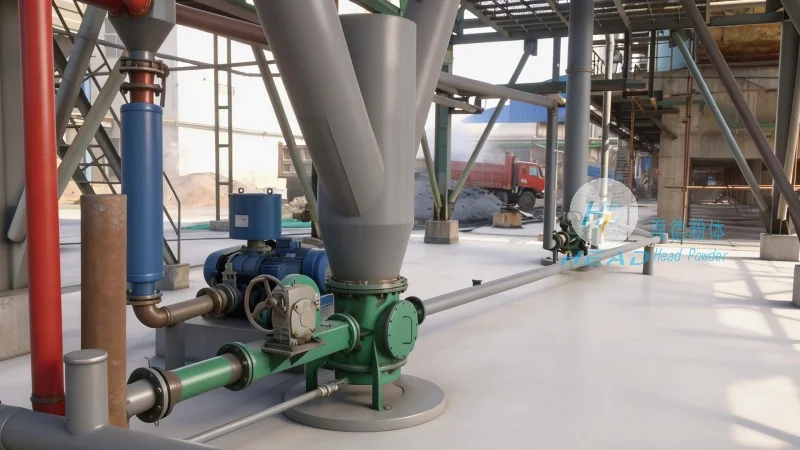
Another key design principle is the sizing of the pipeline. The diameter of the pipeline is determined by the material's properties, such as particle size, density, and flowability. Larger particles require larger diameters to prevent blockages and ensure smooth flow. The pipeline is also designed with smooth, rounded bends and transitions to minimize pressure losses and maintain consistent air velocity. Proper insulation and sealing are also essential to prevent air leakage and maintain the system's pressure.
The system's control and monitoring mechanisms are also integral to its design. Modern systems often incorporate sensors and control panels to monitor pressure, flow rate, and material level. These features allow for real-time adjustments, ensuring the system operates within optimal parameters. Additionally, the design considers the material's specific characteristics, such as moisture content and abrasiveness, to select appropriate materials for the components, such as stainless steel or special alloys, to withstand the material's effects and prolong the system's lifespan.
Advantages and Applications
Positive pressure dilute phase pneumatic conveying systems offer several advantages over traditional material handling methods. These include reduced product contamination, as the material is transported in a closed system, and lower labor costs due to automated operation. The system is also versatile, capable of handling a wide range of materials, from fine powders to granules, and can transport materials over long distances with minimal maintenance.
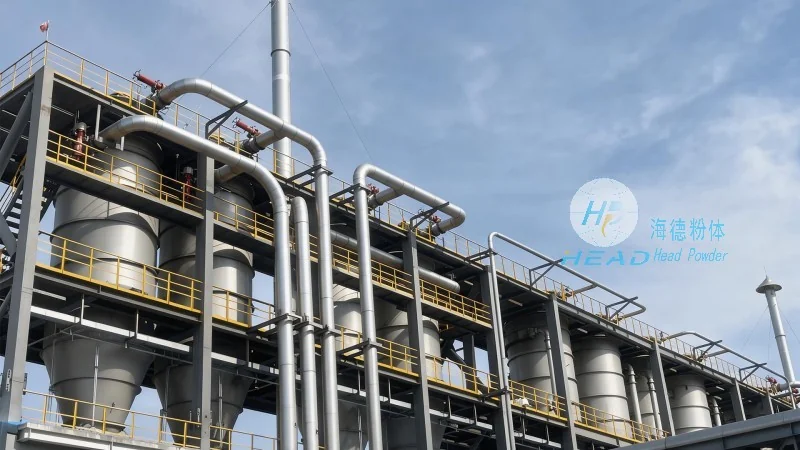
Applications of this technology span various industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for example, the system is used to transport sensitive powders while maintaining sterile conditions. In the food industry, it ensures that products are handled hygienically and without cross-contamination. The chemical industry utilizes these systems for transporting abrasive materials, while the mining sector employs them for transporting bulk ores and minerals.
Customization and Implementation by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized positive pressure dilute phase pneumatic conveying systems tailored to the specific needs of each client. The company's team of engineers works closely with clients to understand their operational requirements, material characteristics, and budget constraints. Through detailed analysis and design, the company develops solutions that maximize efficiency and minimize operational costs.
The implementation process begins with a thorough site assessment and material analysis. Engineers then design a system that meets the client's specifications, including the selection of components, pipeline layout, and control systems. The company's expertise in material handling and pneumatic conveying ensures that the final system is robust, reliable, and meets all safety and regulatory standards. With a strong commitment to quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. has become a trusted partner for businesses seeking advanced material handling solutions.
By leveraging the positive pressure dilute phase pneumatic conveying system, industries can enhance their operational efficiency, reduce costs, and improve product quality. The system's design principles, combined with the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., ensure that bulk material transport is handled with precision and reliability. As industrial demands continue to evolve, such advanced systems will play an increasingly vital role in maintaining competitiveness and operational excellence.