

What is a Gravel Material Conveyor Line? Understanding Its Design Principles
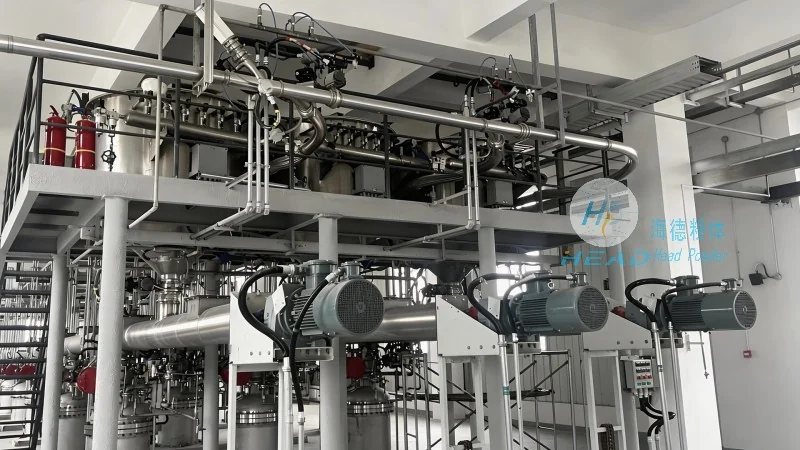
Gravel material conveyor lines are essential industrial systems engineered to transport loose bulk materials, such as gravel, sand, and crushed stones, with precision and efficiency. These systems are widely utilized across various sectors, including construction, mining, and material processing, to streamline material handling operations and enhance productivity. The design of a gravel conveyor line involves a comprehensive approach that integrates mechanical, structural, and operational considerations to ensure optimal performance under diverse working conditions.
Introduction to Gravel Material Conveyor Lines
A gravel material conveyor line typically consists of a continuous belt or chain that moves material from a loading point to a discharge point. The primary function of these systems is to automate the movement of bulk materials, reducing manual labor and minimizing the risk of material loss or spillage. By leveraging gravity or mechanical power, conveyor lines can transport materials over horizontal, inclined, or even vertical distances, making them versatile solutions for different industrial applications. The efficiency of a gravel conveyor line is directly influenced by its design, which must account for factors like material characteristics, throughput requirements, and operational environment.
Key Design Principles for Efficient Material Handling
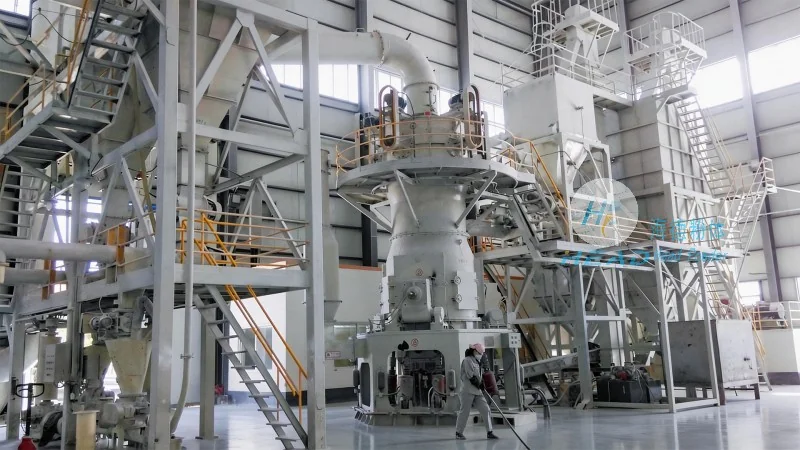
The design of a gravel material conveyor line is guided by several critical principles aimed at maximizing performance and durability. One of the fundamental principles is the selection of appropriate conveyor components, such as the type of belt (e.g., rubber or PVC) and the material of the rollers, which must withstand the abrasive nature of gravel and other bulk materials. The system's capacity is determined by the belt speed, width, and the angle of inclination, ensuring that the conveyor can handle the desired volume of material without overloading or causing material degradation. Additionally, the structural design must consider the weight of the materials and the operational loads, incorporating robust frames and supports to prevent deformation or failure under heavy usage.
Components and Functional Aspects
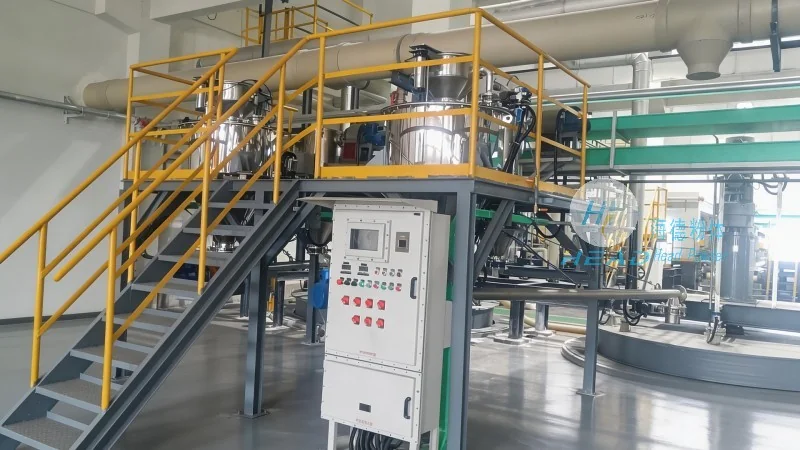
A gravel material conveyor line comprises several key components that work in tandem to achieve efficient material transport. The conveyor belt, often made of durable rubber or synthetic materials, is the core element that carries the gravel. It is supported by a series of rollers, including drive rollers and idler rollers, which reduce friction and maintain the belt's tension. The drive system, typically powered by electric motors, provides the necessary force to move the belt and the material. Control mechanisms, such as variable speed drives and safety sensors, ensure that the conveyor operates smoothly and safely, preventing accidents and downtime. Additionally, the system may include features like belt cleaners and material feeders to maintain consistent material flow and prevent blockages.
Application Scenarios and Industry Use Cases
Gravel material conveyor lines are widely applied in various industries to facilitate the movement of bulk materials. In the construction industry, they are used to transport gravel and sand from stockpiles to construction sites, ensuring a steady supply of materials for concrete mixing and road laying. In mining operations, these systems are employed to move crushed stones and ore from processing plants to storage areas or for further processing. The mining sector also utilizes conveyor lines for transporting tailings and waste materials, optimizing the overall mining process. Furthermore, in material processing plants, gravel conveyor lines help in the sorting and distribution of different grades of gravel, enabling efficient production and quality control. The adaptability of these systems makes them suitable for both large-scale industrial operations and smaller-scale projects, providing a reliable solution for material handling needs.
About HeadPowder Engineering Co., Ltd.
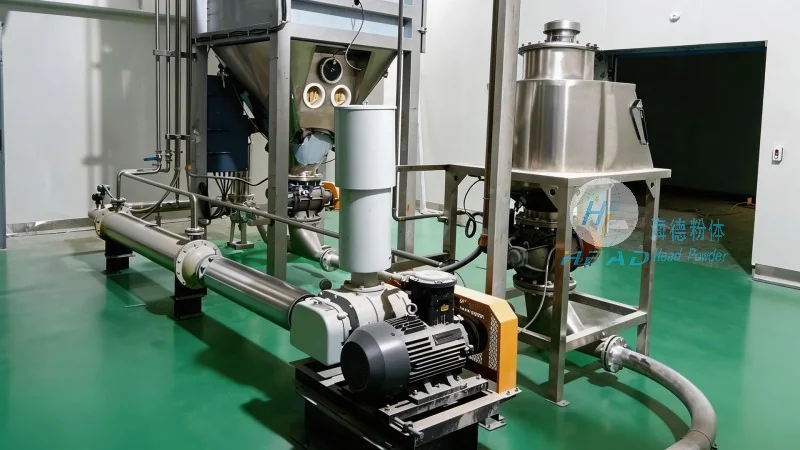
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and supply of high-quality gravel material conveyor lines. With a commitment to innovation and precision engineering, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder's conveyor systems are engineered to meet the specific requirements of clients, ensuring durability, efficiency, and safety in diverse operational environments. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled expertise to deliver superior products and services to its global clientele. By adhering to rigorous quality standards and customer-centric approaches, HeadPowder continues to excel in providing reliable and effective solutions for material handling challenges.