

Working Principle and Features of Intelligent Tonne Bag Feeding Station for Powder Material Handling
The intelligent tonne bag feeding station is a specialized system designed for efficient and automated handling of bulk powder materials from tonne bags. This equipment is widely used in various industries such as chemical, food, pharmaceutical, and mining, where precise and reliable material transfer is crucial. The system integrates advanced technology to streamline the process of opening, emptying, and transporting powder from large bags into processing lines or storage systems.
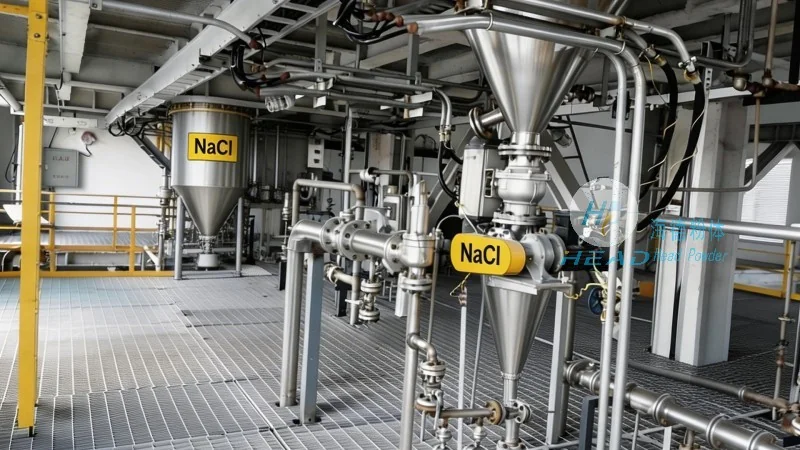
Working Principle of the Intelligent Tonne Bag Feeding Station
The core working principle of the intelligent tonne bag feeding station involves several key steps that ensure seamless operation. First, the tonne bag is positioned on a designated platform or pallet. The system then uses a combination of mechanical and pneumatic components to open the bag's top, typically by cutting or tearing the bag's opening. Once the bag is opened, the powder is discharged into a hopper or collection bin. The system may employ a vacuum or pressure-assisted mechanism to facilitate the flow of powder from the bag into the hopper. Subsequently, the powder is transferred to the downstream processing equipment through a conveyor system or pneumatic conveying line. The entire process is controlled by a programmable logic controller (PLC) or a similar control system, which coordinates the movement of the bag, the opening mechanism, and the material transfer components. This automation ensures consistent performance and reduces the risk of human error or material loss.
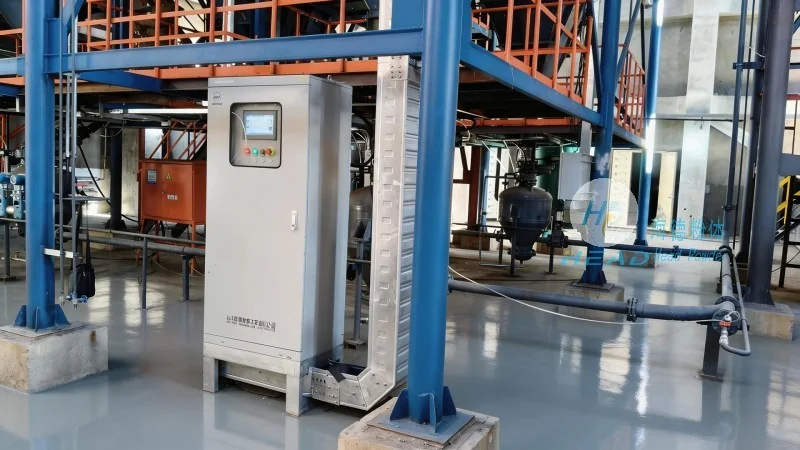
Key Features of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station offers several distinct features that enhance its functionality and usability. One of the primary features is its high degree of automation, which minimizes the need for manual intervention during the feeding process. This not only improves operational efficiency but also enhances safety by reducing the exposure of personnel to dust and potential hazards. Another notable feature is the system's ability to handle a wide range of powder materials, including those with varying bulk densities, flow properties, and moisture content. The adjustable parameters, such as the opening speed, discharge rate, and conveyor speed, allow for customization to suit different material characteristics. Additionally, the station is equipped with sensors and monitoring systems that provide real-time feedback on the material level, bag status, and operational parameters. These features enable proactive maintenance and troubleshooting, ensuring optimal performance and minimizing downtime. The design also incorporates dust collection and filtration systems to maintain a clean and safe working environment, which is essential for industries where air quality and compliance with regulations are critical.
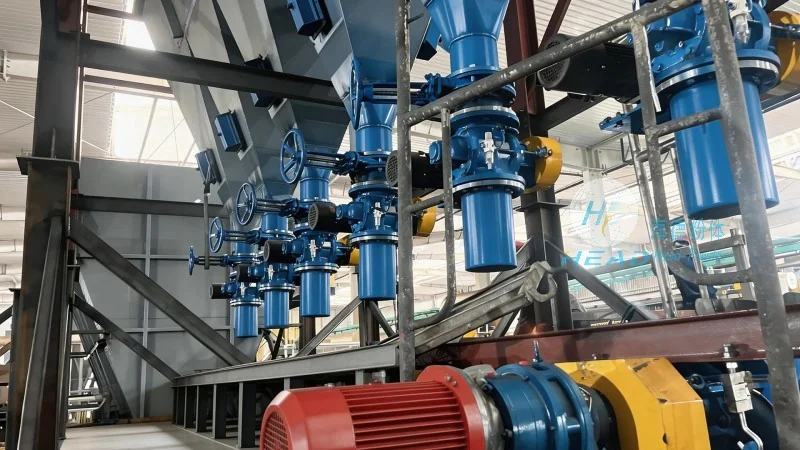
Benefits of Using the Intelligent Tonne Bag Feeding Station
Implementing an intelligent tonne bag feeding station brings numerous benefits to industrial operations. Firstly, it significantly improves the efficiency of material handling by automating the process from bag opening to material transfer. This reduces the time required for each batch, allowing for higher throughput and increased productivity. Secondly, the system enhances safety by minimizing the need for manual handling of heavy bags and reducing exposure to airborne dust, which can cause respiratory issues or other health problems. Thirdly, the automation reduces labor costs and the risk of human error, leading to more consistent and reliable material transfer. The system also helps in maintaining a clean and organized workspace, as the dust collection systems prevent the accumulation of powder in the environment. Furthermore, the adjustable and customizable features allow the station to adapt to different production requirements, making it a versatile solution for various applications. The integration of advanced control systems ensures that the operation is precise and repeatable, which is crucial for maintaining product quality and consistency.
Application Examples and Industry Use Cases
The intelligent tonne bag feeding station is applicable in a wide range of industries where bulk powder handling is essential. In the chemical industry, it is used for handling raw materials such as powders, granules, and additives, which are then processed into finished products. In the food and pharmaceutical industries, the system is employed to handle ingredients like flour, sugar, and active pharmaceutical ingredients (APIs), ensuring that the materials are transferred hygienically and in compliance with regulatory standards. The mining industry also utilizes this equipment for handling ore powders and other minerals, which are then processed for extraction and refinement. Additionally, in the agricultural sector, the station can be used for handling fertilizers and other agricultural chemicals, facilitating their distribution to farms and processing facilities. Each of these applications benefits from the system's ability to handle large quantities of material efficiently and safely, while maintaining the quality and integrity of the product.
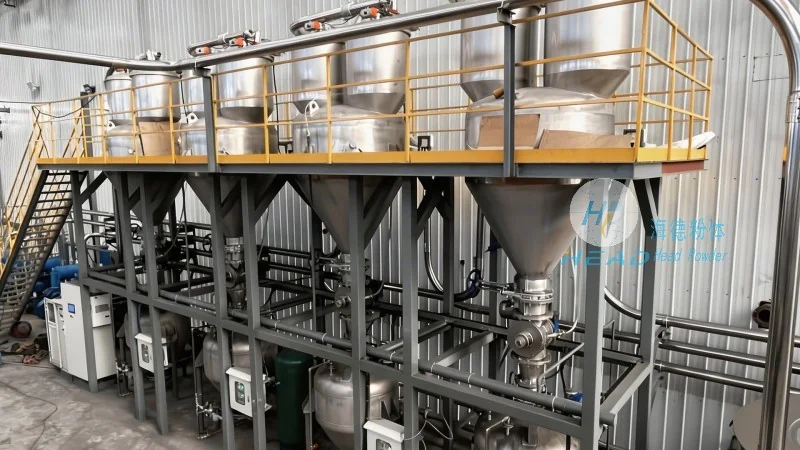
Conclusion and Company Information
The intelligent tonne bag feeding station represents a significant advancement in bulk powder handling technology, offering a combination of efficiency, safety, and reliability. By automating the process of opening, emptying, and transporting powder from tonne bags, the system streamlines industrial operations and enhances overall productivity. The key features, such as automation, adaptability, and real-time monitoring, make it a valuable asset for various industries. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such advanced systems, ensuring that clients receive high-quality equipment tailored to their specific needs. With a commitment to innovation and customer satisfaction, HeadPowder continues to deliver solutions that meet the evolving demands of the industrial sector. The company's headquarters is located in Shandong, China, where it leverages its expertise and resources to develop cutting-edge material handling solutions for global markets.