

Working Principle and Features of Lithium Fluoride Powder Handling Systems
This article provides an in-depth exploration of the working principles and key features of lithium fluoride powder handling systems, a critical component in industrial applications where precise and efficient material transport is essential. The system is designed to handle the unique properties of lithium fluoride, a highly reactive and hygroscopic powder, ensuring safe and reliable operation in various processing environments.
Working Principle of the Powder Handling System
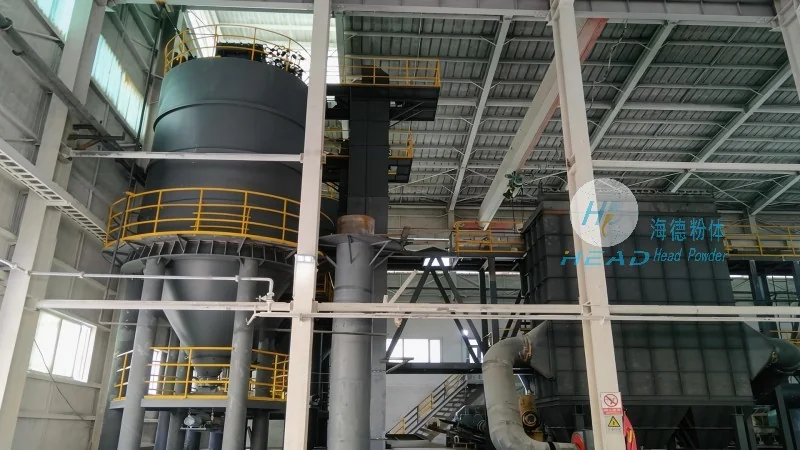
The lithium fluoride powder handling system operates on a closed-loop mechanism that minimizes exposure to external contaminants and maintains the purity of the material. The process begins with the storage of lithium fluoride in a sealed hopper, which is equipped with a level indicator and a discharge valve. When the system is activated, the powder is drawn from the hopper by a positive displacement pump or a rotary valve, depending on the system configuration. The material is then conveyed through a series of flexible or rigid pipes, often using air-assisted or mechanical methods to ensure consistent flow. The system incorporates a filtration stage to remove any fines or agglomerates, preventing blockages in downstream equipment. The discharge end of the system is connected to the processing unit, where the powder is metered and used as required. The entire process is controlled by a programmable logic controller (PLC), which monitors parameters such as pressure, flow rate, and temperature to maintain optimal performance. This closed-loop design not only enhances efficiency but also ensures compliance with safety and environmental regulations.
Key Features of the Lithium Fluoride Powder Handling System
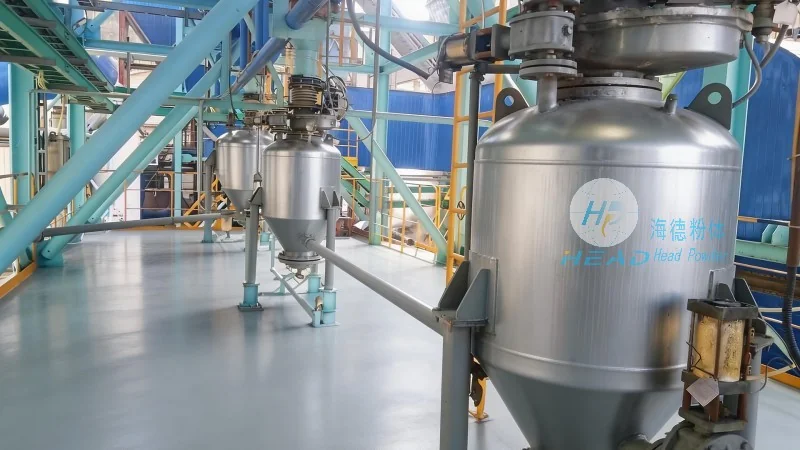
Shandong HeadPowder Engineering Co., Ltd. has developed a comprehensive range of features that distinguish their lithium fluoride powder handling systems from conventional solutions. One of the primary features is the integration of a dust suppression system, which uses a combination of air and water to control airborne particles, reducing the risk of inhalation and environmental contamination. The system also includes a temperature control module, which maintains the powder at a consistent temperature to prevent caking or degradation, especially important for lithium fluoride's hygroscopic nature. Additionally, the design incorporates a material recovery system, which recovers any spilled or excess powder, minimizing waste and improving operational efficiency. The system is constructed from corrosion-resistant materials, such as stainless steel and PTFE, to withstand the chemical properties of lithium fluoride and ensure long-term durability. Another notable feature is the user-friendly interface, which allows operators to monitor and adjust system parameters in real-time, enhancing control and reducing downtime. The system also complies with international safety standards, including ATEX certification for hazardous environments, ensuring safe operation in industrial settings.
Benefits of Using a Specialized Powder Handling System for Lithium Fluoride
Implementing a specialized powder handling system for lithium fluoride offers numerous benefits to industrial operations. Firstly, it significantly improves material handling efficiency by reducing the time and labor required for manual handling, which is both costly and hazardous. The automated system ensures consistent flow rates and accurate dosing, leading to improved product quality and reduced waste. Secondly, the closed-loop design minimizes material exposure to moisture and air, preserving the chemical integrity of lithium fluoride and preventing degradation that could affect its performance in downstream applications. This is particularly critical in industries such as battery manufacturing, where the purity of lithium fluoride directly impacts the efficiency and lifespan of lithium-ion batteries. Thirdly, the system enhances workplace safety by eliminating the need for manual handling of powders, reducing the risk of respiratory issues and other health hazards associated with inhalation of fine particles. The dust suppression and filtration features further contribute to a safer working environment, complying with occupational health and safety regulations. Finally, the system's durability and low maintenance requirements result in long-term cost savings, as it reduces the frequency of equipment replacement and repair.
Conclusion
In conclusion, the lithium fluoride powder handling system developed by Shandong HeadPowder Engineering Co., Ltd. combines advanced technology with robust design to address the unique challenges of handling lithium fluoride. The system's working principle, centered on a closed-loop mechanism with precise control, ensures efficient and safe material transport. The key features, including dust suppression, temperature control, and material recovery, enhance performance and safety while maintaining material purity. The benefits of using such a specialized system extend beyond operational efficiency to include improved product quality, workplace safety, and long-term cost savings. For industries relying on lithium fluoride in their processes, investing in a high-quality powder handling system is essential to optimize performance and ensure compliance with industry standards. Shandong HeadPowder Engineering Co., Ltd. continues to lead in providing tailored solutions that meet the evolving needs of the lithium fluoride handling industry.