

The Working Principle and Features of a Bin Pump Powder Conveyor
Bin pump powder conveyors are essential equipment in the powder handling industry, designed to transport bulk materials efficiently and reliably. Understanding their working principle and key features is crucial for selecting the right equipment for specific industrial applications. This article provides an in-depth look at the operational mechanics and characteristics of bin pump powder conveyors, highlighting how they enhance material handling processes.
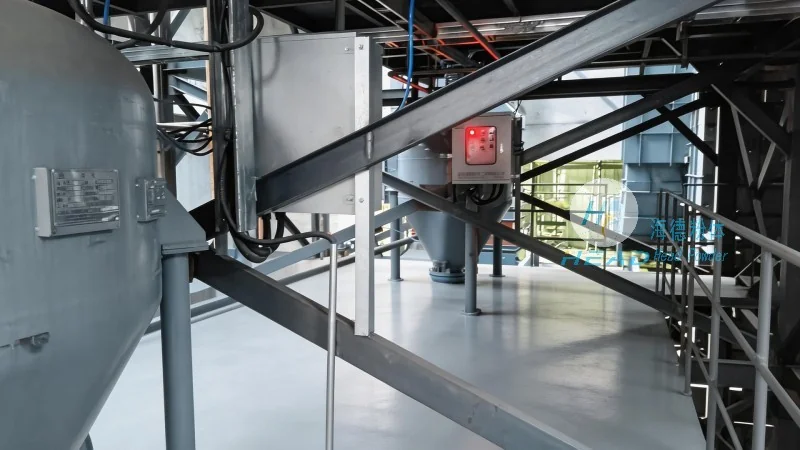
The Working Principle of a Bin Pump Powder Conveyor
A bin pump powder conveyor operates by using a pressure vessel, commonly known as a bin pump, to store and transport bulk materials. The process typically involves several key steps. First, the material is fed into the bin pump from a hopper or storage silo. Once the bin pump is filled, it is sealed and pressurized using a compressed air or nitrogen system. This pressurization creates a high-pressure environment inside the pump, which then forces the material through a pipeline to the discharge point. The bin pump can be operated in a cyclic manner, where it fills, pressurizes, and discharges material in a controlled sequence. This cycle ensures consistent and continuous material flow, even over long distances or with varying material characteristics. The system is equipped with sensors and control valves to regulate the pressure and flow rate, ensuring safe and efficient operation. The entire process is automated, allowing for precise control and minimal human intervention, which enhances operational efficiency and reduces the risk of material spillage or equipment damage.

Key Features of a Bin Pump Powder Conveyor
Bin pump powder conveyors offer several advantages that make them suitable for a wide range of industrial applications. One of the primary features is their ability to handle a variety of bulk materials, including powders, granules, and fine particles, with minimal degradation or segregation. The enclosed system prevents material contamination and dust emissions, making it ideal for applications requiring high purity and environmental compliance. Another significant feature is the high pressure operation, which allows for long-distance transport (up to several kilometers) and vertical or horizontal material movement without the need for additional equipment like conveyor belts or screw conveyors. The system is also highly flexible, as it can be easily reconfigured to accommodate different material types or process requirements. Additionally, bin pump conveyors are known for their low maintenance requirements and long service life, reducing operational costs over time. The automated control system ensures consistent performance and reduces the need for manual adjustments, which improves overall productivity. Furthermore, the equipment is designed with safety features such as pressure relief valves and emergency shut-off mechanisms, ensuring safe operation in industrial settings. These features collectively make bin pump powder conveyors a reliable and efficient solution for bulk material handling in various industries.
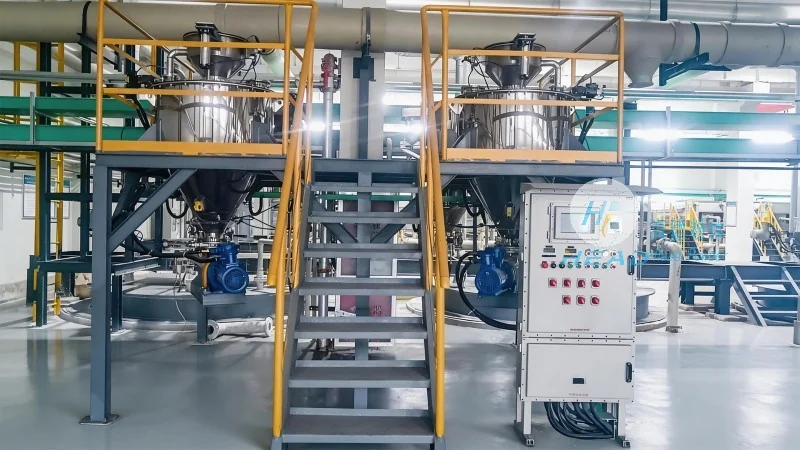
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling equipment. With a strong focus on innovation and quality, the company specializes in designing and manufacturing bin pump powder conveyors and other related systems. HeadPowder is committed to providing reliable and efficient solutions for material handling challenges, ensuring that their products meet the highest industry standards. The company's headquarters is located in Shandong, China, where they leverage local expertise and resources to develop cutting-edge technology in the powder handling sector. Their products are widely used in industries such as pharmaceuticals, food processing, chemicals, and mining, where precise and safe material transport is critical. HeadPowder's dedication to customer satisfaction and technological advancement has established them as a trusted partner in the global powder handling market.