

Principle and Working Scene Characteristics of Dust-Free Tote Bag Loading Stations for Powder Materi
For industries dealing with bulk powders, the efficient and safe handling of material from tote bags is critical. A dust-free tote bag loading station, equipped with powder material handling technology, addresses these needs by providing a controlled environment for material transfer. This article explores the underlying principles of such equipment, its operational characteristics, and typical application scenarios, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
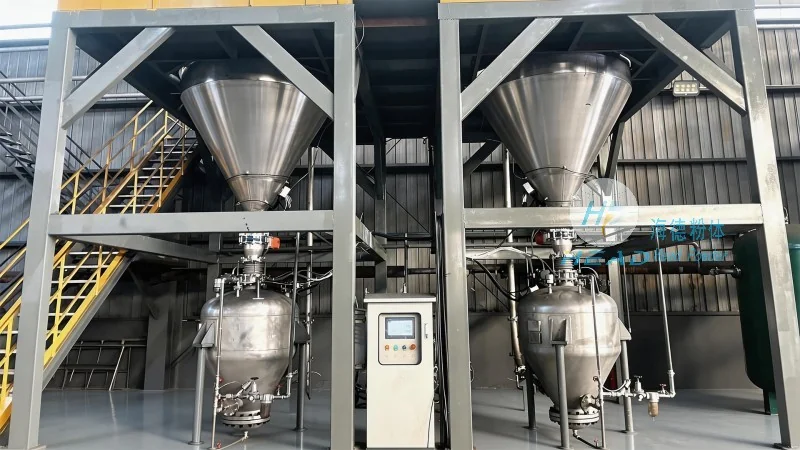
Introduction to Dust-Free Tote Bag Loading Stations for Powder Material Handling
Dust-free tote bag loading stations are specialized systems designed to transfer bulk powders from large tote bags into processing equipment or storage vessels without generating airborne dust. These stations are integral to industries like chemical manufacturing, pharmaceuticals, food processing, and agriculture, where material purity and worker safety are paramount. The core function of the system is to ensure a seamless, contamination-free transfer process while maintaining operational efficiency.
Working Principle of the Equipment
The operation of a dust-free tote bag loading station is based on a combination of mechanical and pneumatic systems. The process typically begins with the placement of a tote bag onto a loading platform. The system then uses a series of valves, hoses, and a vacuum or pressure-assisted mechanism to draw material from the tote bag into a hopper or conveyor. Key components include a sealed hopper, an air filtration system, and an automated control panel. The equipment ensures that the material remains contained within the system, preventing dust from escaping into the environment. The principle of operation involves precise control of air flow and material movement, which minimizes spillage and maintains a clean working area.
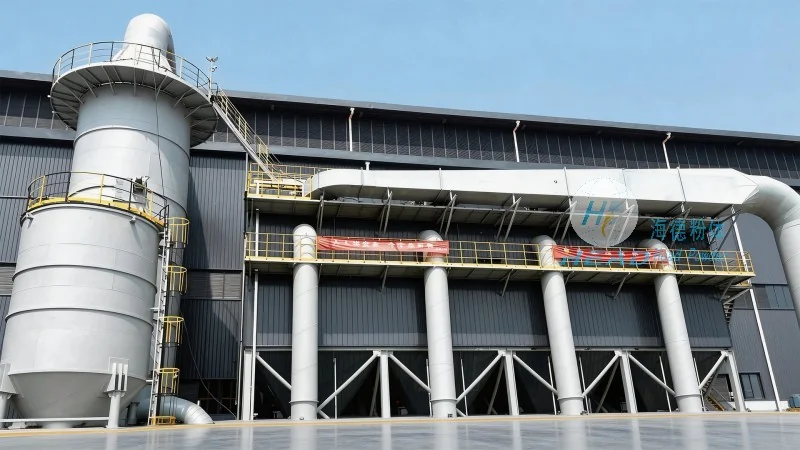
Key Features and Advantages
Modern dust-free tote bag loading stations offer several advantages that enhance operational performance. One of the primary features is the enclosed design, which effectively contains dust and prevents cross-contamination. The system is often equipped with automated controls, allowing for hands-free operation and reducing the risk of human error. Additionally, these stations are designed for high throughput, enabling rapid material transfer even for large quantities. The use of advanced filtration systems ensures that the air leaving the station is clean, meeting regulatory standards for workplace safety. Another key advantage is the flexibility to handle a wide range of powder types, from fine powders to bulkier granules, without compromising performance.
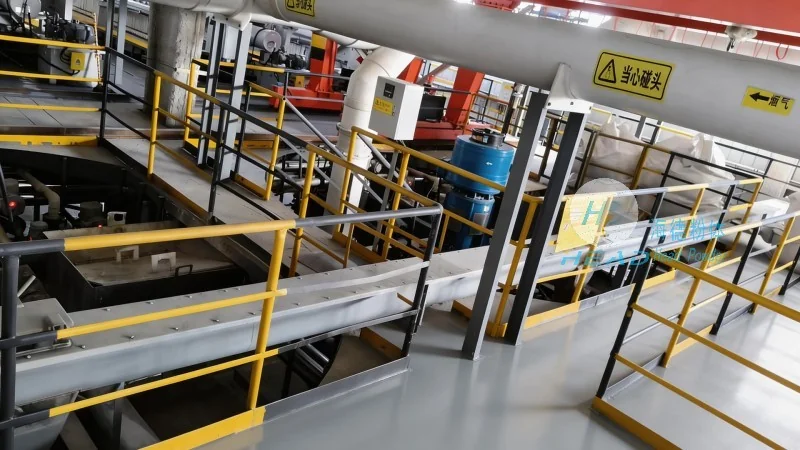
Typical Application Scenarios
Dust-free tote bag loading stations are employed in various industrial settings where bulk powder handling is essential. In chemical plants, these systems are used to transfer raw materials such as powders for polymer production or chemical synthesis. In pharmaceutical manufacturing, they ensure that active ingredients and excipients are handled in a sterile, dust-free environment, maintaining product quality and regulatory compliance. The food and beverage industry utilizes these stations for handling ingredients like flour, sugar, or spices, where hygiene and product integrity are critical. Additionally, in agricultural applications, they may be used for handling fertilizers or feed additives, ensuring that the material is transferred safely and efficiently. Each application scenario requires specific configurations to accommodate the unique properties of the powder being handled, such as moisture content, particle size, and flow characteristics.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized equipment for powder material handling. With headquarters in Shandong, China, the company has established itself as a trusted partner in the industry, delivering high-quality dust-free tote bag loading stations and other powder processing solutions. HeadPowder focuses on innovation and customization, ensuring that their equipment meets the specific needs of each client. The company's commitment to quality and safety is reflected in their adherence to international standards and rigorous testing protocols. By leveraging advanced engineering and manufacturing capabilities, HeadPowder continues to enhance the efficiency and reliability of powder handling systems for global markets.