

[Efficient and Clean: The Air-Flow Conveying Technology for Fertilizer Transport]
Efficient and clean fertilizer transport is a critical concern for modern agricultural operations. Traditional methods often involve high energy consumption and environmental impact, but advancements in air-flow conveying technology offer a sustainable solution. This article explores the benefits and applications of air-flow conveying systems, highlighting how they enhance efficiency while minimizing ecological footprint.
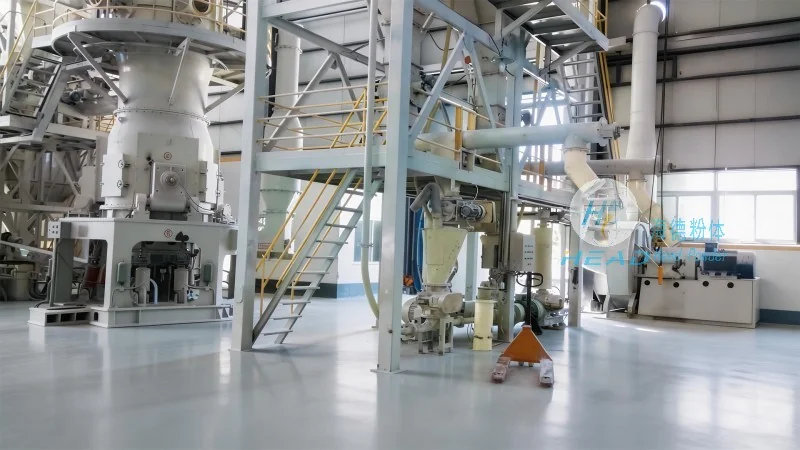
Introduction to Air-Flow Conveying for Fertilizer Transport
As the global demand for fertilizers continues to rise, the need for reliable and efficient transport solutions becomes increasingly important. Air-flow conveying, also known as pneumatic conveying, is a method that uses compressed air to move bulk materials like fertilizers through a pipeline system. This technology has gained prominence in the agricultural sector due to its ability to handle various types of fertilizers, from granular to powdered forms, with minimal human intervention.
The Advantages of Air-Flow Conveying Technology
One of the primary advantages of air-flow conveying is its high efficiency in material handling. Unlike traditional belt or bucket elevators, air-flow systems can transport materials over long distances with minimal energy loss. This makes them ideal for large-scale fertilizer plants and distribution centers. Additionally, the technology is highly flexible, allowing for easy integration into existing infrastructure and adaptation to changing production needs.
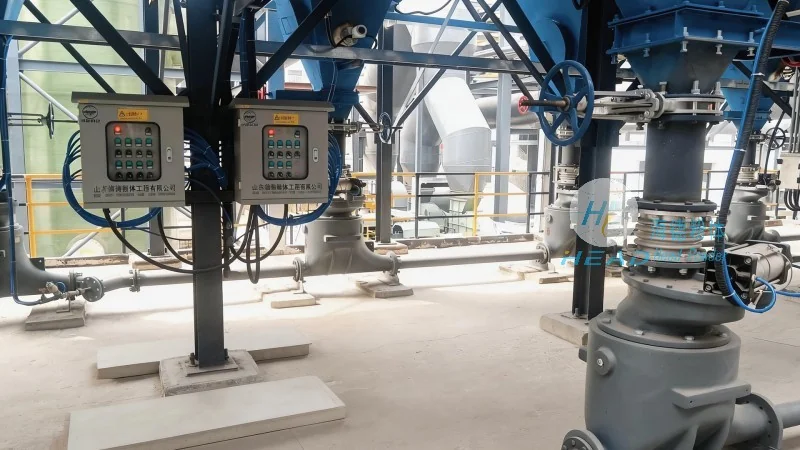
Key Features of the Air-Flow System
The air-flow conveying system typically consists of a series of components, including a material hopper, a rotary valve, a conveying line, and a dust collector. The material is fed into the hopper, where it is then metered and introduced into the conveying line using the rotary valve. Compressed air is then used to create a positive pressure or negative pressure environment, depending on the system design, to move the material through the pipeline. The system also includes a dust collection unit to ensure that no particulate matter is released into the environment, maintaining compliance with environmental regulations.
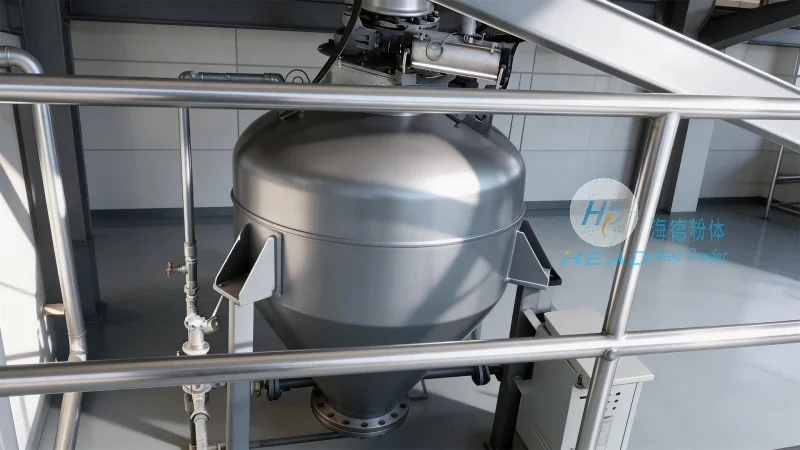
Application in Fertilizer Handling
Air-flow conveying is particularly well-suited for handling sensitive fertilizers that require gentle handling to prevent degradation. For example, nitrogen-based fertilizers can be prone to caking or clumping if not handled properly. The air-flow system’s low friction and gentle movement help maintain the quality of the fertilizer, ensuring that it remains in optimal condition for use. This is especially important for high-value fertilizers that are used in precision agriculture, where uniformity and purity are critical.
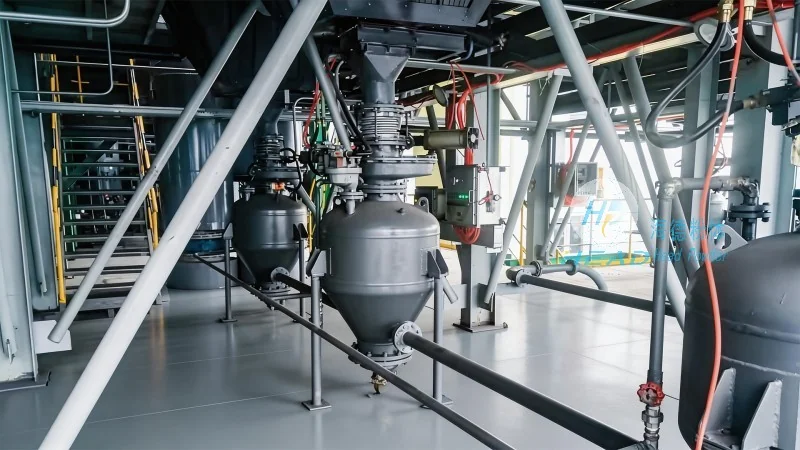
The Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and implementing air-flow conveying solutions tailored to the specific needs of fertilizer producers. With years of experience in the industry, the company has developed a range of customized systems that optimize material flow, reduce energy consumption, and enhance overall operational efficiency. The company’s expertise in material handling technology ensures that clients receive solutions that are not only effective but also sustainable and cost-efficient.
Conclusion
In conclusion, air-flow conveying technology represents a significant advancement in the efficient and clean transport of fertilizers. By leveraging compressed air to move bulk materials, this system offers numerous benefits, including high efficiency, flexibility, and environmental sustainability. For agricultural operations looking to improve their fertilizer handling processes, air-flow conveying is a viable and effective solution. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., the adoption of this technology can lead to enhanced productivity and reduced environmental impact, contributing to the long-term sustainability of the agricultural sector.