

Principle and Working Scene Characteristics of Heptahydrate Magnesium Sulfate Powder Handling Equipm
Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial applications. The efficient handling and transportation of this powder are crucial for maintaining production efficiency and product quality. This article explores the principle and working scene characteristics of specialized powder handling equipment designed for heptahydrate magnesium sulfate, highlighting the technical aspects and practical applications in industrial settings.
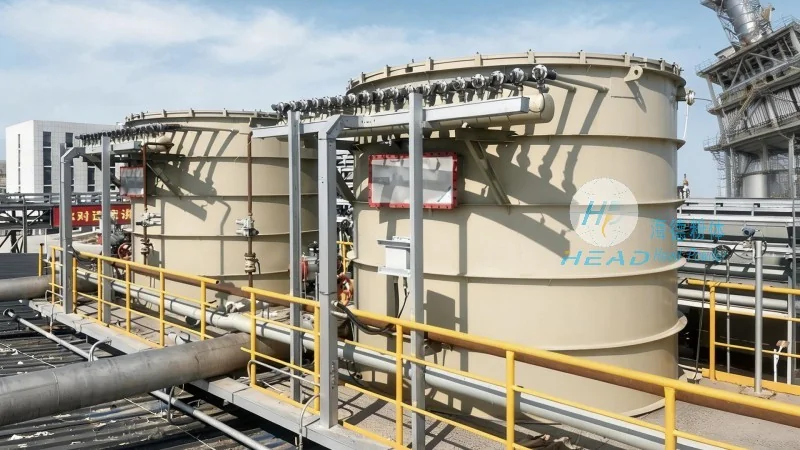
Introduction to Heptahydrate Magnesium Sulfate Powder Handling Equipment
Heptahydrate magnesium sulfate powder handling equipment is engineered to address the unique challenges associated with transporting fine powders like heptahydrate magnesium sulfate. These challenges include dust generation, caking, and the need for precise control over flow rates. The equipment is designed to ensure safe, efficient, and reliable operation in industrial environments, supporting processes such as material transfer, storage, and processing.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of the powder handling equipment discussed in this article, is a leading company in the field of powder processing technology. With a focus on innovation and quality, HeadPowder has established itself as a trusted provider of industrial equipment for various chemical and material handling applications. The company's headquarters is located in Shandong, China, where it leverages advanced engineering capabilities to develop cutting-edge solutions tailored to client needs.
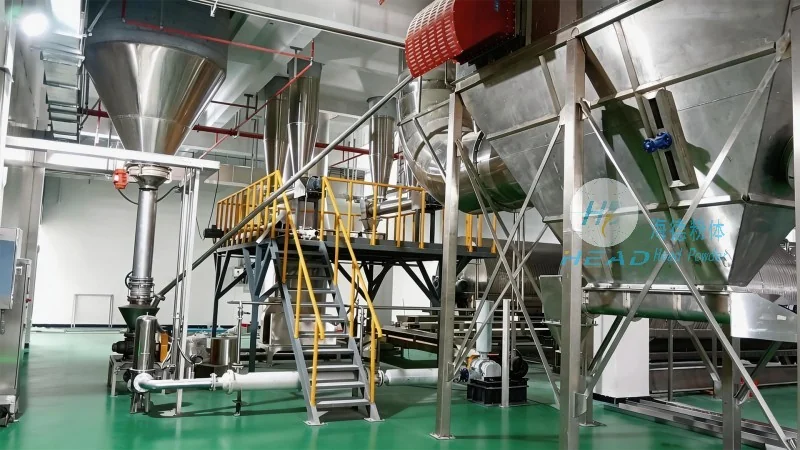
The Working Principle of the Powder Handling Equipment
The core principle of heptahydrate magnesium sulfate powder handling equipment involves the use of mechanical and pneumatic systems to move the powder from one location to another. Common mechanisms include screw conveyors, pneumatic conveying systems, and vacuum pumps. The equipment is typically equipped with features such as adjustable speed controls, material flow monitoring, and dust suppression systems to ensure optimal performance and safety. The design aims to minimize product degradation, prevent clogging, and maintain consistent flow rates, which are critical for maintaining product integrity and operational efficiency.
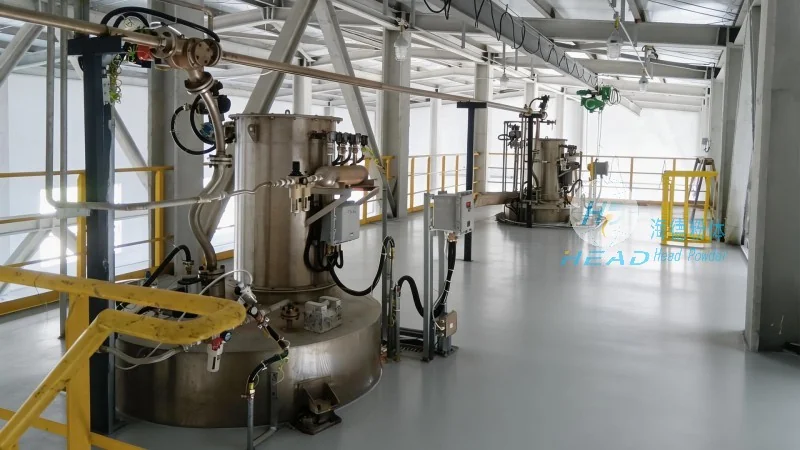
Key Working Scene Characteristics
The working scene characteristics of heptahydrate magnesium sulfate powder handling equipment are tailored to the specific demands of industrial applications. These characteristics include high throughput capacity, low maintenance requirements, and adaptability to different production scales. The equipment is often used in scenarios such as bulk material handling in chemical plants, pharmaceutical manufacturing, and food processing facilities. In these settings, the equipment's ability to handle fine powders without causing dust or caking is essential for maintaining a clean and safe working environment. Additionally, the equipment's design allows for integration with existing production lines, reducing downtime and enhancing overall operational efficiency.
Technical Advantages and Practical Applications
HeadPowder's powder handling equipment for heptahydrate magnesium sulfate offers several technical advantages that make it suitable for demanding industrial applications. These advantages include robust construction, corrosion-resistant materials, and advanced control systems that ensure precise operation. The equipment is designed to handle the specific properties of heptahydrate magnesium sulfate, such as its hygroscopic nature and tendency to cake under certain conditions. By addressing these challenges, the equipment ensures reliable performance and minimal product loss. Practical applications include the transportation of heptahydrate magnesium sulfate from storage silos to processing units, as well as its distribution to various end-use industries like agriculture, cosmetics, and healthcare.