

Principle and Working Scene Characteristics of Powder Bin Material Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. is a leading enterprise specializing in advanced powder processing technologies. The company focuses on developing and delivering high-performance material conveying systems, particularly the powder bin material conveying system, which is designed to efficiently handle bulk powders in various industrial applications. This system is engineered to ensure reliable, safe, and efficient material transport from storage bins to downstream processing equipment, catering to the diverse needs of sectors such as pharmaceuticals, food, and chemicals.
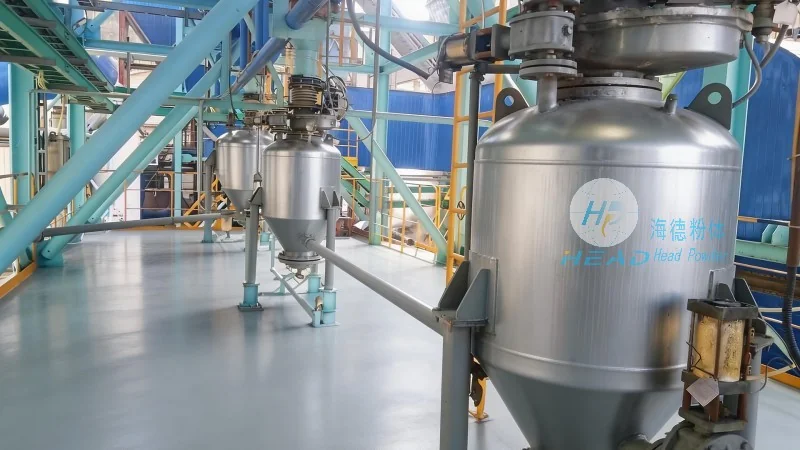
The Core Principles of the Powder Bin Material Conveying System
The powder bin material conveying system operates on a combination of mechanical and pneumatic principles, ensuring precise control over powder flow and handling. The system typically includes a storage bin, a conveying mechanism (e.g., screw conveyor or pneumatic duct), and an integrated control unit. The storage bin, constructed from durable materials like stainless steel or carbon steel, provides a secure environment for storing bulk powders, preventing contamination and ensuring stable material levels. The conveying mechanism is responsible for transporting the material from the bin to processing equipment, with options tailored to the specific properties of the powder, such as its density, moisture content, and flowability.
Pneumatic conveying, a common method in many systems, utilizes compressed air to move powders through a network of pipes. This approach offers advantages like low maintenance, the ability to handle abrasive or sensitive materials, and flexibility in transporting powders over long distances. The screw conveyor, another popular choice, employs rotating screws to push material forward, providing consistent flow rates, especially for cohesive or sticky powders. The selection of the conveying mechanism depends on factors like material characteristics, required throughput, and the layout of the processing facility.
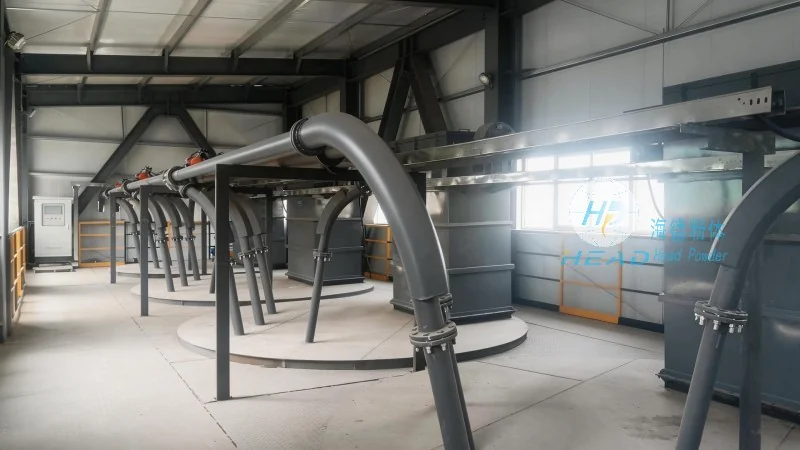
Control Systems and Automation in the Conveying Process
Modern powder bin material conveying systems are equipped with advanced control systems that enhance operational efficiency and safety. These systems utilize programmable logic controllers (PLCs) and human-machine interfaces (HMIs) to allow real-time monitoring and adjustment of parameters such as air pressure, flow rates, and material discharge. The control unit ensures precise regulation, preventing issues like blockages, overfilling, or underfilling. Additionally, sensors and feedback mechanisms are integrated to detect changes in material level, pressure, or temperature, enabling automated responses to maintain system stability and safety.
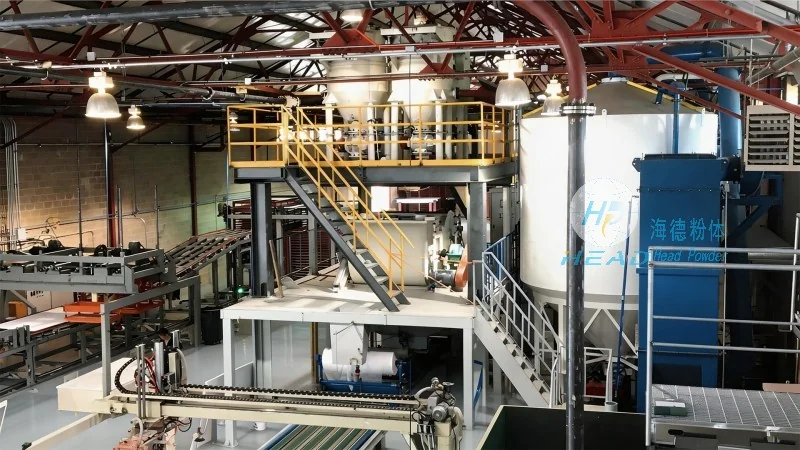
Working Scene Characteristics and Industry Applications
The working scene characteristics of the powder bin material conveying system are tailored to meet the specific demands of different industrial environments. In pharmaceutical manufacturing, the system adheres to stringent hygiene and contamination control standards. It features sealed components, easy-to-clean surfaces, and validated cleaning procedures to comply with regulatory requirements. In the food industry, the system incorporates food-grade materials and sanitary design to prevent cross-contamination and maintain product quality. For chemical processing, the system is engineered to handle corrosive or hazardous materials, with robust construction and safety features to protect personnel and equipment.
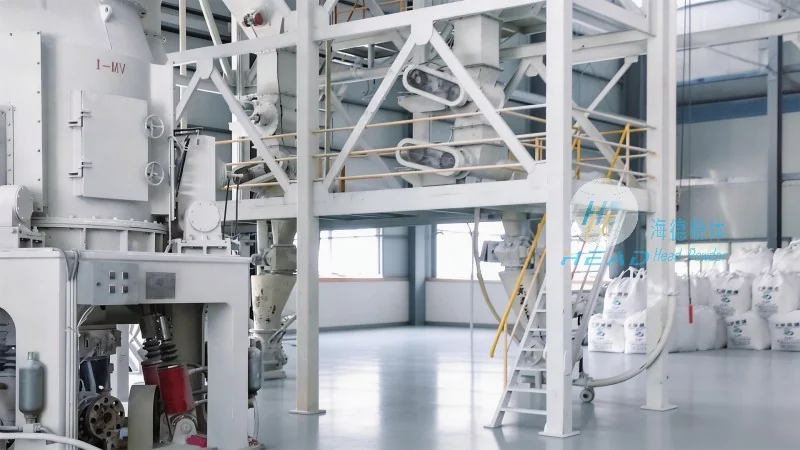
Another key characteristic is the system's adaptability to varying production scales and operational conditions. Whether used in small-scale laboratory settings or large-scale industrial plants, the system can be customized to meet specific throughput requirements. The modular design allows for easy expansion or reconfiguration as production needs evolve, providing long-term value and flexibility. This adaptability is further enhanced by the integration of advanced monitoring and analytics tools, which enable predictive maintenance and performance optimization over time.
Conclusion: Reliability and Innovation in Bulk Powder Handling
Shandong HeadPowder Engineering Co., Ltd.'s powder bin material conveying system represents a sophisticated solution for efficient bulk powder handling. By combining robust engineering principles with tailored design features, the system addresses the unique challenges of various working scenarios while ensuring reliability, safety, and compliance with industry standards. As a trusted partner in powder processing technology, the company continues to innovate and deliver systems that meet the evolving demands of modern industrial applications, providing customers with a reliable and efficient solution for their material conveying needs.