

[Efficient and Clean Coffee Powder Conveying: An In-Depth Look at Pneumatic Conveying Technology]
Coffee processing facilities worldwide face the critical challenge of efficiently and hygienically transporting coffee powder from production to storage or packaging stages. Traditional methods, such as belt conveyors or manual handling, often introduce contamination risks and inefficiencies that can compromise product quality and operational productivity. Enter pneumatic conveying—a technology that has revolutionized the industry by offering a clean, efficient, and versatile solution for coffee powder transport. This article delves into the principles, benefits, and practical applications of pneumatic conveying, highlighting how it addresses the unique demands of coffee powder handling while maintaining the highest standards of hygiene and performance.
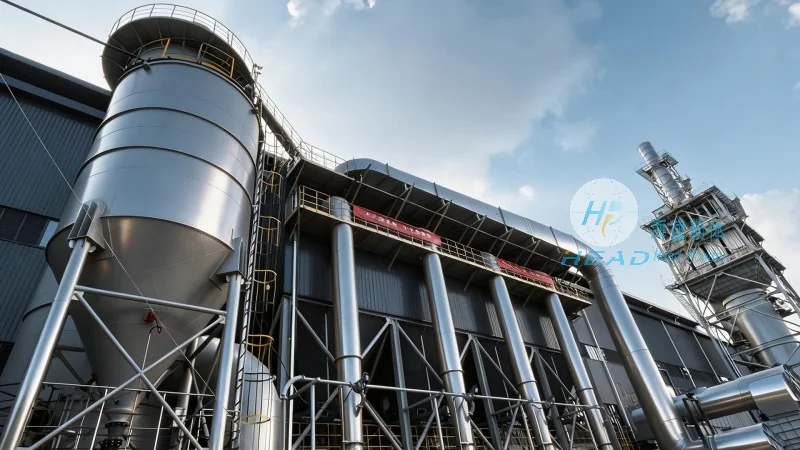
About HeadPowder: Your Trusted Partner in Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of specialized conveying systems tailored for the food and beverage industry. With a focus on innovation and adherence to industry standards, HeadPowder has established itself as a trusted partner for businesses seeking reliable solutions to enhance their coffee powder handling processes. The company’s expertise lies in designing and manufacturing pneumatic conveying systems that meet the stringent requirements of food safety, ensuring that every component is constructed from materials that resist corrosion and contamination, such as stainless steel and food-grade plastics.
Understanding Pneumatic Conveying Technology for Coffee Powder
Pneumatic conveying operates by using air or other gases to transport bulk materials like coffee powder through a network of pipes. There are two primary types: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems create a negative pressure to draw material in. For coffee powder, pressure systems are often preferred due to their ability to handle high volumes and maintain consistent flow rates. The system typically includes a hopper, a rotary valve (for controlling material flow), a conveyor line, and a receiver or silo. The air flow is controlled by a blower or compressor, ensuring that the material is moved smoothly without causing excessive wear or degradation.
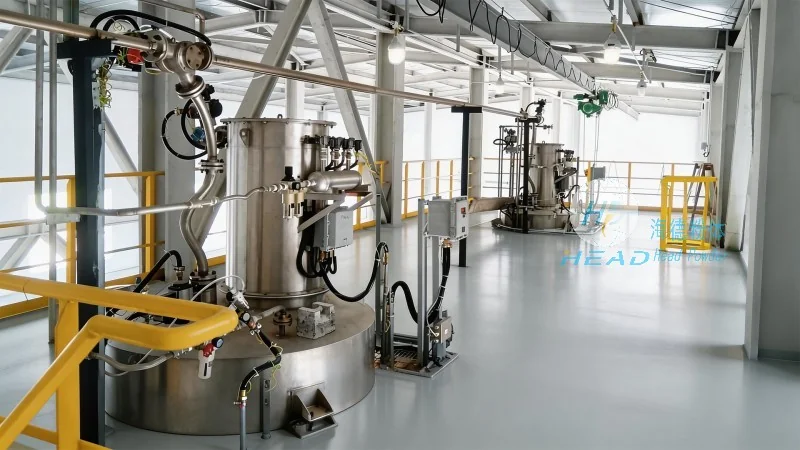
Key Advantages of Pneumatic Conveying for Coffee Powder Handling
One of the most significant advantages of pneumatic conveying for coffee powder is its hygienic design. Unlike mechanical conveyors, which may trap particles and harbor bacteria, pneumatic systems use enclosed pipes that prevent contamination from external sources. This is crucial in coffee processing, where product purity is paramount. Additionally, pneumatic conveying reduces the risk of cross-contamination between different batches of coffee powder, as each system can be isolated and cleaned independently. The technology also minimizes product degradation by avoiding direct contact with metal surfaces and reducing the risk of oxidation or moisture exposure.
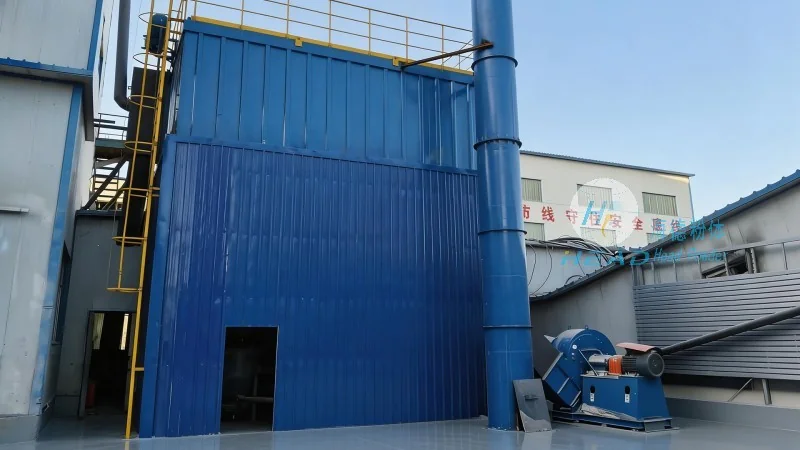
Real-World Applications in Coffee Processing
In coffee processing plants, pneumatic conveying is used in various stages, from raw coffee bean storage to final product packaging. For instance, after roasting, coffee beans are ground into powder, and the pneumatic system can transport this fine powder from the grinding machine to a storage silo without the need for manual handling. This not only improves efficiency but also maintains the freshness and aroma of the coffee by minimizing exposure to air and light. In packaging lines, the system can deliver coffee powder directly to filling machines, ensuring a consistent and controlled flow that reduces waste and improves packaging accuracy.
Conclusion: Enhancing Efficiency and Quality with Pneumatic Conveying
As the coffee industry continues to grow and demand higher standards of quality and hygiene, the importance of efficient and clean conveying systems cannot be overstated. Pneumatic conveying, with its ability to deliver superior performance while maintaining strict food safety protocols, remains a top choice for coffee powder handling. HeadPowder, with its expertise in designing tailored solutions, provides businesses with the tools they need to optimize their operations and meet the evolving needs of the market. By investing in pneumatic conveying technology, coffee producers can enhance productivity, reduce costs, and ensure that their products reach consumers in the best possible condition.