

[Pneumatic Conveying Systems Effectively Solve Cereal Pellet Transportation Challenges]
Efficient and reliable material handling is a critical concern for industries dealing with bulk products, particularly in the food processing sector where maintaining product integrity and operational efficiency is paramount. Among these challenges, the transportation of cereal pellets presents unique difficulties due to their size, shape, and the need for hygienic, dust-free handling. Traditional methods such as belt conveyors or bucket elevators often fall short in meeting these stringent requirements, leading to issues like product degradation, contamination, and increased maintenance costs. This is where pneumatic conveying systems emerge as a superior solution, offering a seamless and effective approach to cereal pellet handling.
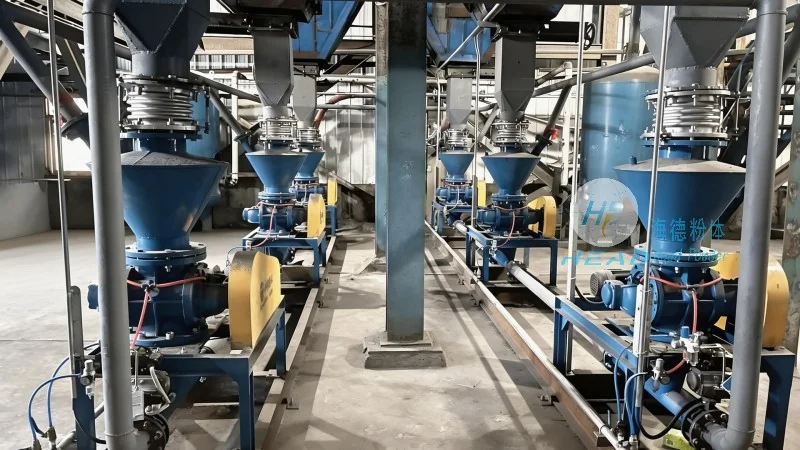
Understanding Pneumatic Conveying Technology
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. Unlike mechanical systems that rely on physical contact and moving parts, pneumatic systems operate by creating a pressure differential that propels the material forward. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems draw material into the system using a vacuum pump. For cereal pellets, pressure systems are often preferred as they provide higher conveying velocities and can handle longer distances without significant pressure loss. The choice of system depends on factors such as the material's properties, the required conveying distance, and the desired level of control over the material flow.
Key Advantages of Pneumatic Conveying for Cereal Pellets
When it comes to cereal pellet transportation, pneumatic conveying systems offer several distinct advantages that make them ideal for this application. First and foremost, they provide a completely enclosed and dust-free environment, which is essential for maintaining the quality and hygiene of food products. Unlike open systems that expose the material to the air and potential contaminants, pneumatic conveyors keep the pellets contained within the pipeline, preventing dust emissions and cross-contamination. This not only ensures compliance with food safety regulations but also enhances the overall product quality by preserving the pellets' texture and nutritional value.
Another significant advantage is the ability to handle varying material characteristics. Cereal pellets can vary in size, density, and moisture content, which can affect the performance of traditional conveyors. Pneumatic systems are designed to accommodate these variations, ensuring consistent and reliable transportation. They can handle both dry and slightly moist pellets without causing blockages or degradation. Additionally, the enclosed nature of the system reduces the risk of material degradation due to exposure to air, light, or moisture, which is crucial for maintaining the product's shelf life and market value.
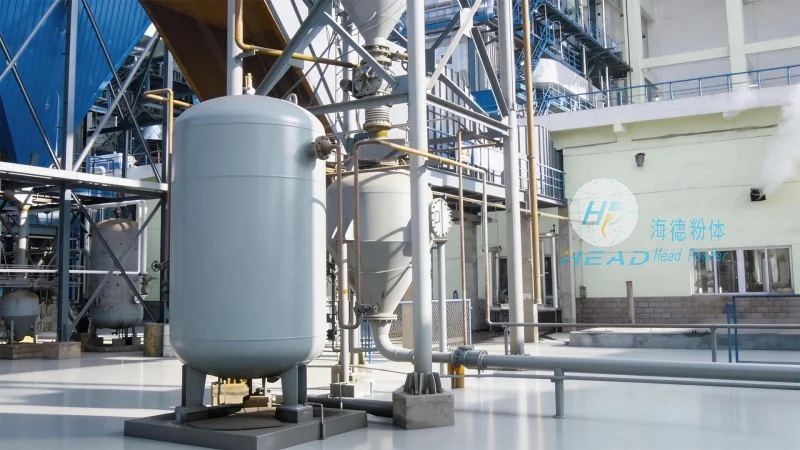
Operational efficiency is another key benefit. Pneumatic conveying systems can transport cereal pellets over long distances with minimal energy consumption compared to mechanical systems. The absence of moving parts like belts or buckets reduces maintenance requirements and downtime, leading to lower operational costs over the system's lifespan. Furthermore, the flexibility of pneumatic systems allows for easy integration with existing production lines, enabling seamless material flow from storage to processing or packaging stages. This adaptability makes them a versatile solution for various production scales and layouts.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of the food processing industry. With years of experience and a deep understanding of material handling challenges, HeadPowder has developed innovative solutions that address the unique requirements of cereal pellet transportation. The company's expertise lies in customizing systems to ensure optimal performance, reliability, and compliance with industry standards.
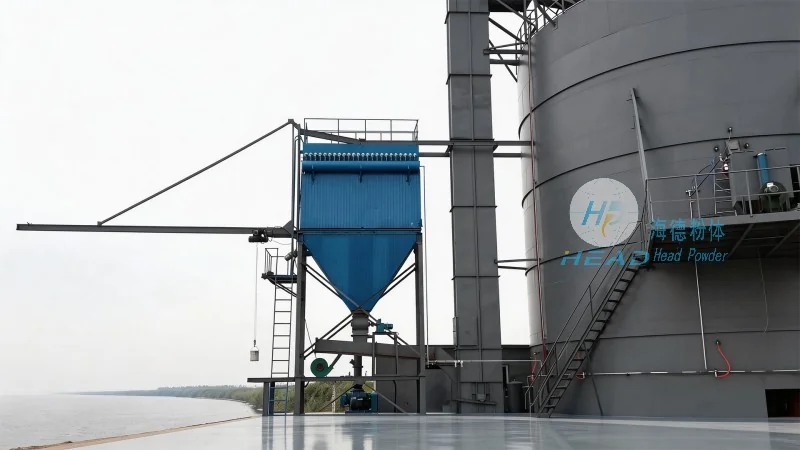
HeadPowder's pneumatic conveying systems are engineered with precision to handle the delicate nature of cereal pellets. The company uses advanced materials and components that are resistant to corrosion, wear, and contamination, ensuring long-term durability and performance. Each system is designed to meet the specific conveying needs of the client, whether it's for short-distance transport within a facility or long-distance transfer between production sites. The company's commitment to quality and customer satisfaction is evident in the robustness and efficiency of their products.
HeadPowder's team of engineers and technicians works closely with clients to understand their operational requirements and provide tailored solutions. From initial consultation and system design to installation and maintenance, HeadPowder offers comprehensive support to ensure the successful implementation and long-term operation of the conveying system. The company's focus on customer needs and technical excellence has made it a trusted partner for businesses seeking reliable and efficient material handling solutions.
Conclusion: The Future of Cereal Pellet Transportation
In conclusion, pneumatic conveying systems represent a highly effective and efficient solution for the transportation of cereal pellets. By leveraging the power of air to move materials through enclosed pipelines, these systems offer superior control, hygiene, and flexibility compared to traditional methods. For industries dealing with bulk food products, the adoption of pneumatic conveying technology is not just an option but a necessity to maintain product quality, operational efficiency, and regulatory compliance. With the expertise and innovation of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can now access advanced solutions that address their specific challenges and drive operational success.