

Principle and Working Scene Characteristics of White and Gray Material Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced material handling solutions tailored for the transportation of white and gray powders. This article explores the fundamental principles underlying such systems and highlights key working scene characteristics that define their effectiveness in industrial applications.
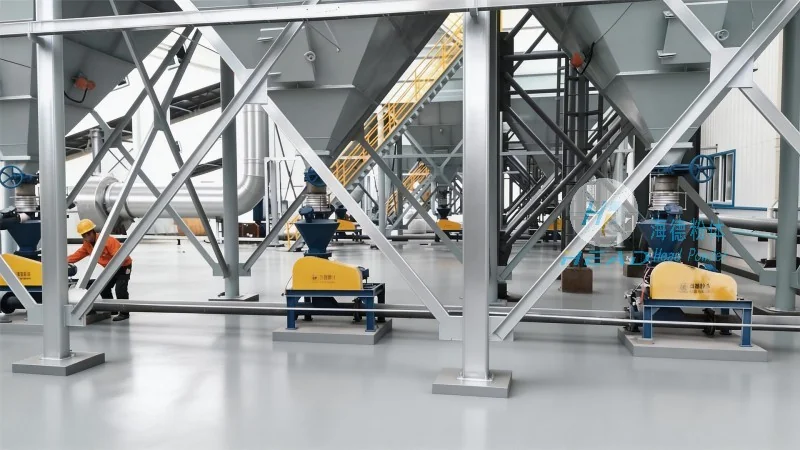
Core Principles of Material Conveying Systems
The operation of white and gray material conveying systems is built upon several core principles that ensure efficient, reliable, and safe material transport. These systems typically utilize a combination of mechanical components, such as conveyor belts, screw conveyors, or pneumatic pipelines, to move bulk materials from one location to another. The choice of equipment depends on factors like material properties, required throughput, and environmental conditions. For instance, pneumatic conveying systems are ideal for handling fine powders due to their ability to transport materials through air, minimizing dust and contamination risks. In contrast, screw conveyors offer a cost-effective solution for bulkier, less abrasive materials, providing consistent flow and minimal maintenance.
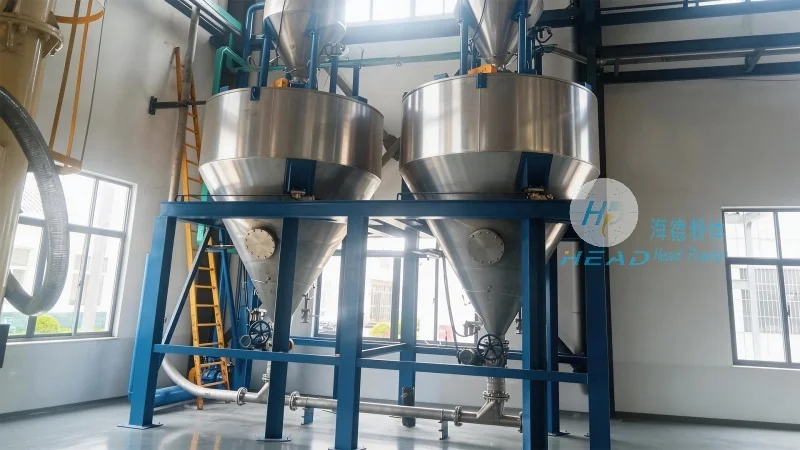
Working Scene Characteristics and Application Scenarios
The working scene characteristics of white and gray material conveying systems are closely tied to the specific industrial environments where they are deployed. These systems are commonly found in sectors like cement production, chemical processing, food processing, and pharmaceutical manufacturing, where the handling of fine powders is critical. In cement plants, for example, conveying systems transport raw materials like limestone and clay to grinding mills, ensuring a steady supply for cement production. The working scene often involves high-volume material handling, requiring robust equipment capable of withstanding heavy loads and abrasive materials. Similarly, in chemical plants, conveying systems move white powders like calcium carbonate or gray powders like silica, maintaining process efficiency and product quality. The working environment may include strict safety protocols, as many powders are combustible or toxic, necessitating explosion-proof designs and proper ventilation systems.
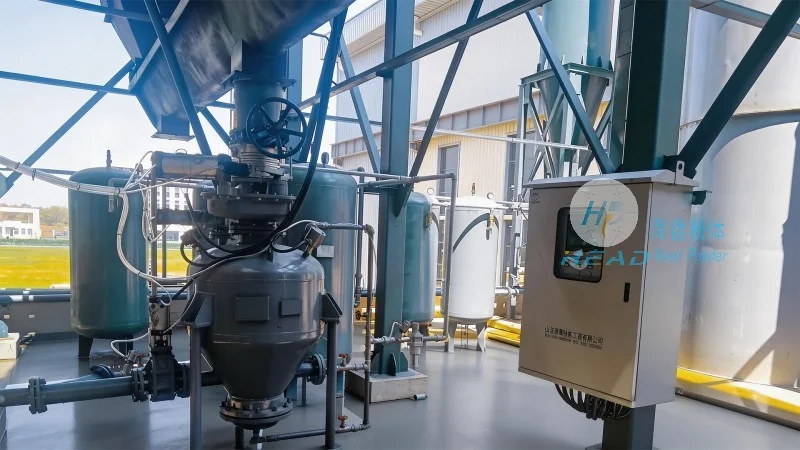
Key Features and Advantages in Real-World Applications
Real-world applications of white and gray material conveying systems showcase several key features that enhance operational performance. One notable advantage is the ability to handle diverse material types, from fine powders to bulk granules, without compromising system efficiency. This versatility is achieved through adjustable conveyor speeds, variable pressure in pneumatic systems, and modular components that can be customized to meet specific process requirements. Another critical feature is the integration of monitoring and control systems, which allow operators to track material flow, detect blockages, and adjust parameters in real time. This not only improves productivity but also reduces downtime and maintenance costs. Additionally, modern conveying systems incorporate energy-efficient designs, such as variable frequency drives (VFDs), which optimize power consumption based on the load, contributing to lower operational costs and reduced environmental impact.
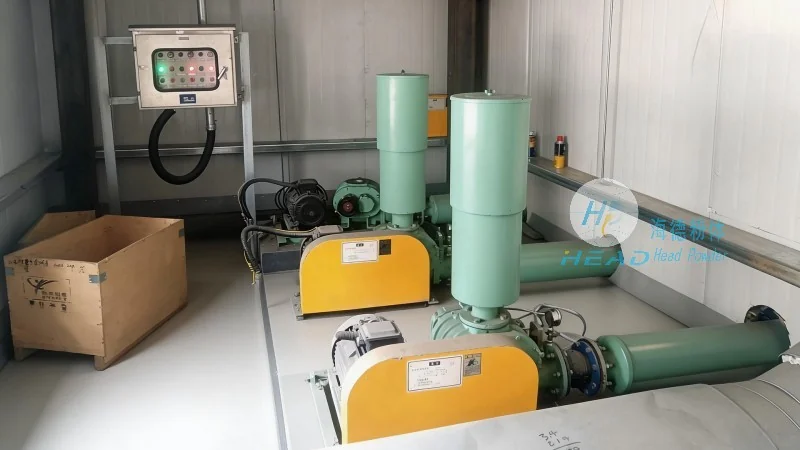
Conclusion and Company Expertise
White and gray material conveying systems represent a vital component of modern industrial operations, enabling efficient and safe material handling across various sectors. Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in engineering and manufacturing to deliver tailored solutions that meet the unique demands of each application. By adhering to rigorous quality standards and incorporating advanced technologies, the company ensures that its conveying systems provide reliable performance, enhance productivity, and contribute to sustainable industrial practices. Whether for cement production, chemical processing, or other industries, the principles and working scene characteristics of these systems remain central to optimizing material transport and supporting overall operational success.