

Principle and Operational Characteristics of Nitrile Rubber Powder Pneumatic Conveying Systems
HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying systems designed for the efficient transport of nitrile rubber powders. This article delves into the fundamental principles and operational characteristics of such systems, highlighting their applications and benefits in industrial settings.
Understanding the Core Principle of Nitrile Rubber Powder Pneumatic Conveying
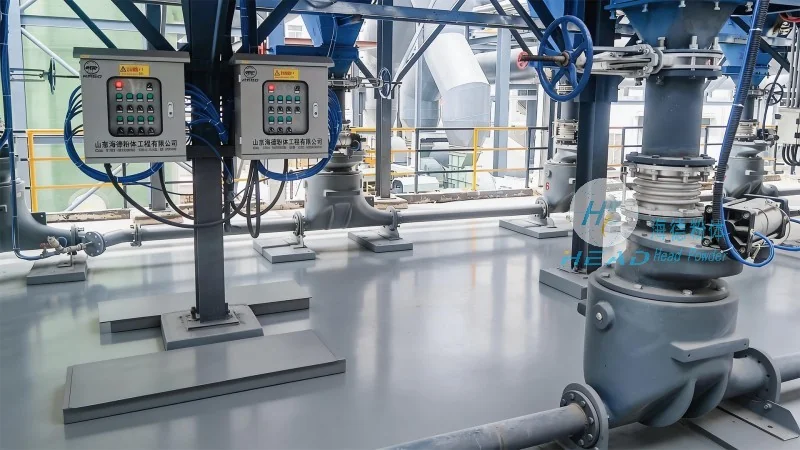
The pneumatic conveying system for nitrile rubber powders operates on the principle of using air or gas as the medium to transport solid particles. This method, also known as pneumatic transport, involves the creation of a flow of air through a pipeline, which then carries the rubber powder particles along with it. The system typically consists of several key components, including a feeding device, a conveying line, a separation unit, and a discharge outlet. The feeding device ensures a consistent and controlled introduction of the nitrile rubber powder into the system, while the conveying line facilitates the movement of the material through the pipeline. The separation unit, often a cyclone or a filter, separates the powder from the air stream, allowing for the recovery of the material and the release of clean air. The discharge outlet then delivers the nitrile rubber powder to its final destination, such as a storage silo or a processing unit.
Key Operational Characteristics and Advantages
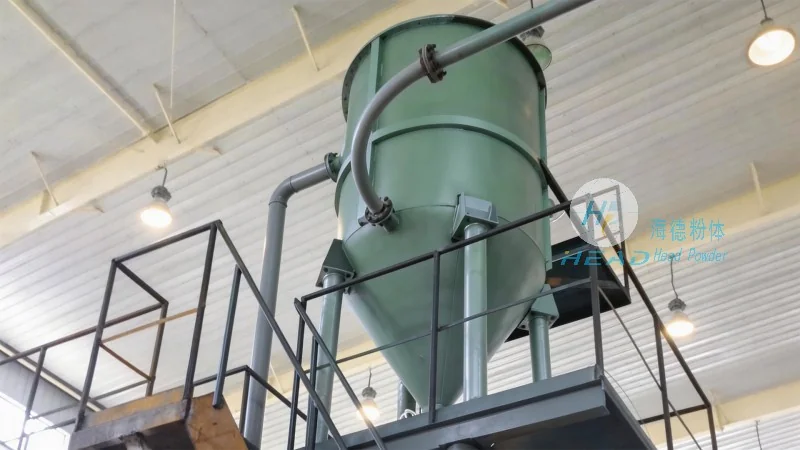
One of the primary advantages of nitrile rubber powder pneumatic conveying systems is their ability to handle fine powders with high efficiency and minimal product degradation. The system's design minimizes the risk of material caking or agglomeration, which can occur in traditional bulk handling methods. Additionally, pneumatic conveying offers a hygienic and dust-free operation, making it suitable for applications where product purity is critical, such as in the manufacturing of automotive parts or medical devices. The system also provides flexibility in terms of layout, as the conveying lines can be configured to follow the existing plant layout, optimizing space utilization. Furthermore, the use of air as the conveying medium allows for the integration of multiple feeding and discharge points, enabling the simultaneous transport of different materials or the transfer of materials between different processing stages.
Typical Work Scenarios and Applications
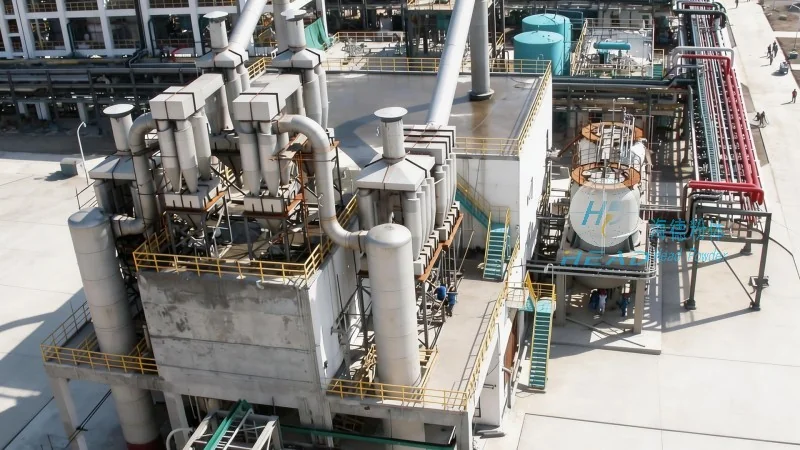
Nitrile rubber powder pneumatic conveying systems are widely used in various industrial applications, particularly in the rubber and tire manufacturing industries. In these settings, the system is employed to transport nitrile rubber powders from storage silos to mixing units, or from processing lines to packaging facilities. The systems are also utilized in the production of adhesives, sealants, and other rubber-based products, where the consistent and reliable transport of raw materials is essential for maintaining product quality and production efficiency. Another common application is in the recycling industry, where the system helps in the transport of recycled nitrile rubber particles from sorting and grinding processes to reprocessing units. The versatility of the system makes it suitable for both new plant installations and the retrofitting of existing facilities, providing a cost-effective solution for material handling needs.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
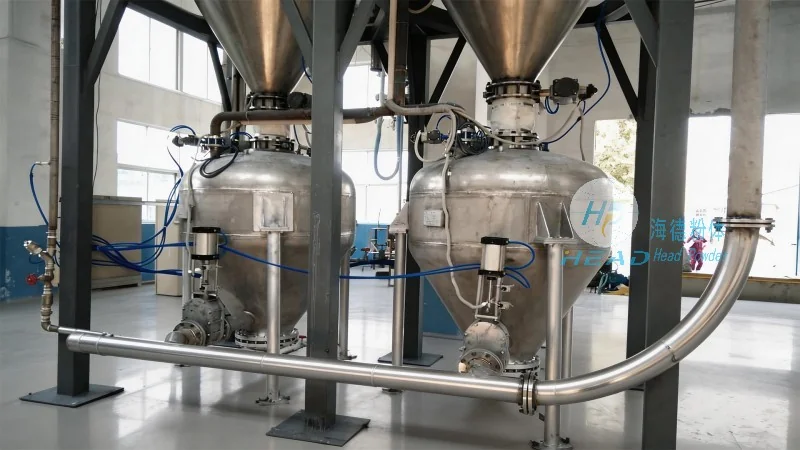
HeadPowder, as a professional engineering company based in Shandong, China, has established itself as a trusted partner in the design, manufacturing, and installation of pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has developed a range of customized solutions tailored to the specific requirements of its clients. The company's team of experienced engineers and technicians ensures that each system is designed to meet the highest standards of performance, reliability, and safety. HeadPowder's commitment to quality is reflected in its adherence to international standards and its use of advanced materials and technologies in the construction of its systems. The company's facilities in Shandong are equipped with state-of-the-art equipment and testing capabilities, enabling it to deliver systems that are efficient, durable, and cost-effective. By leveraging its expertise and local presence, HeadPowder provides comprehensive support to its clients, from initial consultation and system design to installation, commissioning, and after-sales service.