

Principle and Working Scene Characteristics of Chocolate Powder Pneumatic Conveying Lines
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the chocolate industry. This article delves into the fundamental principles behind these systems and highlights key operational characteristics that define their effectiveness in real-world applications.
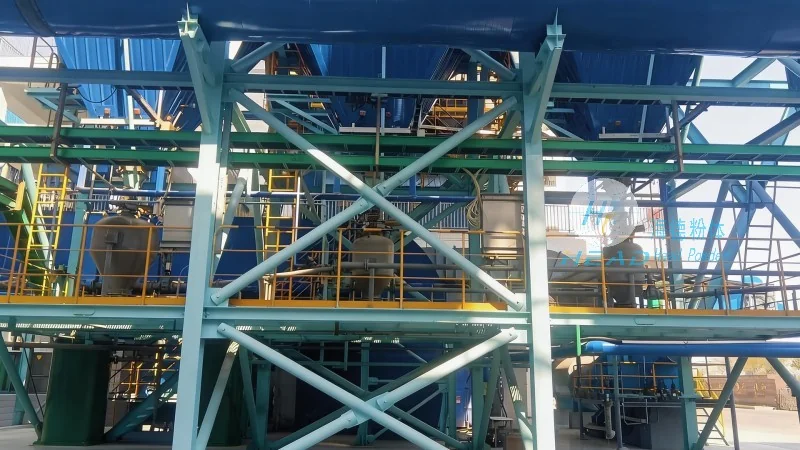
Company Overview: HeadPowder Engineering
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to providing innovative solutions for material handling challenges, particularly in the food processing sector. With a strong presence in Shandong, China, the company leverages decades of expertise to develop customized pneumatic conveying lines that meet stringent industry standards for hygiene, efficiency, and reliability. The company’s commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking to optimize their chocolate powder handling processes.
The Principle of Pneumatic Conveying for Chocolate Powder
Pneumatic conveying systems operate by transporting bulk materials, such as chocolate powder, through a pipeline using compressed air. In the case of chocolate powder, these systems typically employ a positive pressure or negative pressure (vacuum) method to move the material from the source to the destination. The positive pressure system involves blowing air into the pipeline, creating a flow that carries the powder particles. This method is particularly effective for short to medium-distance transfers and is commonly used in chocolate production facilities where space is limited. The negative pressure system, on the other hand, draws the powder into the pipeline using a vacuum, which is ideal for longer distances or when the material needs to be collected from multiple points. Both methods ensure that the chocolate powder remains in a dry, free-flowing state, minimizing the risk of caking or degradation during transport.
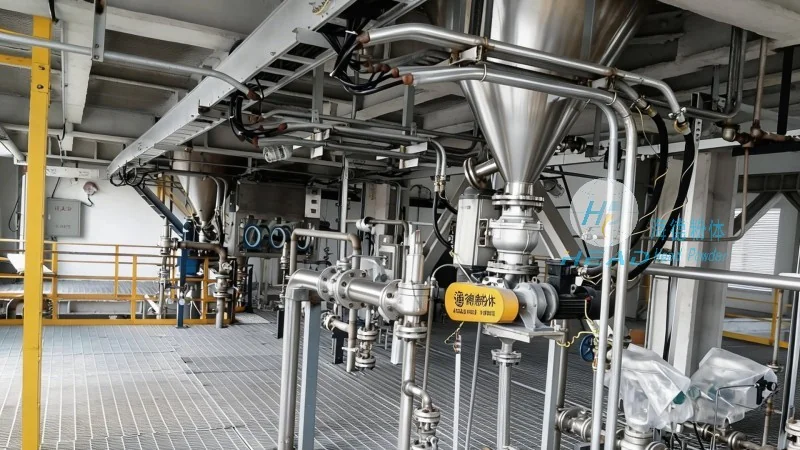
Key Working Scene Characteristics
The effectiveness of chocolate powder pneumatic conveying lines is defined by several critical characteristics that adapt to diverse operational needs. Firstly, the system’s ability to maintain a consistent flow rate is paramount, as fluctuations can lead to product loss or equipment damage. Advanced control systems, often integrated with the conveying line, allow for real-time monitoring and adjustment of air pressure and flow, ensuring optimal performance. Secondly, the design of the system must consider the hygienic requirements of the chocolate industry. Materials used in the construction of the pipeline, such as stainless steel, are non-corrosive and easy to clean, complying with food safety regulations. Additionally, the system’s flexibility in handling varying particle sizes and moisture content is essential, as chocolate powders can have different properties depending on the production stage. For instance, pre-conveyed powders may require different air-to-material ratios compared to freshly produced powders, and the system must be capable of adapting to these variations without compromising efficiency.
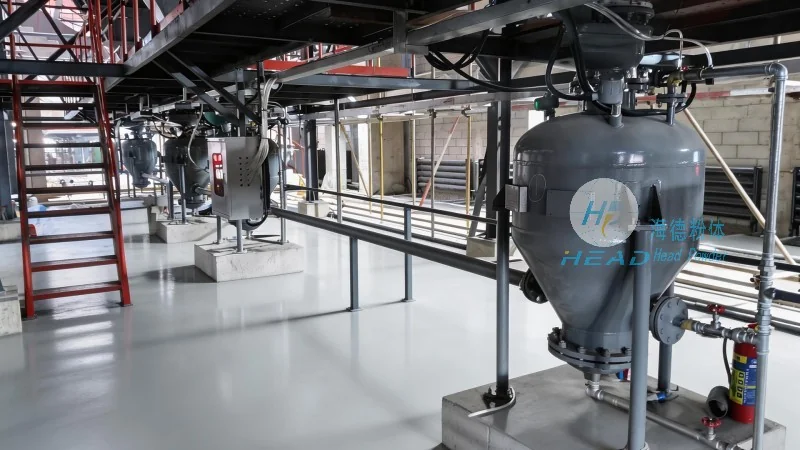
Applications and Operational Efficiency
Chocolate powder pneumatic conveying lines are widely used in various stages of chocolate production, from raw material handling to final product packaging. In the raw material stage, these systems efficiently transport cocoa powder and other ingredients from storage silos to mixing tanks, reducing manual labor and improving process consistency. During the production phase, the system can convey the mixed chocolate paste to the molding or enrobing machines, ensuring a smooth and continuous flow. In the packaging stage, the system transfers finished chocolate powders into packaging machines, minimizing product exposure to contaminants and maintaining product integrity. The operational efficiency of these systems is further enhanced by their ability to handle large volumes of material with minimal downtime. By integrating automated controls and sensors, the systems can detect blockages or leaks in real time, allowing for immediate troubleshooting and preventing costly production interruptions.
Conclusion and Company Commitment
Chocolate powder pneumatic conveying lines, as exemplified by the solutions offered by HeadPowder Engineering, represent a sophisticated approach to material handling in the chocolate industry. By combining fundamental pneumatic principles with advanced engineering, these systems provide reliable, hygienic, and efficient transport solutions that meet the demanding requirements of modern chocolate production. HeadPowder Engineering remains committed to innovation, continuously developing and refining its systems to deliver optimal performance for its clients. With a strong foundation in Shandong, China, the company continues to serve the global market with tailored solutions that enhance productivity and ensure product quality.