

[Efficient Pneumatic Conveying Systems for Organic Fertilizer Granule Transport Solutions]
Organic fertilizer granules present unique challenges in material handling due to their size, shape, and tendency to clump or agglomerate. Traditional methods like belt conveyors or bucket elevators often struggle with maintaining consistent flow rates and can cause material degradation or equipment wear. Pneumatic conveying systems, however, offer a robust and flexible solution tailored to these specific demands.
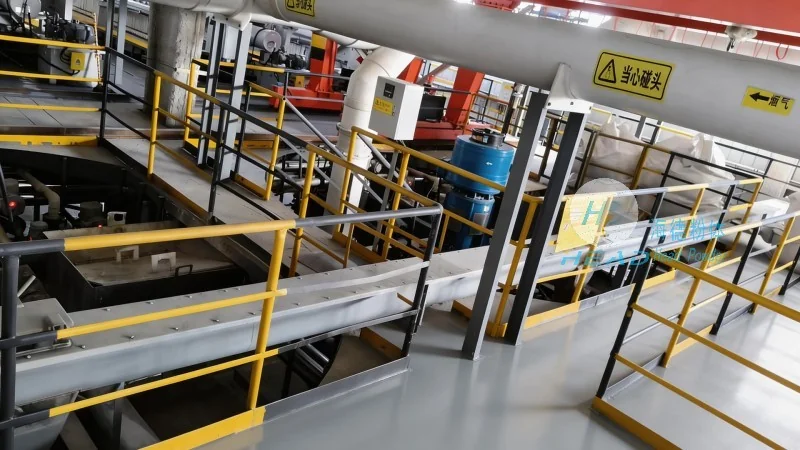
Advanced Pneumatic Conveying Technology for Organic Fertilizer Handling
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems that address the complexities of organic fertilizer granule transport. Our systems leverage compressed air to move materials through pipelines, eliminating the need for mechanical components that may interfere with delicate or sticky granules. This approach not only ensures minimal product degradation but also reduces maintenance costs and operational downtime.
Key Advantages of Pneumatic Conveying for Organic Fertilizers
Compared to traditional bulk handling equipment, pneumatic conveying systems provide several advantages for organic fertilizer granules. First, they offer high flexibility in system layout, allowing for complex routing around existing structures or equipment. Second, the air-based transport minimizes friction and abrasion, preserving the granule's integrity and preventing caking or degradation. Third, these systems can handle a wide range of particle sizes and moisture contents, making them suitable for various organic fertilizer formulations. Additionally, the enclosed pipeline design enhances safety by containing dust and odors, which is crucial in agricultural and environmental applications.
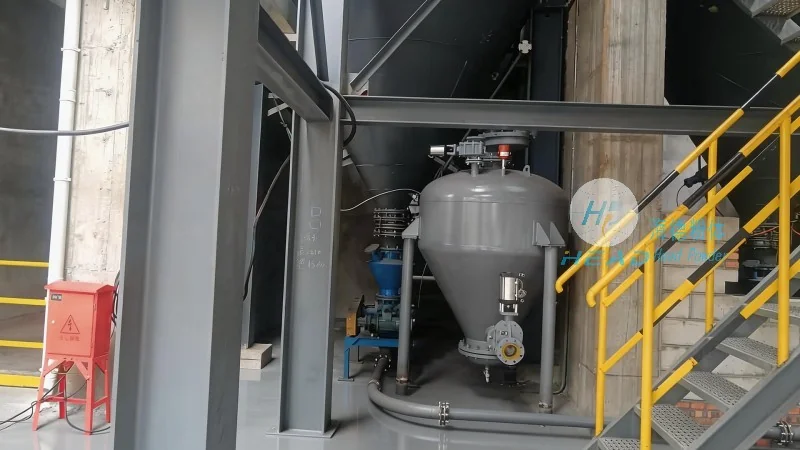
Customized Solutions from HeadPowder
At Shandong HeadPowder Engineering Co., Ltd., we understand that each organic fertilizer operation has unique requirements. Our engineering team works closely with clients to develop tailored pneumatic conveying solutions that meet specific production capacities, space constraints, and material characteristics. Whether for short-distance transport within a facility or long-distance transfer between sites, our systems are designed for reliability and efficiency. We utilize advanced control systems to optimize air pressure, flow rates, and material velocity, ensuring consistent performance and minimal energy consumption.
Reliability and Durability in Organic Fertilizer Handling
Organic fertilizers often contain abrasive or corrosive components that can impact equipment longevity. HeadPowder's pneumatic conveying systems are constructed with high-quality materials, including stainless steel and corrosion-resistant alloys, to withstand the harsh conditions of organic fertilizer processing. The use of flexible hoses and wear-resistant liners in critical areas further extends the system's lifespan. Regular maintenance and service programs are also available to ensure continuous operation and reduce unexpected failures. Our commitment to durability ensures that clients can rely on our systems for long-term, trouble-free operation in demanding agricultural environments.
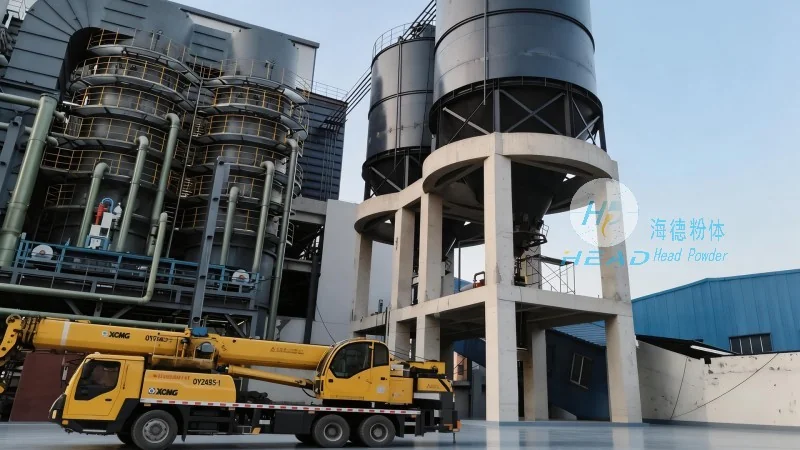
Environmental and Operational Benefits
Pneumatic conveying systems offer significant environmental advantages for organic fertilizer handling. By containing dust and odors within the pipeline, they reduce emissions and improve workplace air quality. This is particularly important in facilities where organic fertilizers are processed or stored, as it helps comply with environmental regulations and enhances worker safety. Additionally, the enclosed system minimizes material loss during transport, improving overall efficiency and reducing waste. From a operational standpoint, pneumatic conveying systems can be integrated with existing production lines, allowing for seamless material transfer without disrupting workflow. The energy efficiency of these systems, achieved through optimized air usage and minimal mechanical parts, also contributes to lower operational costs over time.
Conclusion: The Role of Pneumatic Conveying in Modern Organic Fertilizer Processing
For industries dealing with organic fertilizer granules, pneumatic conveying systems represent a superior solution to traditional bulk handling methods. The flexibility, efficiency, and reliability of these systems make them indispensable in modern agricultural and environmental applications. Shandong HeadPowder Engineering Co., Ltd. stands as a leader in providing advanced pneumatic conveying solutions tailored to the unique needs of organic fertilizer producers. By investing in such technology, companies can enhance their operational performance, reduce costs, and ensure compliance with environmental standards. The future of organic fertilizer transport lies in innovative, reliable systems like those offered by HeadPowder, supporting sustainable agricultural practices and environmental stewardship.