

What is a Powdered Mineral Pneumatic Conveying Machine? And What Are Its Design Principles?
Understanding the powdered mineral pneumatic conveying machine and its design principles is crucial for industries dealing with bulk material handling. This equipment is specifically engineered to transport dry, fine powders through a pipeline using air or gas as the conveying medium. The technology offers a flexible and efficient solution for moving materials like minerals, chemicals, and other granular substances over short to medium distances.
Introduction to Powdered Mineral Pneumatic Conveying Machines
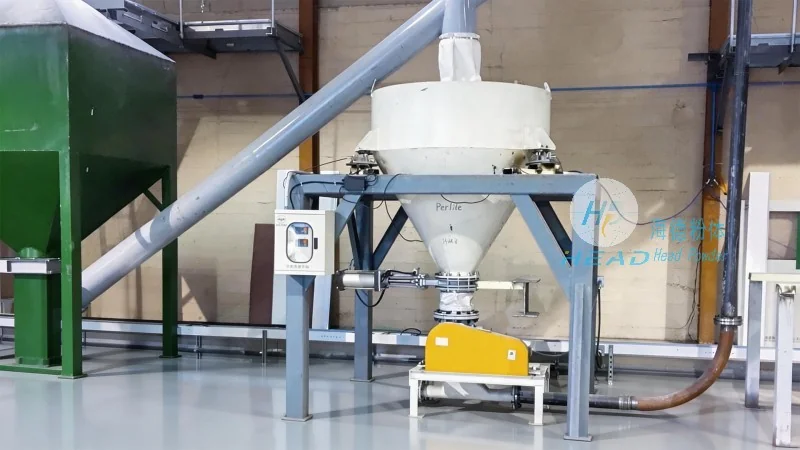
Powdered mineral pneumatic conveying machines, often referred to as pneumatic conveyors, are industrial systems designed to transport dry, fine powders from one location to another. Unlike traditional mechanical conveyors, which rely on belts or buckets, pneumatic systems use compressed air or other gases to create a flow of material through a pipeline. This method is particularly advantageous for handling materials that are prone to dust, require minimal contact with equipment, or need to be transported in a closed system to prevent contamination or environmental issues.
Core Components and Working Principle
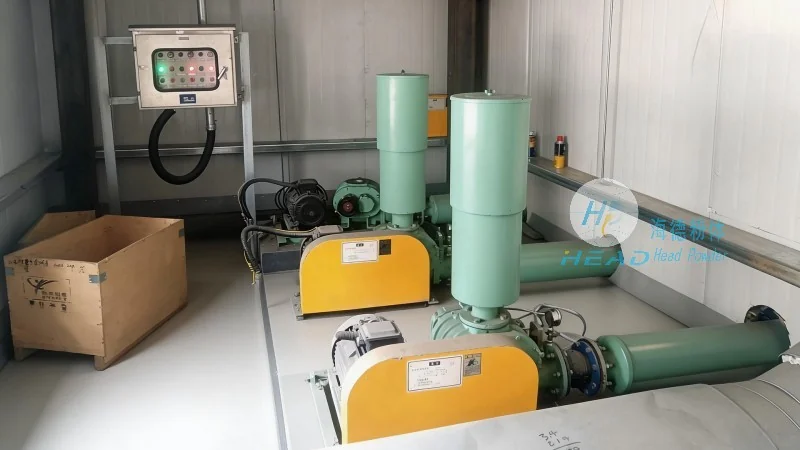
The design of a powdered mineral pneumatic conveying machine typically involves several key components that work in concert to achieve efficient material transport. The primary components include a hopper for material storage, a blower or compressor to generate the conveying air, a pipeline system to direct the material flow, and a receiver or discharge unit to collect the transported material. The working principle revolves around creating a pressure differential within the pipeline. The blower generates high-pressure air, which is introduced into the hopper, causing the powder to be entrained and carried along the pipeline. As the material travels through the system, it is suspended in the air stream and directed to the discharge point. The receiver then collects the material, and the air is typically filtered and recycled back to the system to maintain efficiency and reduce waste.
Design Principles for Efficient Material Handling
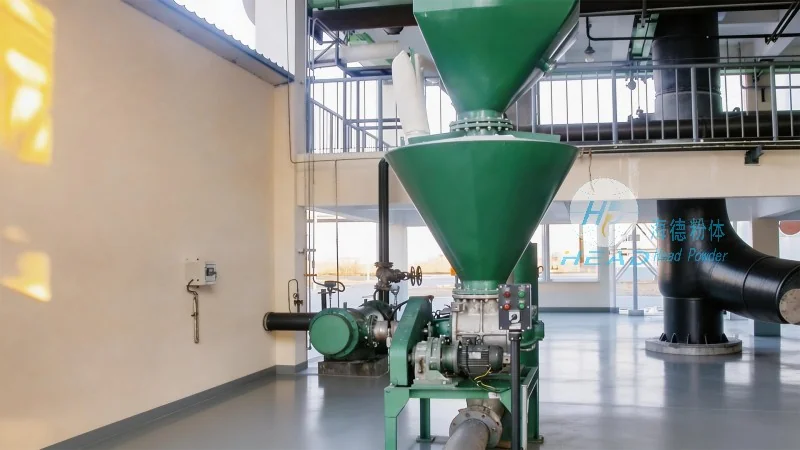
The design principles of a powdered mineral pneumatic conveying machine are centered on optimizing the flow of material and air to ensure maximum efficiency and minimal energy consumption. Key design considerations include the selection of appropriate air velocity, which must be sufficient to keep the powder suspended but not so high as to cause excessive pressure drops or energy waste. The pipeline diameter and length are also critical factors, as they directly impact the pressure requirements and overall system performance. Engineers must carefully calculate the air volume and pressure needed to overcome friction losses in the pipeline and lift the material to the desired height. Additionally, the system's layout, including the number and placement of bends, expansions, and contractions, must be optimized to minimize pressure losses and maintain a consistent flow rate. The choice of materials for the pipeline and components is another important design aspect, as they must be resistant to corrosion, abrasion, and the specific properties of the mineral being conveyed.
Applications and Benefits in Industrial Settings
Powdered mineral pneumatic conveying machines are widely used in various industrial applications, including mining, chemical processing, food processing, and pharmaceutical manufacturing. In the mining industry, they are used to transport ore and mineral powders from processing plants to storage facilities or for further processing. In chemical plants, they handle powders such as cement, limestone, and various chemicals, ensuring a clean and efficient transfer process. The benefits of using pneumatic conveying systems include improved safety by containing dust and preventing exposure to hazardous materials, reduced maintenance compared to mechanical systems, and the ability to transport materials in a closed system, which helps maintain product quality and prevents contamination. Additionally, these systems offer flexibility in terms of layout and can be easily integrated into existing production lines, making them a versatile solution for bulk material handling needs.
About Shandong HeadPowder Engineering Co., Ltd.
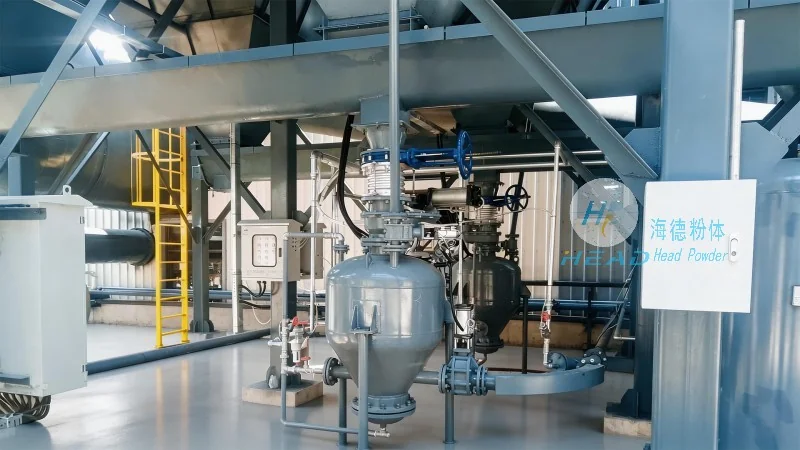
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying equipment and related solutions. With a strong focus on innovation and quality, the company specializes in designing and manufacturing customized powdered mineral pneumatic conveying machines tailored to the specific needs of its clients. HeadPowder's headquarters is located in Shandong, China, where the company leverages advanced technology and experienced engineering teams to develop cutting-edge solutions for the bulk material handling industry. The company's commitment to customer satisfaction and product excellence has established it as a trusted partner for businesses seeking reliable and efficient pneumatic conveying systems.