

What is a Multi-functional Powder Handling Equipment? What are its Design Principles?
For industries dealing with bulk powders, the selection of an appropriate powder handling system is crucial for operational efficiency and product quality. A multi-functional powder handling equipment, as offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to meet diverse material handling needs. This article explores the concept of such equipment and delves into its underlying design principles, highlighting how these systems enhance process reliability and operational flexibility.
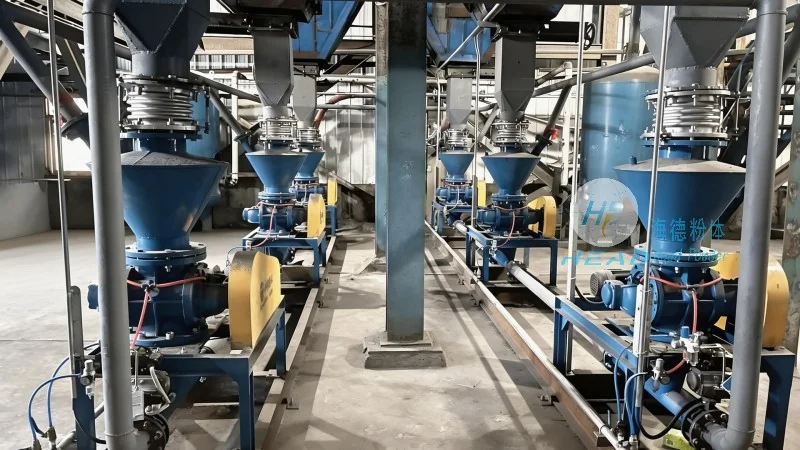
Introduction to Multi-functional Powder Handling Equipment
Multi-functional powder handling equipment is a versatile system engineered to transport, store, and manage various types of powders in industrial settings. Unlike traditional, single-purpose conveyors, these systems integrate multiple functions such as bulk material feeding, conveying, dosing, and storage, making them indispensable in sectors like pharmaceuticals, food processing, chemical manufacturing, and mining. The design of these equipment is tailored to accommodate a wide range of powder characteristics, including different particle sizes, densities, and flow properties, ensuring optimal performance under varying operational conditions.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the research, development, and manufacturing of advanced powder handling solutions. With a strong commitment to innovation and quality, the company has established itself as a leading provider in the industry. HeadPowder's products are designed to address the unique challenges faced by modern industrial processes, offering reliable and efficient solutions that enhance productivity and reduce downtime. The company's headquarters is located in Shandong, China, where state-of-the-art facilities and a skilled workforce ensure the production of high-performance equipment that meets international standards.
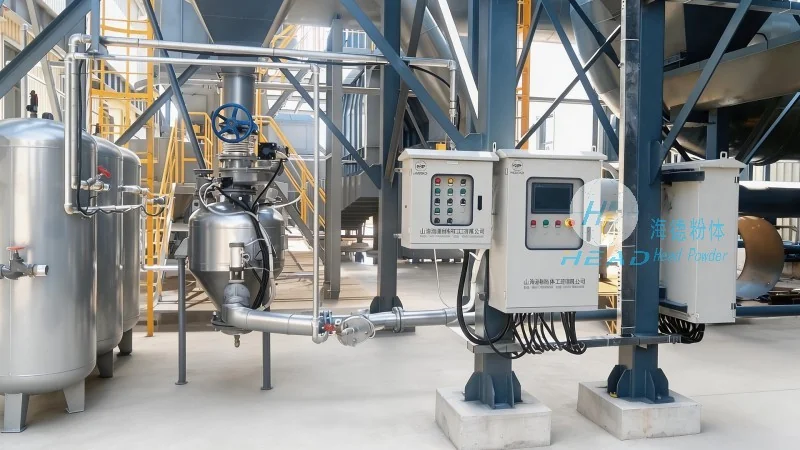
Design Principles of Multi-functional Powder Handling Equipment
The design of a multi-functional powder handling equipment is guided by several key principles aimed at maximizing efficiency, safety, and adaptability. First, the system must ensure reliable material flow, which is achieved through the integration of appropriate conveying technologies such as pneumatic conveying, screw conveyors, or belt conveyors. The choice of conveying method depends on the specific properties of the powder, such as its flowability and dustiness. For example, pneumatic conveying systems are ideal for handling fine powders that are prone to dust generation, while screw conveyors are suitable for bulkier materials that require consistent feeding.
Second, the equipment must incorporate robust control mechanisms to regulate the flow rate and dosing accuracy. Advanced sensors and control systems are employed to monitor parameters like pressure, flow rate, and temperature, ensuring that the material is handled within safe and optimal conditions. This not only improves the precision of the process but also enhances safety by preventing overloading or underflow situations. The control systems are typically integrated with user-friendly interfaces, allowing operators to adjust settings easily and monitor the system's performance in real-time.
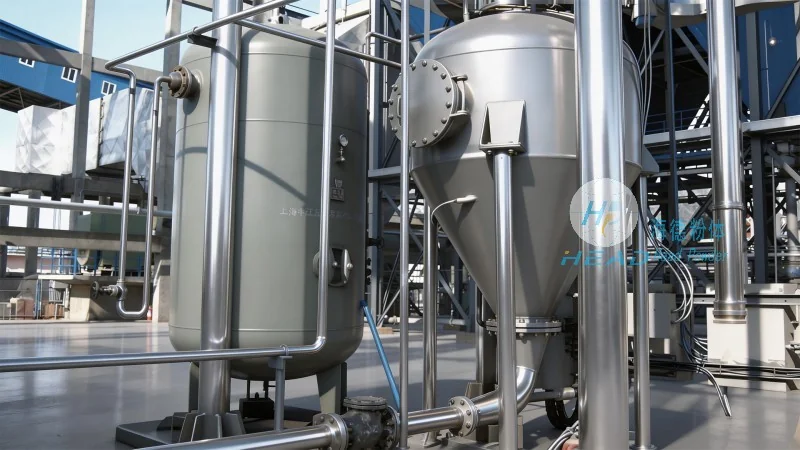
Third, the design emphasizes modular construction, enabling flexibility and scalability. Modular components allow for easy customization and expansion as the production needs evolve. This modularity also facilitates maintenance and repair, as individual parts can be replaced without disrupting the entire system. Additionally, the equipment is designed with materials that are resistant to corrosion and wear, ensuring long-term durability and minimal maintenance costs.
Key Features and Benefits
Multi-functional powder handling equipment from HeadPowder offers several key features that contribute to its effectiveness. One of the primary advantages is the ability to handle a wide variety of powders, from fine pharmaceutical powders to coarse industrial materials, without the need for multiple systems. This versatility reduces capital expenditure and operational complexity, as a single unit can serve multiple applications. The equipment also features high efficiency in material transport, minimizing energy consumption and operational costs. Furthermore, the design prioritizes safety, incorporating features such as dust collection systems and explosion-proof components to protect both personnel and equipment from potential hazards.
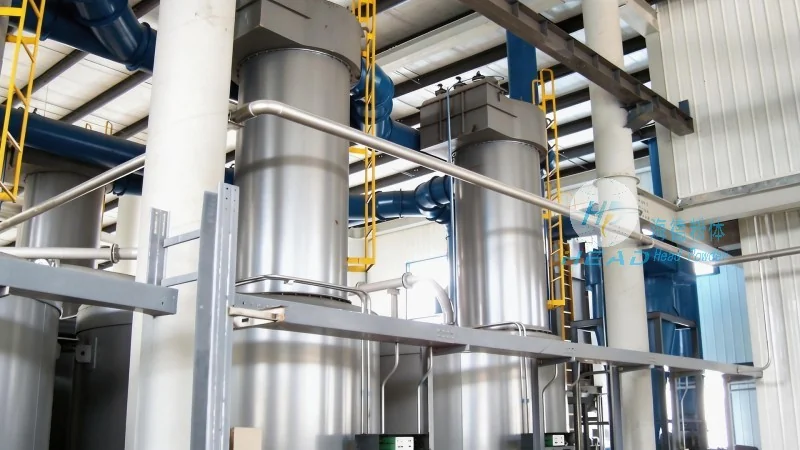
Another significant benefit is the enhanced process control and consistency. By integrating precise dosing and conveying mechanisms, the equipment ensures that the material is delivered in the exact quantities required, reducing waste and improving product quality. This level of control is particularly critical in industries where product uniformity is paramount, such as in food and pharmaceutical manufacturing. The equipment also supports automated operation, allowing for seamless integration into existing production lines and reducing the need for manual intervention.
Conclusion
In conclusion, multi-functional powder handling equipment, as designed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution for modern industrial material handling challenges. By combining advanced design principles with robust construction and versatile functionality, these systems enhance operational efficiency, improve product quality, and ensure safety in various industrial applications. For businesses seeking reliable and efficient powder handling solutions, HeadPowder's equipment offers a comprehensive and adaptable approach to meet their needs, supporting long-term operational success and growth.